

Principle and Working Scene Characteristics of Mobile Powder Pneumatic Conveying Equipment
Mobile powder pneumatic conveying equipment represents a sophisticated solution for transporting bulk powder materials efficiently and reliably. This technology leverages compressed air or other gases to move powders through a network of pipes, offering a flexible and portable alternative to traditional bulk material handling methods. The equipment is designed with a mobile chassis, allowing it to be deployed quickly to various work sites, making it ideal for applications where fixed infrastructure is not feasible or where material handling needs to be adapted to changing project requirements.
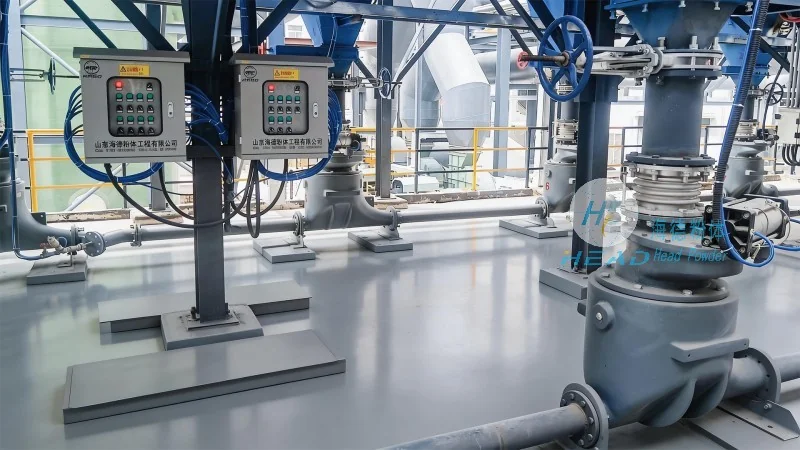
Working Scene Characteristics
The working scene characteristics of mobile powder pneumatic conveying equipment are defined by its adaptability and operational flexibility. These systems are commonly employed in industrial settings such as construction sites, chemical plants, and food processing facilities. The equipment excels in scenarios requiring the transport of large volumes of powders over moderate distances, often in environments where traditional conveyor systems may be impractical due to space constraints or site accessibility issues. For instance, on a construction project, a mobile unit can be used to convey cement, fly ash, or other bulk building materials from storage to mixing areas, reducing the need for manual labor and minimizing material spillage.
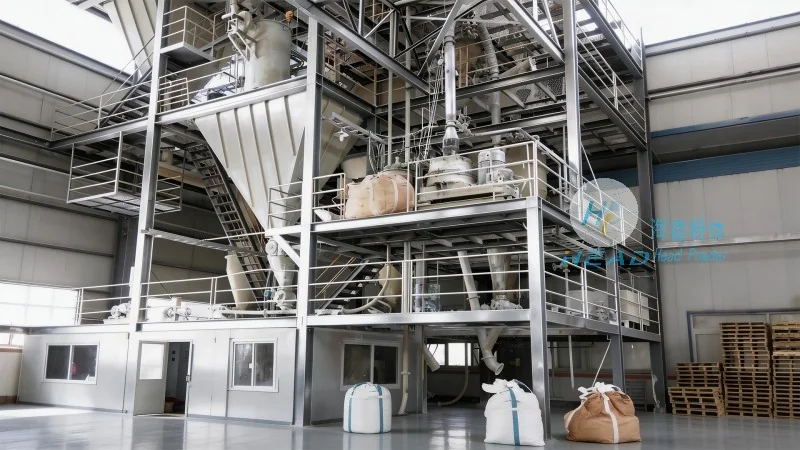
Technical Principles
The technical foundation of mobile powder pneumatic conveying equipment is rooted in fluid dynamics and air pressure principles. The system operates by generating a high-pressure airflow using a powerful blower or fan. This airflow creates a negative pressure (in the case of suction systems) or positive pressure (in the case of pressure systems) that draws or pushes the powder particles into the conveying line. The equipment typically includes key components such as a hopper for material loading, a filter system to capture fine particles and prevent air pollution, and a separation unit to return the conveyed material to the discharge point. The mobile design integrates these components onto a wheeled or tracked chassis, enabling easy movement and setup at different locations.
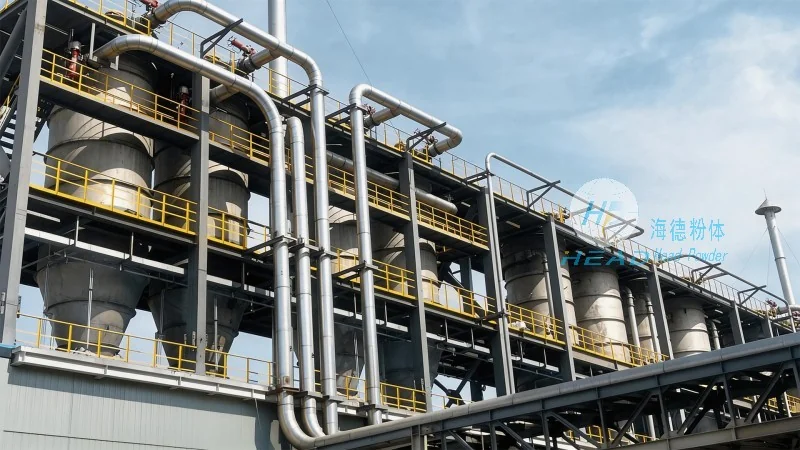
Application Scenarios
Application scenarios for mobile powder pneumatic conveying equipment span a wide range of industries and tasks. In the construction industry, they are widely used for transporting cement, sand, and other construction powders, especially in large-scale projects where material supply needs to be managed efficiently. In the chemical industry, these systems handle various raw materials like polymers, pigments, and additives, ensuring precise and contamination-free transfer. The food processing sector also benefits from their use, as they can convey ingredients like flour, sugar, and spices while maintaining hygiene standards. The equipment's ability to handle different particle sizes, moisture contents, and flow rates makes it versatile for diverse applications, from small-scale on-site production to large-scale industrial operations.
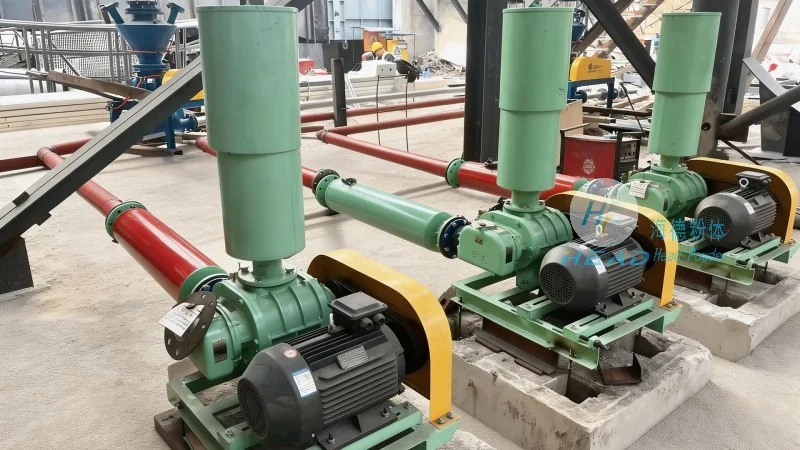
Company Profile
HeadPowder, the brand behind this advanced technology, is represented by Shandong HeadPowder Engineering Co., Ltd., a company based in Shandong, China. With a focus on engineering excellence and customer-centric solutions, HeadPowder specializes in the design, manufacturing, and supply of high-quality pneumatic conveying systems. The company's mobile powder conveying equipment is engineered to meet the rigorous demands of modern industrial applications, combining durability, efficiency, and ease of use. By leveraging years of experience in the field, HeadPowder ensures that its products deliver reliable performance and contribute to enhanced productivity in various work environments.