

Principle and Working Scene Characteristics of Gray Silo Powder Pneumatic Conveying Machine
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced powder handling equipment. This article focuses on the gray silo powder pneumatic conveying machine, exploring its fundamental principles and typical working scenarios to help users understand its application and benefits.
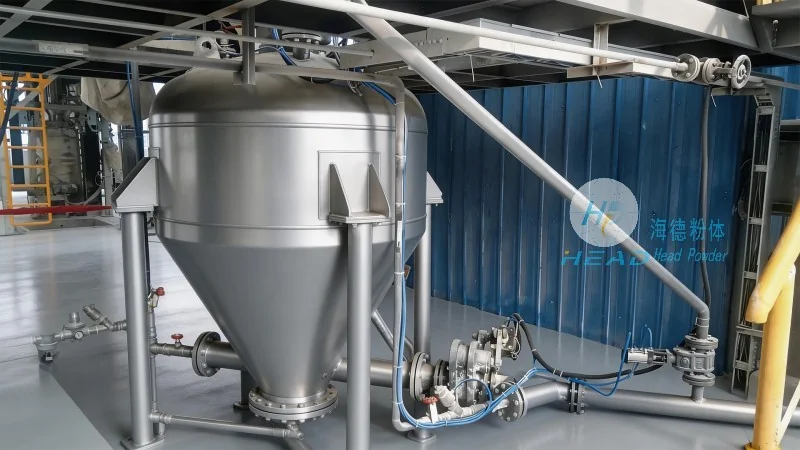
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder is a professional enterprise dedicated to providing high-quality powder conveying solutions. With years of experience in the industry, the company has established itself as a reliable partner for businesses seeking efficient and reliable powder handling systems. The company's headquarters is located in Shandong, China, where it conducts research, development, and manufacturing of its products.
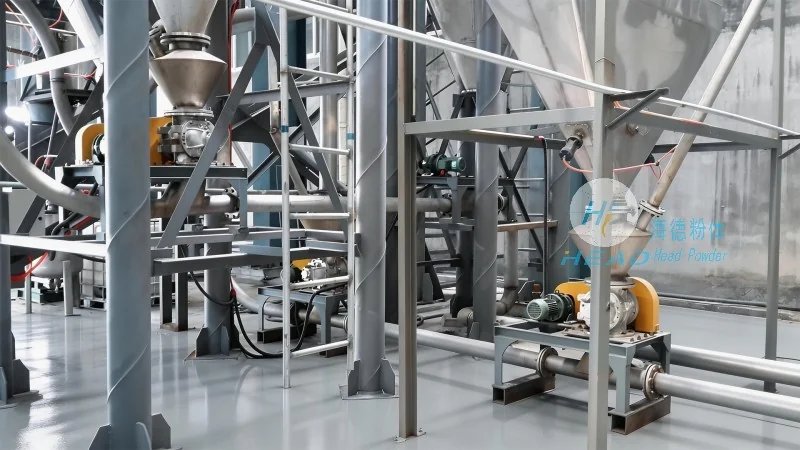
Principle of Pneumatic Conveying Technology
The gray silo powder pneumatic conveying machine operates based on pneumatic conveying technology, which uses compressed air to transport powder materials from the storage silo to the discharge point. The core components include the gray silo (storage tank), air compressor, conveying pipeline, and control system. The process typically involves feeding powder into the silo, activating the air compressor to generate high-pressure air, and then using the air flow to lift and transport the powder through the pipeline to the target location. This method eliminates the need for mechanical components like screws or belts, reducing maintenance costs and improving operational efficiency.
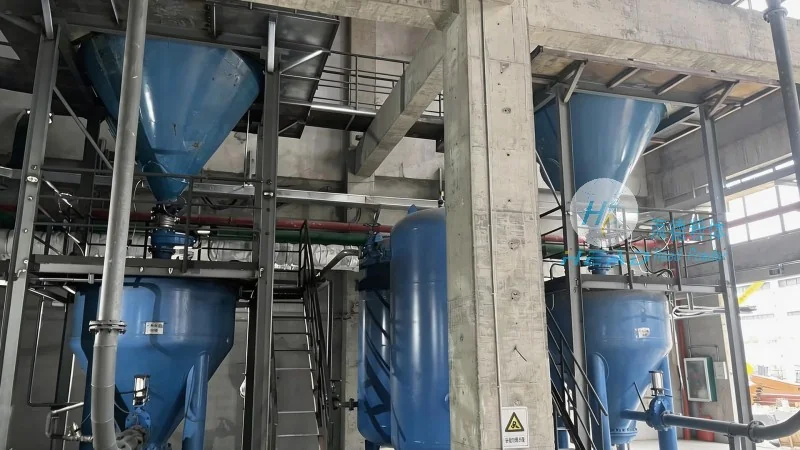
Working Scene Characteristics
The gray silo powder pneumatic conveying machine is widely used in various industrial sectors due to its versatility and adaptability. In the chemical industry, it is commonly employed for transporting powders such as pigments, additives, and raw materials, ensuring precise and clean material transfer. In the food processing industry, the machine is used to handle food-grade powders like flour, sugar, and spices, maintaining hygiene and preventing contamination. Additionally, in the pharmaceutical industry, it plays a crucial role in transporting active pharmaceutical ingredients (APIs) and other sensitive powders, adhering to strict quality and safety standards. The machine's ability to handle different powder types and its low contamination risk make it suitable for applications where product purity is paramount.
Advantages in Different Working Scenarios
In industrial applications, the gray silo powder pneumatic conveying machine offers several advantages that enhance operational performance. Its compact design allows for easy integration into existing production lines, minimizing space requirements. The system is also highly flexible, capable of transporting powders over long distances and varying elevations without significant pressure loss. Furthermore, the machine's automated control system ensures consistent and reliable operation, reducing human intervention and improving overall productivity. These features make it an ideal choice for businesses looking to optimize their powder handling processes and improve efficiency.
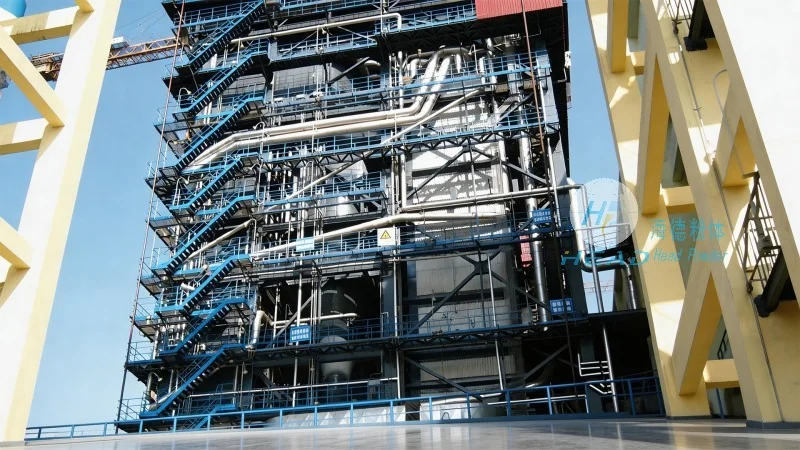
Conclusion
HeadPowder's gray silo powder pneumatic conveying machine is a robust and efficient solution for various powder handling needs. By leveraging pneumatic conveying technology, the machine provides a clean, low-maintenance, and cost-effective method for transporting powders in different industrial applications. With its adaptability and reliability, it continues to be a preferred choice for businesses seeking to enhance their material handling processes. HeadPowder remains committed to delivering high-quality equipment and services to meet the evolving needs of its clients.