

Application and Optimization of Pneumatic Conveying Technology in Quartz Sand Particle Transport Des
HeadPowder, a leading engineering firm based in Shandong, China, specializes in advanced material handling solutions, particularly in the application of pneumatic conveying systems for quartz sand and similar granular materials. The company's expertise lies in optimizing the design and implementation of these systems to ensure efficient, reliable, and cost-effective transport of quartz sand particles.
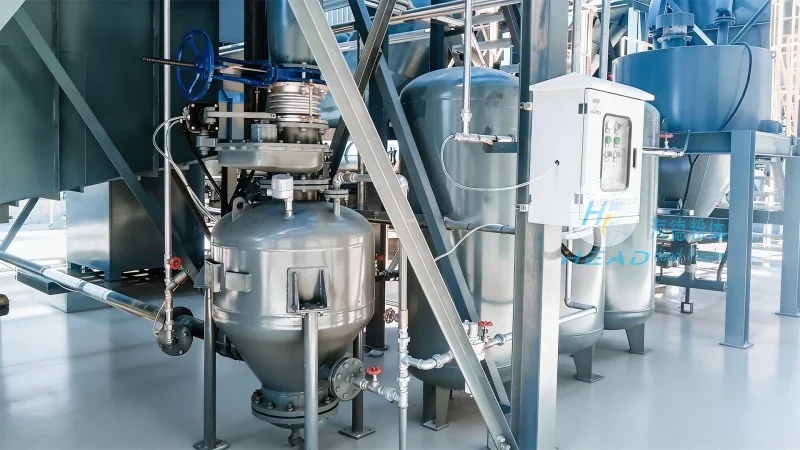
Pneumatic Conveying Technology: Core Principles and Advantages
Pneumatic conveying technology utilizes air or gas to transport bulk materials like quartz sand through a pipeline system. This method offers several key advantages over traditional mechanical conveying solutions. First, it eliminates the need for moving parts such as belts or buckets, reducing maintenance requirements and operational downtime. Second, the system can handle a wide range of particle sizes and densities, making it versatile for various industrial applications. Third, pneumatic conveying provides excellent control over material flow, allowing for precise dosing and distribution. These benefits contribute to improved safety, reduced energy consumption, and enhanced overall system performance.
Application in Quartz Sand Particle Transport: Design Considerations
When designing a pneumatic conveying system for quartz sand, several critical factors must be considered to ensure optimal performance. The first is the particle size distribution and density of the quartz sand, as these properties directly impact the air velocity and pressure required for effective transport. HeadPowder engineers conduct thorough material analysis to determine the appropriate air flow rates and pressure levels. Another crucial aspect is the system layout, including the number and placement of inlets, outlets, and any necessary expansion or separation devices. The design also accounts for the potential for material segregation or agglomeration, which can affect flow characteristics. By carefully addressing these design considerations, the system can achieve high throughput with minimal pressure drop and energy consumption.
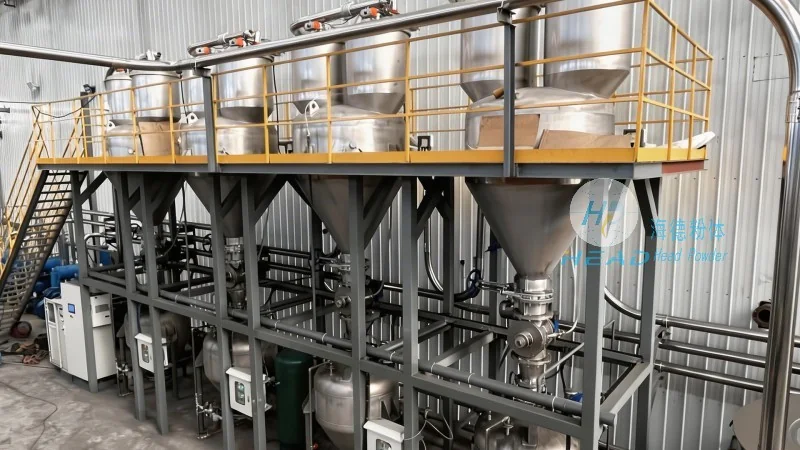
Optimization Strategies for Enhanced Performance
HeadPowder employs several optimization strategies to enhance the performance of pneumatic conveying systems for quartz sand. One key approach is the use of variable frequency drives (VFDs) to control air flow and pressure dynamically, matching the system's output to actual demand. This not only reduces energy waste but also extends the lifespan of components by preventing overloading. Another optimization technique involves implementing advanced control systems that monitor key parameters such as pressure, flow rate, and temperature in real-time. These systems can automatically adjust operating conditions to maintain optimal performance, even under varying load conditions. Additionally, HeadPowder utilizes computational fluid dynamics (CFD) simulations to model the behavior of quartz sand particles within the conveying system, allowing for predictive maintenance and proactive adjustments to improve efficiency.
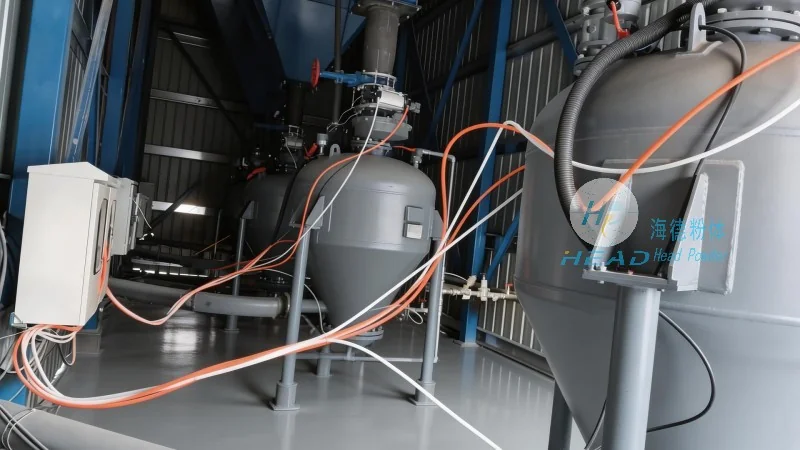
Case Study: Successful Implementation in a Quartz Sand Processing Plant
A recent project for a quartz sand processing plant in Shandong exemplifies the effectiveness of HeadPowder's pneumatic conveying solutions. The client required a system to transport 200 tons of quartz sand per hour from a storage silo to a processing unit, with strict requirements for minimal dust generation and high material purity. HeadPowder's engineering team designed a closed-loop pneumatic conveying system with a positive pressure section for the initial transport and a negative pressure section for the final delivery. The system was equipped with high-efficiency filters to capture any airborne particles, ensuring compliance with environmental regulations. After installation and commissioning, the system achieved a throughput of 220 tons per hour, exceeding the client's expectations. The pressure drop across the system was maintained at a low level, resulting in significant energy savings compared to traditional mechanical conveying methods. The client reported improved operational efficiency and reduced maintenance costs, validating the effectiveness of HeadPowder's optimization strategies.
Conclusion: Advancing Material Handling with Pneumatic Conveying
HeadPowder's application and optimization of pneumatic conveying technology in quartz sand particle transport design represent a significant advancement in material handling solutions. By leveraging advanced engineering principles, state-of-the-art control systems, and continuous optimization techniques, the company ensures that its clients achieve efficient, reliable, and cost-effective transport of quartz sand. The success of projects like the quartz sand processing plant case study demonstrates the practical benefits of these solutions, including increased throughput, reduced energy consumption, and improved safety. As the demand for efficient material handling continues to grow, HeadPowder remains committed to providing innovative solutions that meet the evolving needs of the industry.