

Principle and Working Scenario Characteristics of Automatic Quantitative Powder Pneumatic Conveying
Automatic quantitative powder pneumatic conveying systems represent a sophisticated technology in material handling, designed to transport bulk powders with precision and efficiency. These systems integrate advanced control mechanisms and pneumatic principles to ensure accurate measurement and delivery of powder materials. The core function is to replace traditional manual or semi-automatic methods, offering enhanced automation, consistency, and operational reliability in industrial settings.
Principle of Operation
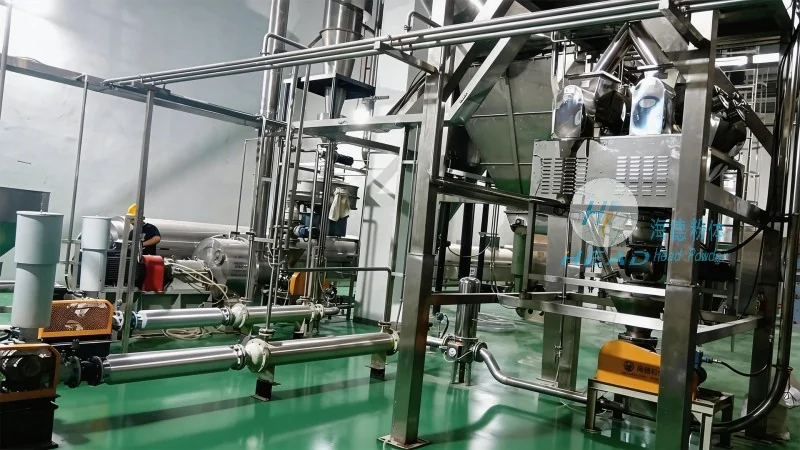
The fundamental principle of these systems revolves around the use of compressed air to create a fluidized state in the powder, enabling it to be conveyed through pipelines. The system typically comprises a hopper, a feeder, a pneumatic conveying line, and a discharge device. The feeder, often equipped with a rotary valve or volumetric meter, controls the flow rate of the powder into the conveying line. Compressed air is introduced at the inlet, creating a pressure differential that propels the powder particles. The key to quantitative accuracy lies in the precise regulation of air flow and powder feed rate, which are synchronized by the system's control unit. This ensures that the delivered quantity matches the setpoint, minimizing material loss and optimizing process efficiency.
Working Scenario Characteristics
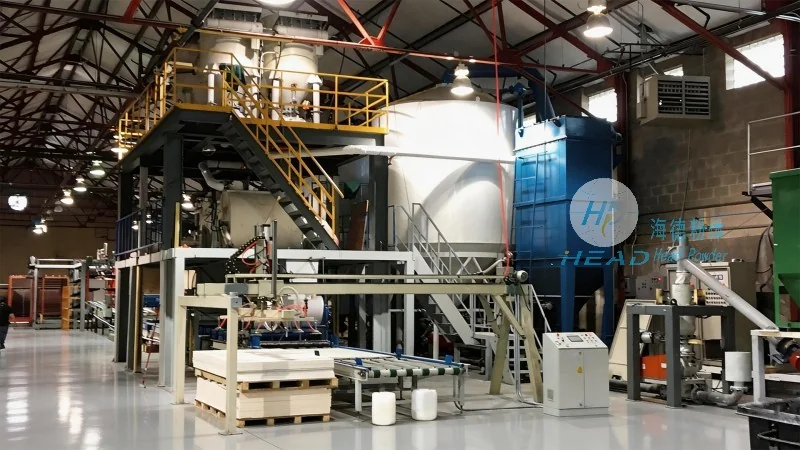
The application scenarios of automatic quantitative powder pneumatic conveying systems are diverse and tailored to various industrial needs. In pharmaceutical manufacturing, for instance, these systems are crucial for handling sensitive powders, where contamination control and precise dosing are paramount. The closed-loop design prevents cross-contamination and maintains product integrity, aligning with stringent regulatory standards. In the food industry, similar systems are employed for transporting ingredients like flour, sugar, or spices, ensuring hygienic handling and accurate portioning for production lines. Additionally, in chemical and mineral processing, these systems facilitate the transport of raw materials or finished products, supporting continuous production processes and reducing downtime. The adaptability of the system allows it to handle different powder properties, such as particle size, density, and moisture content, by adjusting air pressure and flow rates accordingly. This flexibility makes it suitable for both small-scale and large-scale operations, from laboratory settings to industrial plants.
Key Features and Advantages
Automatic quantitative powder pneumatic conveying systems offer several advantages that enhance operational performance and cost-effectiveness. One of the primary benefits is the high level of automation, which reduces the need for manual intervention, thereby minimizing human error and labor costs. The precise control over powder flow ensures consistent product quality, which is critical in industries where uniformity is essential, such as pharmaceuticals and food processing. Furthermore, the closed system design eliminates dust emissions, improving workplace safety and environmental compliance. The compact and modular design of these systems allows for easy integration into existing production lines, reducing installation time and complexity. Maintenance is also simplified due to the use of standardized components and easy access points for inspection and repair. Overall, these systems contribute to increased productivity, reduced material waste, and improved overall operational efficiency.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
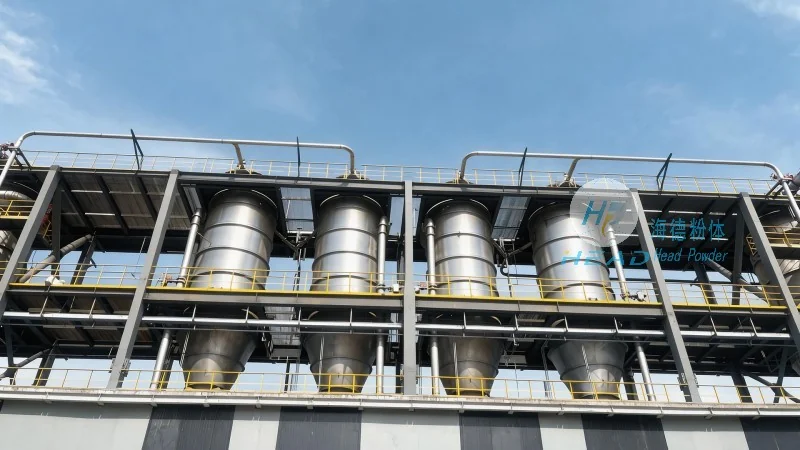
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer specializing in the design, development, and supply of advanced powder handling equipment. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in the industry, providing tailored solutions for diverse material handling challenges. HeadPowder's expertise lies in the integration of cutting-edge technology with practical application, ensuring that their systems meet the specific requirements of each client. The company's products are engineered to deliver reliability, durability, and performance, supported by comprehensive after-sales services and technical support. HeadPowder's facilities are located in Shandong, China, where the company leverages local resources and expertise to maintain high standards of production and customer service. By focusing on customer needs and technological advancement, HeadPowder continues to lead in the field of automatic quantitative powder pneumatic conveying systems, delivering solutions that enhance industrial efficiency and sustainability.