

Principle and Working Scene Characteristics of Nanometer Calcium Carbonate Powder Conveying System E
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer and supplier specializing in powder conveying systems. The company is headquartered in Shandong, China, and has been committed to providing high-quality conveying solutions for various industrial applications. This article will introduce the principle and working scene characteristics of the nanometer calcium carbonate powder conveying system equipment, which is widely used in the production processes of calcium carbonate powder.
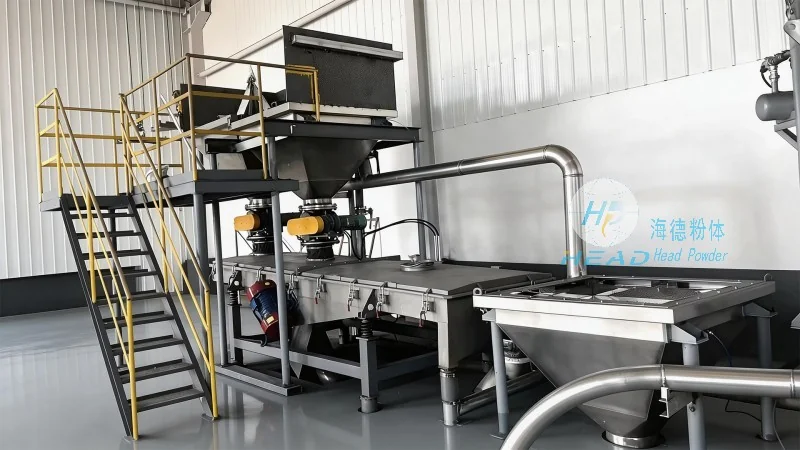
Overview of Nanometer Calcium Carbonate Powder Conveying System Equipment
The nanometer calcium carbonate powder conveying system equipment is a specialized device designed to transport nanometer-sized calcium carbonate powder efficiently and reliably. This equipment is crucial in industries such as chemical manufacturing, plastic processing, and rubber production, where the precise handling of fine powders is essential for maintaining product quality and operational efficiency. The system typically consists of components like feeders, conveying pipes, control units, and dust collection systems, all working in harmony to ensure smooth and continuous powder flow.
Working Principle of the Conveying System
The core principle of the nanometer calcium carbonate powder conveying system is the utilization of air or mechanical forces to move the powder through the conveying pipeline. In many applications, pneumatic conveying is employed, where compressed air is used to create a flow that carries the powder particles. The system may include different types of airlocks, rotary valves, and pressure vessels to control the flow rate and prevent material buildup. The design of the conveying equipment is optimized to handle the low bulk density and high surface area characteristics of nanometer calcium carbonate, ensuring minimal particle degradation and loss during transport.
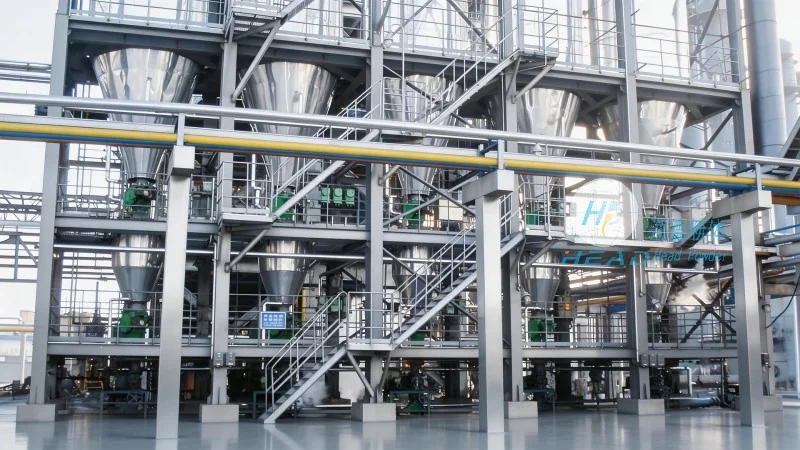
Key Features and Technical Advantages
One of the significant advantages of the nanometer calcium carbonate powder conveying system is its ability to maintain the integrity of the powder particles. The equipment is engineered to minimize friction and impact, which are common causes of particle agglomeration or damage in traditional conveying methods. Additionally, the system offers high conveying capacity and flexibility, allowing it to adapt to varying production demands. The control systems are often equipped with sensors and automation features that enable real-time monitoring and adjustment of the conveying parameters, ensuring optimal performance and reducing downtime.
Working Scene Characteristics and Applications
The nanometer calcium carbonate powder conveying system is widely applied in diverse industrial scenarios. In chemical plants, it is used to transport calcium carbonate from storage silos to processing lines, ensuring a steady supply of raw material. In plastic and rubber manufacturing, the system helps integrate the powder into the production stream, maintaining consistent product properties. The equipment is also suitable for use in environments where dust control is critical, as many models are equipped with advanced dust collection and filtration systems to comply with environmental regulations. The working scene characteristics include the need for high precision, low maintenance, and the ability to handle large volumes of fine powder, making it an indispensable part of modern industrial operations.
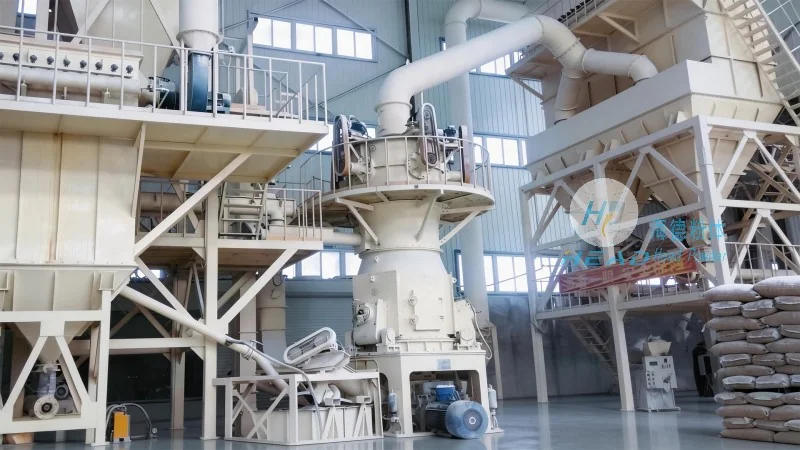
Operational Efficiency and Maintenance Considerations
Efficiency is a key aspect of the nanometer calcium carbonate powder conveying system. The system is designed to minimize energy consumption while maximizing throughput. The use of efficient air compressors and optimized pipeline designs contributes to lower operational costs. Regular maintenance is essential to ensure the longevity and reliability of the equipment. This includes cleaning the conveying lines, inspecting airlocks and valves, and checking the performance of the dust collection system. Proper maintenance not only extends the equipment's lifespan but also maintains the quality of the conveyed powder, preventing contamination and ensuring consistent product output.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides advanced nanometer calcium carbonate powder conveying system equipment that combines innovative technology with practical application. The system's working principle, technical features, and working scene characteristics make it a reliable solution for industries requiring efficient and precise handling of fine powders. By understanding the principles and applications of this equipment, businesses can enhance their production processes, improve product quality, and achieve greater operational efficiency. The company's commitment to quality and customer satisfaction ensures that clients receive tailored solutions that meet their specific needs in the industrial landscape.