

Principle and Working Scene Characteristics of Sand and Gravel Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, production, and supply of advanced pneumatic conveying equipment. Our company, Shandong HeadPowder Engineering Co., Ltd., has been committed to providing efficient and reliable solutions for material handling in various industries. The sand and gravel pneumatic conveying machine is one of our core products, engineered to meet the demands of modern construction and mining sectors.
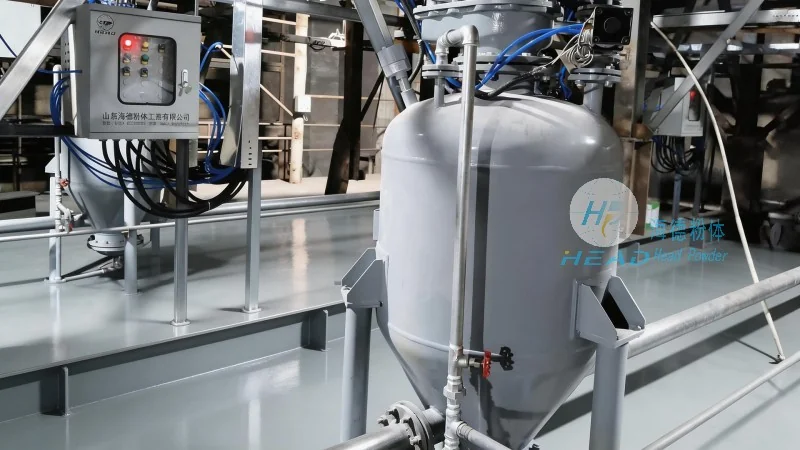
The Principle of Sand and Gravel Pneumatic Conveying
The sand and gravel pneumatic conveying machine operates on the principle of air flow to transport bulk materials. Unlike traditional mechanical conveyors, this equipment uses a closed system where air is compressed and directed through a pipeline to move the material. The process involves several key components, including a blower, a hopper for material storage, a conveying pipe, and a discharge outlet. The blower generates the necessary air pressure to create a flow that pulls the sand and gravel particles into the pipe. As the air flows, it carries the material along the pipeline, ensuring a smooth and continuous transfer. This method eliminates the need for mechanical parts that come into direct contact with the material, reducing wear and maintenance costs. The pneumatic conveying system is designed to handle a wide range of particle sizes and densities, making it versatile for different applications.
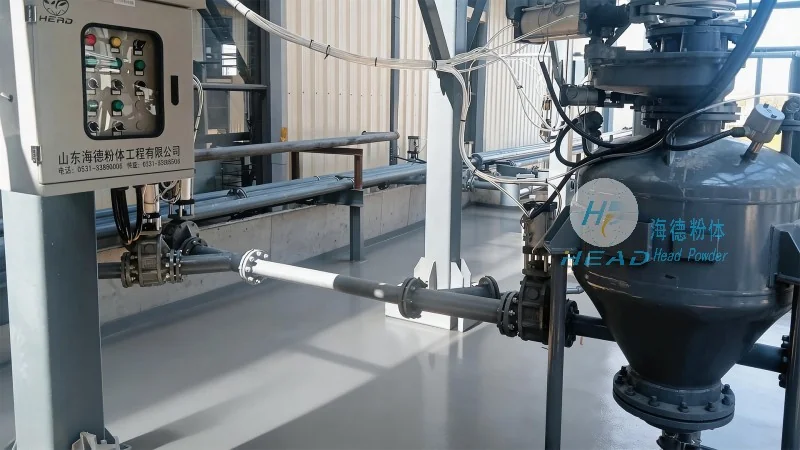
Working Scene Characteristics of Sand and Gravel Pneumatic Conveying Machines
The working scene characteristics of our sand and gravel pneumatic conveying machines are tailored to meet the specific needs of construction sites, mining operations, and aggregate processing facilities. These machines are designed for high efficiency and durability in demanding environments. One of the key features is the ability to handle large volumes of material with minimal labor. The closed system ensures that dust and particles are contained, improving safety and environmental compliance. The equipment is also flexible in terms of layout, as it can be installed in various configurations to fit the space constraints of different work sites. For example, in a construction site, the machine can be used to transport sand and gravel from storage silos to mixing stations, while in a mining operation, it can move crushed rock from processing plants to storage areas. The working scene characteristics also include low energy consumption compared to traditional conveyor systems, which helps in reducing operational costs over time. Additionally, the system is easy to maintain, with accessible components that can be serviced quickly, minimizing downtime.
Application Scenarios and Practical Examples
Our sand and gravel pneumatic conveying machines are widely used in various industrial settings. In the construction industry, they are essential for transporting aggregates to concrete mixing plants, ensuring a steady supply of materials for building projects. The machines can handle different types of sand and gravel, including river sand, crushed stone, and recycled aggregates, adapting to the diverse needs of construction sites. In the mining sector, these equipment are used to transport raw materials from crushers to storage silos, facilitating the processing and distribution of minerals. The pneumatic conveying system is particularly advantageous in areas where traditional conveyors are not feasible due to space limitations or the need to avoid material contamination. For instance, in a quarry, the machine can be installed underground to transport crushed rock from the extraction site to the processing plant, reducing the risk of dust and noise pollution. The working scene characteristics also make these machines suitable for use in remote or difficult-to-access locations, where traditional transportation methods may be impractical. The reliability and efficiency of the sand and gravel pneumatic conveying machine make it a preferred choice for industries that require consistent and high-volume material handling.
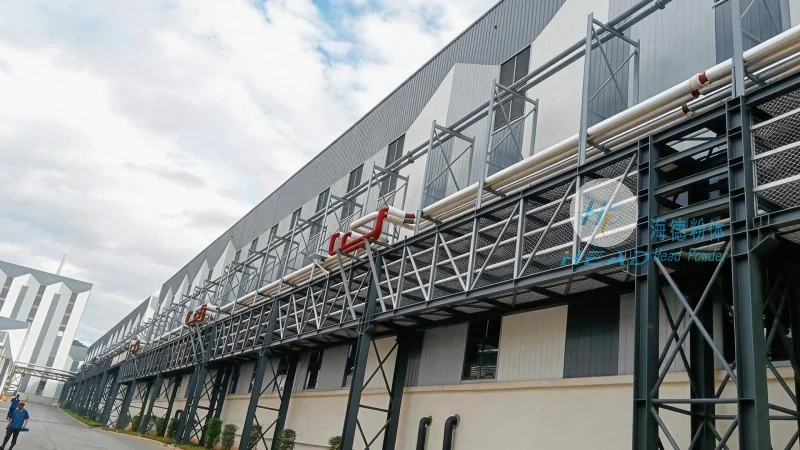
Conclusion and Company Commitment
HeadPowder, with its headquarters in Shandong, China, continues to innovate and improve its pneumatic conveying equipment to meet the evolving needs of the industry. The sand and gravel pneumatic conveying machine exemplifies our commitment to providing high-quality, efficient, and durable solutions. By leveraging advanced technology and rigorous quality control, we ensure that our products meet the highest standards of performance and reliability. Our team of experts is dedicated to understanding the specific requirements of each client and providing tailored solutions that enhance productivity and reduce operational costs. Whether for construction, mining, or other material handling applications, HeadPowder's sand and gravel pneumatic conveying machines offer a reliable and efficient way to transport bulk materials. We are committed to delivering value to our customers and supporting their success in the industry.