

Working Principle and Features of Quartz Stone Powder Pneumatic Conveying Equipment
Quartz stone powder pneumatic conveying equipment is a specialized system designed to transport fine powders like quartz stone powder through the use of air pressure. This equipment is widely used in various industrial applications where efficient and dust-free material handling is crucial. The following sections will explore the working principle and key features of such equipment, providing a comprehensive understanding of its functionality and benefits.
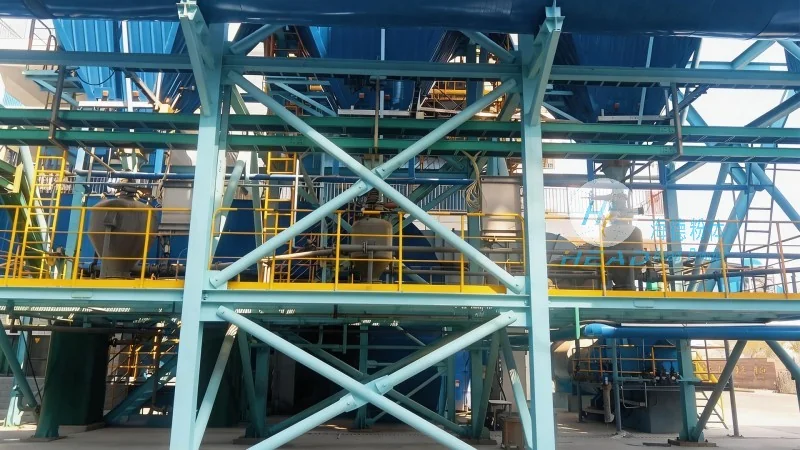
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems. With a strong focus on quality and innovation, the company has established itself as a trusted provider of equipment tailored to the specific needs of the quartz stone powder industry. The equipment offered by HeadPowder is engineered to ensure reliable and efficient material transport, meeting the demands of modern industrial processes.
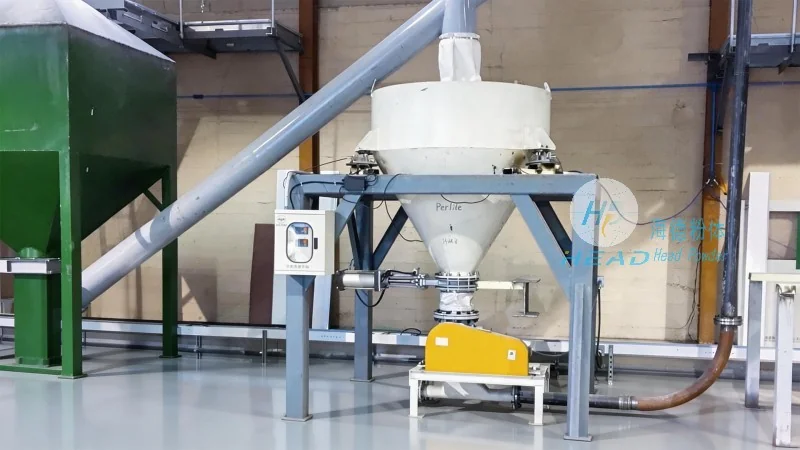
Working Principle of Quartz Stone Powder Pneumatic Conveying Equipment
The core of quartz stone powder pneumatic conveying equipment lies in its ability to use air as the medium for transporting powder. The system typically operates by creating a pressure differential between the source and destination points. At the source, the quartz stone powder is introduced into a hopper or feeder, where it is then drawn into a pipeline by a vacuum or pressure source. The air, often mixed with the powder, moves through the pipeline to the discharge point, where the powder is separated from the air and collected. This process eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational efficiency. The equipment ensures a continuous and controlled flow of powder, minimizing material loss and contamination.
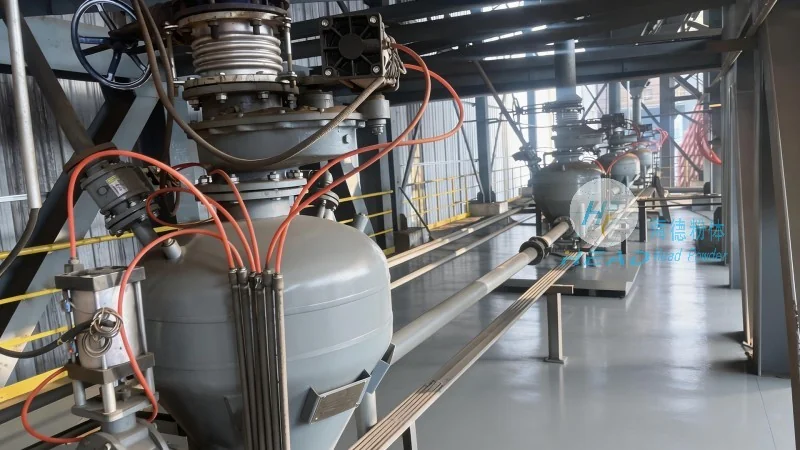
Key Features of Quartz Stone Powder Pneumatic Conveying Equipment
Several key features distinguish quartz stone powder pneumatic conveying equipment from traditional material handling methods. Firstly, it offers a dust-free operation, which is critical for maintaining a clean and safe working environment, especially in industries where fine powders are handled. The enclosed system prevents dust from being released into the air, reducing the risk of respiratory issues and contamination of other materials. Secondly, the equipment provides high efficiency in terms of material transport, with the ability to move large quantities of powder over long distances with minimal energy consumption. This is achieved through optimized air flow and pipeline design, which minimizes pressure drop and energy loss. Thirdly, the system is highly flexible and can be easily integrated into existing production lines. It can handle various particle sizes and moisture contents, making it suitable for a wide range of quartz stone powder applications. Additionally, the equipment is designed for low maintenance, with durable components that can withstand the abrasive nature of quartz stone powder, ensuring long-term reliability and cost-effectiveness.