

Working Principle and Characteristics of Bag-Added Powder Pneumatic Conveying Systems
For industries dealing with bulk powder handling, efficient and reliable material transport is crucial. One advanced solution is the bag-added powder pneumatic conveying system, which offers a flexible and effective method for moving dry powders. This article explores the working principle and key characteristics of such systems, highlighting how they enhance operational efficiency and product integrity.
Understanding the Working Principle of Bag-Added Powder Pneumatic Conveying
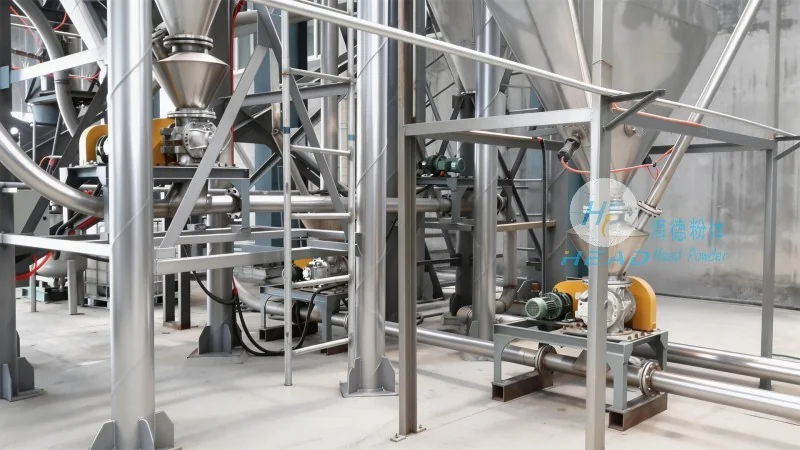
The bag-added powder pneumatic conveying system operates by using compressed air to transport dry powders from a source to a destination. The process begins with the addition of powders into a bag or hopper, which then feeds the material into the conveying line. As compressed air is introduced, it creates a flow that lifts and moves the powder particles through the pipeline. This method relies on the principle of pneumatic transport, where the air velocity and pressure are carefully controlled to ensure smooth material movement without degradation or segregation.
Key components of this system include the feeding hopper, the air compressor, the conveying pipeline, and the discharge unit. The feeding hopper is designed to accommodate bulk powders, often with a bag or container that can be easily opened and emptied. The air compressor generates the necessary pressure to drive the material through the pipeline. The pipeline itself is typically made of durable materials like stainless steel or plastic, ensuring resistance to corrosion and wear from the powders. The discharge unit then delivers the material to the target location, such as a silo, storage tank, or processing equipment.
Key Characteristics of Bag-Added Powder Pneumatic Conveying Systems
Several notable characteristics make bag-added powder pneumatic conveying systems a preferred choice for many industries. First, they offer high flexibility in material handling, allowing for the transport of various powder types, including fine, coarse, and abrasive powders. The system can handle different flow rates and distances, making it adaptable to diverse operational needs. Second, the bag-feeding mechanism provides a controlled and consistent material flow, reducing the risk of clogging or uneven discharge. This consistency is vital for maintaining product quality and preventing contamination.
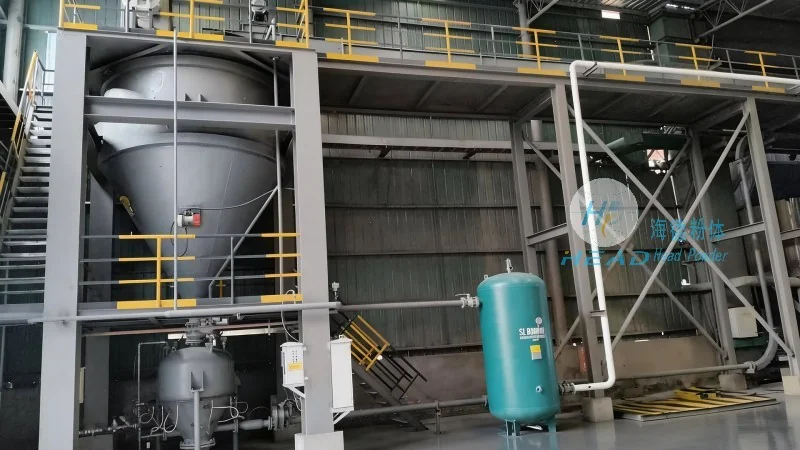
Another significant characteristic is the ability to handle long-distance transport without the need for multiple transfer points. The pneumatic system can move powders over several hundred meters or more, depending on the setup, with minimal loss or degradation. This reduces the need for additional equipment and labor, leading to cost savings and increased efficiency. Additionally, the system is relatively compact and can be integrated into existing facilities, making it a suitable solution for both new and retrofit applications.
Advantages and Applications in Industrial Settings
The bag-added powder pneumatic conveying system offers several advantages that make it ideal for industries such as pharmaceuticals, food processing, chemicals, and minerals. These advantages include improved product safety, as the system minimizes direct human contact with powders, reducing the risk of contamination and exposure to hazardous materials. The enclosed design also helps maintain product integrity, preventing moisture absorption or oxidation that could affect the quality of the powder.
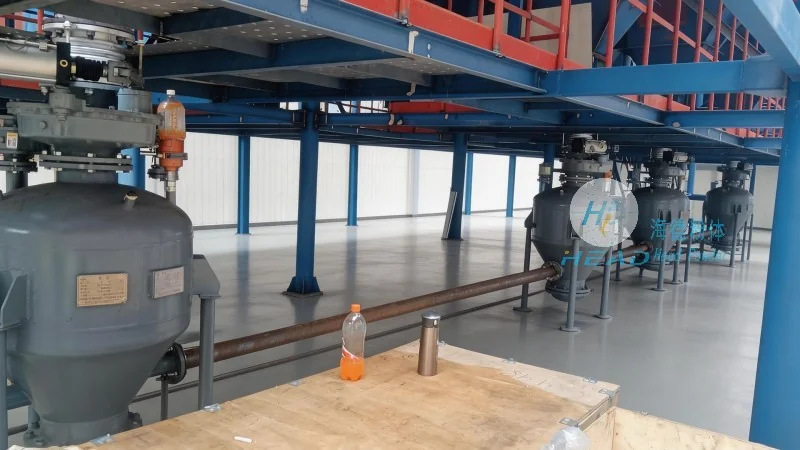
In the pharmaceutical industry, for example, the system is used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the final product meets strict quality standards. In the food industry, it handles ingredients like flour, sugar, and spices, maintaining hygiene and preventing cross-contamination. The chemical industry utilizes it for transporting raw materials and intermediates, while the minerals sector uses it for processing and transporting powders like cement, coal, and ores.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading provider of powder handling solutions, specializes in designing and manufacturing advanced pneumatic conveying systems. With years of experience in the industry, the company has developed a reputation for delivering high-quality, reliable equipment tailored to the specific needs of its clients. HeadPowder's headquarters is located in Shandong, China, where the company operates a state-of-the-art manufacturing facility and research center.
The company's team of engineers and technicians work closely with clients to understand their operational challenges and provide customized solutions. By leveraging cutting-edge technology and rigorous quality control processes, HeadPowder ensures that its systems meet the highest industry standards. The company's commitment to innovation and customer satisfaction has made it a trusted partner for businesses seeking efficient and effective powder handling solutions.