

Working Principle and Features of Broad Bean Material Handling Systems
HeadPowder, a leading manufacturer based in Shandong, China, specializes in designing and manufacturing efficient broad bean material handling systems. These systems are engineered to streamline the processing and transportation of broad beans, ensuring optimal performance in agricultural and food processing applications.
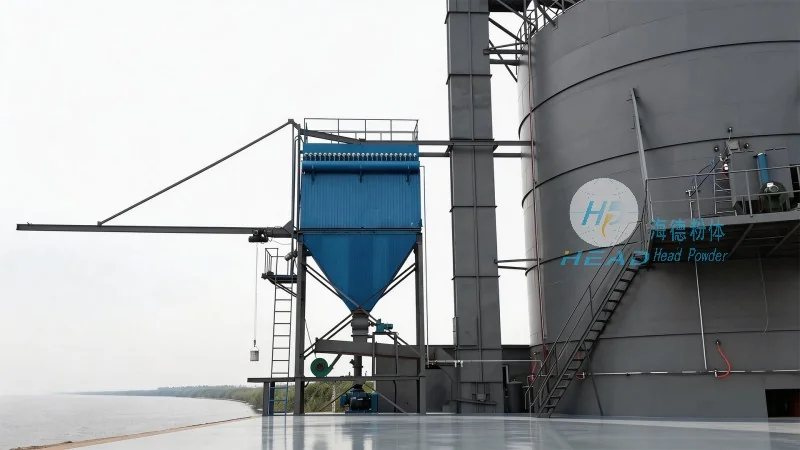
Working Principle of Broad Bean Material Handling Systems
The core working principle of a broad bean material handling system involves a series of integrated components that work in tandem to move, sort, and process broad beans. At its foundation, the system typically includes a feeding mechanism, a conveyor system, and a control unit. The feeding mechanism, often a hopper or a feeding belt, collects broad beans from the source and feeds them into the conveyor. The conveyor, which may be a belt conveyor or a screw conveyor depending on the design, transports the beans through the system. Driven by electric motors or other power sources, the conveyor ensures consistent and reliable movement of the material. Along the conveyor path, there may be additional components such as classifiers, which separate beans based on size or quality, and cleaning devices that remove impurities like dust or debris. The control unit, equipped with sensors and automation technology, monitors the entire process, adjusting the speed and direction of the conveyor as needed to maintain efficiency and product quality.
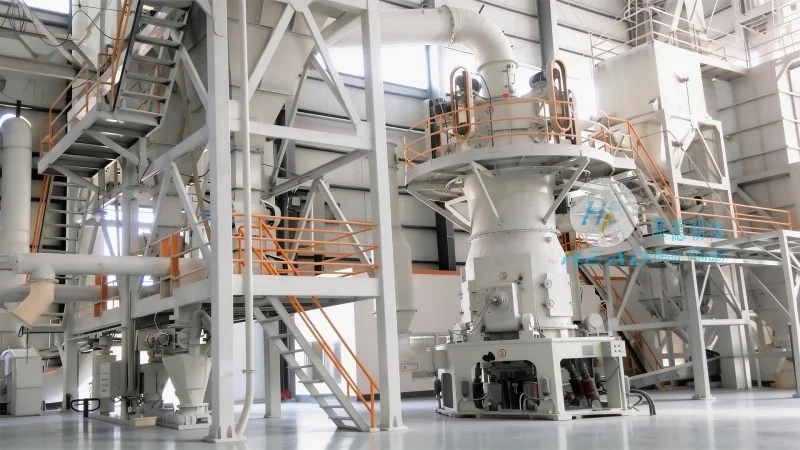
Key Features of Broad Bean Material Handling Systems
Broad bean material handling systems from HeadPowder are characterized by several key features that enhance their performance and adaptability. One of the primary features is high efficiency, achieved through optimized conveyor speeds and automated controls that minimize downtime and maximize throughput. The systems are also designed for durability, using robust materials and components that can withstand the rigors of continuous operation in agricultural and processing environments. Another notable feature is versatility, as these systems can be customized to handle different bean sizes, shapes, and processing requirements. This adaptability makes them suitable for various applications, from initial sorting and cleaning to packaging and storage. Additionally, the systems prioritize safety and hygiene, incorporating features like enclosed conveyor sections to prevent contamination and easy-to-clean surfaces that meet food industry standards. The integration of advanced sensors and monitoring technology further enhances operational reliability, providing real-time data on system performance and alerting operators to any issues that may arise.
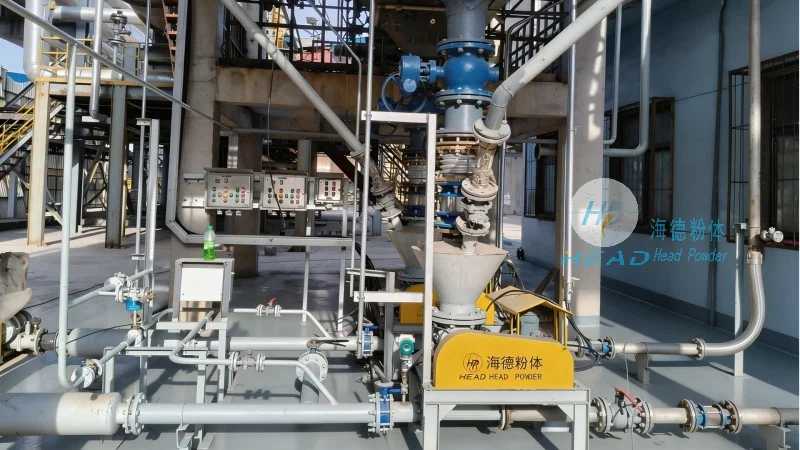
Application and Benefits
Broad bean material handling systems are widely used in the agricultural and food processing industries to improve the efficiency and quality of broad bean handling. By automating the transportation and processing of broad beans, these systems reduce labor costs and minimize the risk of human error. The consistent and reliable operation of the conveyor system ensures that beans are handled gently, preserving their quality and reducing damage. Furthermore, the ability to sort and clean beans in a single system streamlines the overall processing workflow, leading to higher productivity and better product consistency. For businesses operating in the broad bean sector, investing in a high-quality material handling system from HeadPowder can lead to significant operational improvements and increased profitability.