

Working Principle and Features of Bag Breaker Pneumatic Conveying System Equipment
Bag breaker pneumatic conveying system equipment, as a key component in modern material handling and processing industries, plays a crucial role in efficiently handling bulk materials while breaking open sealed bags. This article provides an in-depth exploration of the working principle and key features of such systems, offering insights into their design, functionality, and practical applications.
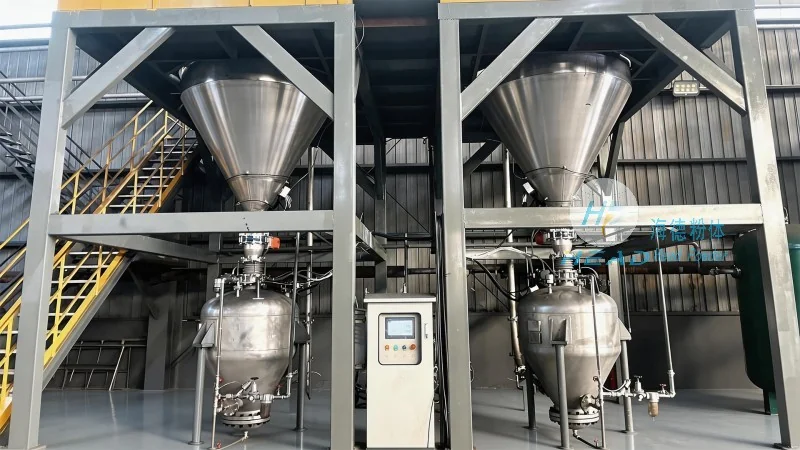
Overview of Bag Breaker Pneumatic Conveying Systems
Bag breaker pneumatic conveying systems are engineered to automate the process of material transfer from sealed bags to processing equipment. These systems integrate bag opening mechanisms with pneumatic conveying technology, enabling seamless material flow from the bag to the target destination. The primary goal is to enhance operational efficiency, reduce labor costs, and maintain material integrity during the transfer process.
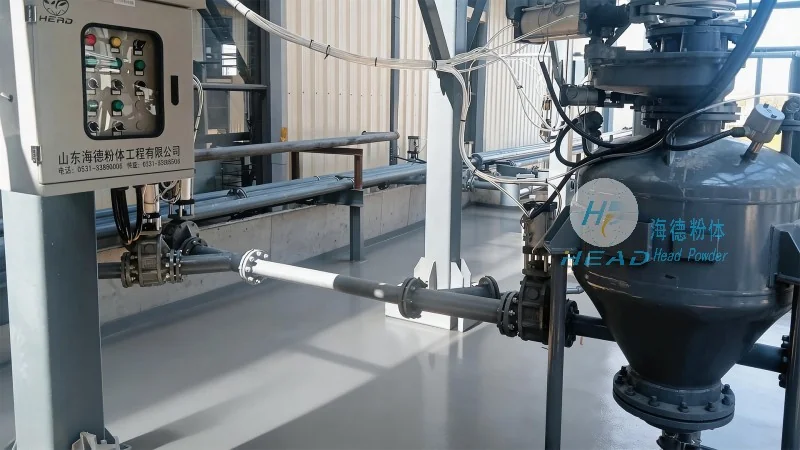
Working Principle of the System
The operation of a bag breaker pneumatic conveying system typically involves several sequential steps. Initially, a sealed bag is placed on a feeding platform or hopper. The system then activates a bag opening device, which may include a mechanical cutter, pneumatic actuator, or other specialized tools, to rupture the bag and release its contents. Once the bag is broken, the material is drawn into the conveying line by a vacuum or pressure source, depending on the system configuration. The conveying line transports the material to the processing equipment or storage area. The entire process is often automated, with sensors and control systems monitoring the flow and ensuring consistent operation.
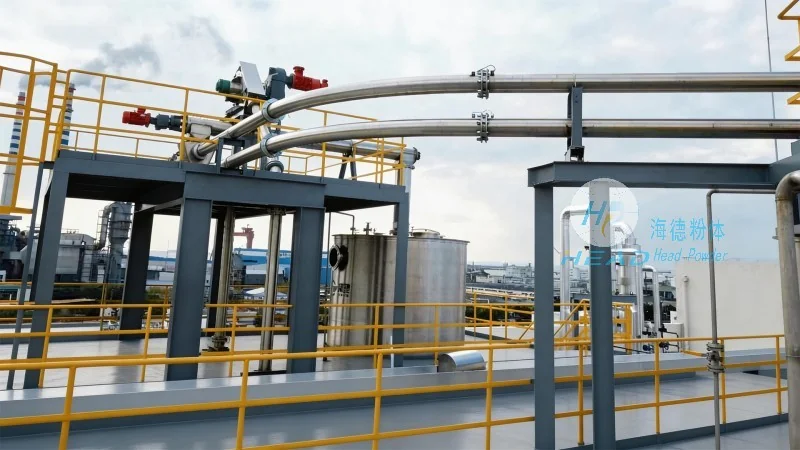
Key Features of the Equipment
HeadPowder, a leading manufacturer based in Shandong, China, offers advanced bag breaker pneumatic conveying systems with several distinctive features. These systems are designed for durability and reliability, featuring robust construction to withstand heavy-duty industrial environments. The bag opening mechanism is precision-engineered to ensure consistent and efficient bag rupture, minimizing material loss and contamination. Additionally, the pneumatic conveying components are optimized for energy efficiency, reducing operational costs while maintaining high material transfer rates. The systems also incorporate user-friendly control interfaces, allowing operators to easily monitor and adjust parameters as needed. Furthermore, HeadPowder's equipment is customizable to meet specific material characteristics and application requirements, ensuring optimal performance in diverse industrial settings.
Advantages in Material Handling
The integration of bag breaking and pneumatic conveying offers significant advantages in material handling operations. By eliminating manual bag opening and material transfer, these systems reduce human error and improve safety in the workplace. The automated process also enhances productivity, as materials can be transferred continuously without interruption. Moreover, the systems help maintain material quality by preventing exposure to air and contaminants during the transfer process. This is particularly important for sensitive materials such as powders, granules, and fine particles, where moisture and contamination can affect product quality and performance.
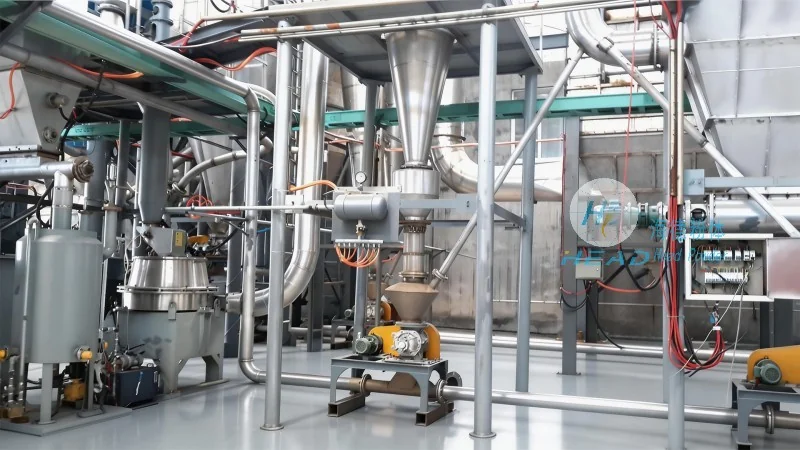
Application Scenarios
Bag breaker pneumatic conveying systems are widely used in various industries, including pharmaceuticals, food processing, chemical manufacturing, and bulk material handling. In pharmaceutical applications, these systems ensure the safe and hygienic transfer of raw materials and finished products, adhering to strict regulatory standards. In the food industry, they facilitate the handling of dry ingredients like flour, sugar, and spices, maintaining product freshness and safety. Chemical manufacturers benefit from the efficient transfer of powders and granules, reducing dust and improving process control. Overall, the systems provide a reliable solution for material handling in environments where speed, accuracy, and material integrity are critical.