

Working Principle and Features of Automatic Tonne Bag Feeding Pneumatic Conveying System Equipment
HeadPowder, a leading provider in the field of material handling solutions, specializes in advanced pneumatic conveying systems designed to streamline bulk material processing. This article delves into the working principle and key features of the automatic tonne bag feeding pneumatic conveying system, a cutting-edge solution that enhances operational efficiency and reliability in industrial applications.
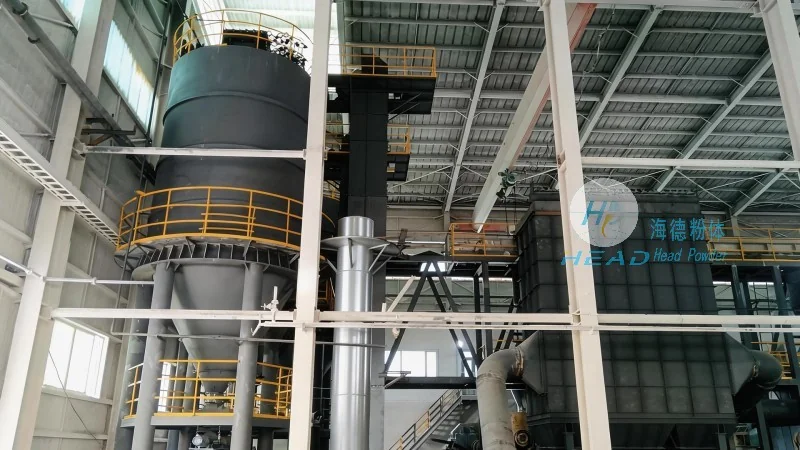
Company Overview and Expertise
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, is dedicated to delivering high-quality engineering solutions for material handling. With years of experience in the industry, HeadPowder has established itself as a trusted partner for businesses seeking reliable and efficient pneumatic conveying systems. The company's commitment to innovation and customer satisfaction drives the development of advanced equipment that meets the evolving needs of modern industrial operations.
Introduction to the Automatic Tonne Bag Feeding Pneumatic Conveying System
The automatic tonne bag feeding pneumatic conveying system is a sophisticated piece of equipment engineered to automate the process of transferring bulk materials from tonne bags into processing lines. This system is particularly valuable in industries such as chemicals, food processing, pharmaceuticals, and mining, where handling large quantities of powders and granules requires precision and consistency. By integrating advanced automation and pneumatic technology, the system ensures seamless material transfer while minimizing human intervention and operational risks.
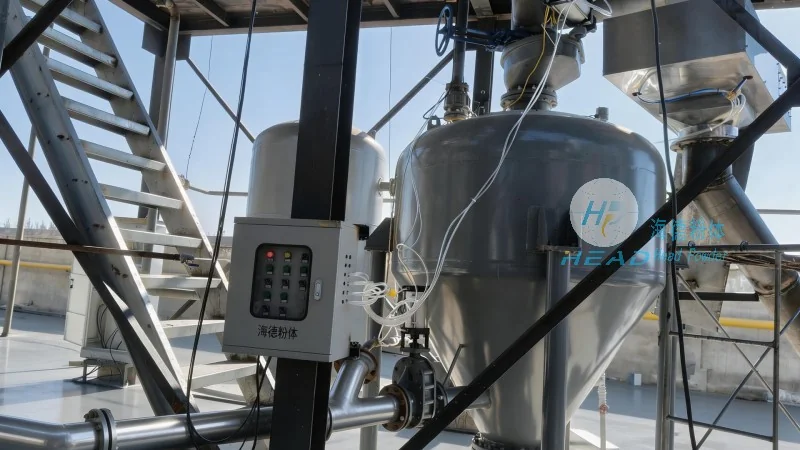
Working Principle of the System
The core of the automatic tonne bag feeding pneumatic conveying system lies in its pneumatic conveying mechanism, which utilizes air pressure to move materials through a network of pipes. The process begins with the automatic opening of a tonne bag, followed by the controlled discharge of material into a hopper or feeder. The system employs a combination of positive and negative pressure air flow to transport the material efficiently. The key components include a bag opener, a material hopper, a rotary valve, and a pneumatic conveyor line. The bag opener uses mechanical or pneumatic force to break the seal of the tonne bag, allowing the material to fall into the hopper. The rotary valve then regulates the flow of material into the conveyor line, while the pneumatic system generates the necessary air pressure to move the material through the pipes to the destination point. The system is equipped with sensors and control panels to monitor and adjust the flow rate, ensuring optimal performance and preventing blockages or overloading.
Key Features and Advantages
The automatic tonne bag feeding pneumatic conveying system offers several distinct features that set it apart from traditional manual or semi-automatic systems. Firstly, it provides high automation levels, reducing the need for manual labor and minimizing the risk of human error. The system can handle various types of materials, including powders, granules, and fine particles, with consistent performance. Another notable feature is its ability to maintain a clean and dust-free environment, which is crucial in industries where contamination control is paramount. The system also offers flexibility in terms of layout and integration with existing processing lines, allowing for easy adaptation to different facility configurations. Additionally, the system is designed for durability and low maintenance, ensuring long-term operational reliability and cost-effectiveness.
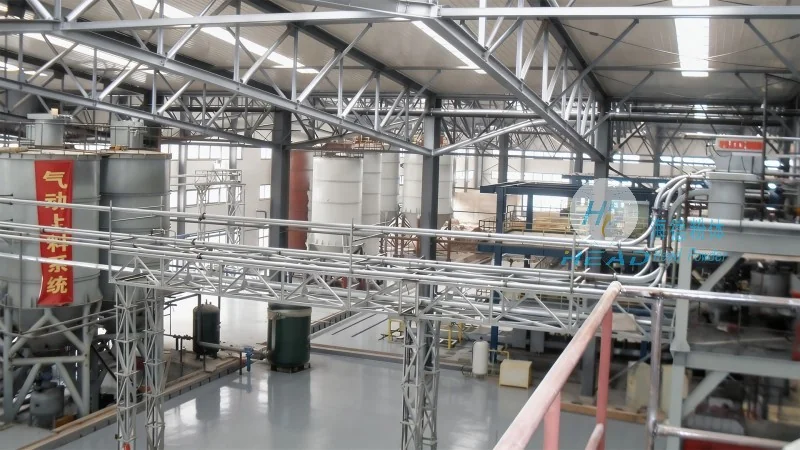
Operational Benefits and Applications
Implementing the automatic tonne bag feeding pneumatic conveying system brings numerous operational benefits to industrial facilities. The primary advantage is the significant improvement in productivity, as the system can process large volumes of material at a consistent rate, reducing downtime and increasing throughput. The automation feature also enhances safety by minimizing the exposure of workers to hazardous materials and reducing the risk of accidents. Furthermore, the system's ability to maintain a clean environment helps in meeting regulatory compliance and quality standards, which is essential in industries such as food and pharmaceuticals. The system is widely applicable in various industries, including chemical manufacturing, where it is used for transporting raw materials and intermediates; in food processing, for handling ingredients like flour and sugar; and in mining, for transporting ore and minerals. The versatility of the system makes it a valuable asset for any facility dealing with bulk materials.
Conclusion
In conclusion, the automatic tonne bag feeding pneumatic conveying system is a highly efficient and reliable solution for bulk material handling. With its advanced working principle and comprehensive features, the system offers significant advantages in terms of productivity, safety, and operational flexibility. As a leading provider, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide cutting-edge solutions that meet the evolving needs of modern industry. By leveraging the expertise and technology of HeadPowder, businesses can enhance their material handling processes and achieve greater operational efficiency and success.