

Working Principle and Features of a Cobalt Hydroxide Pneumatic Conveying System
For industrial applications requiring efficient and reliable material handling, the cobalt hydroxide pneumatic conveying system stands out as a sophisticated solution. This system is designed to transport cobalt hydroxide, a critical component in various industries, with precision and minimal loss. Understanding its working principle and key features is essential for optimizing operational efficiency and ensuring consistent performance.
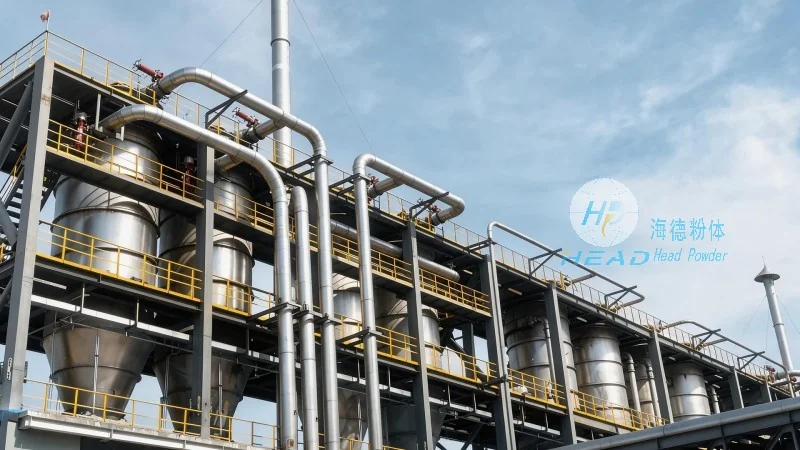
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for businesses seeking to enhance their material transport processes. HeadPowder's expertise lies in tailoring systems to meet specific industrial requirements, ensuring that clients receive customized solutions that address their unique challenges.
Working Principle of the Cobalt Hydroxide Pneumatic Conveying System
The cobalt hydroxide pneumatic conveying system operates on the principle of air-based transport, utilizing a combination of pressure and vacuum to move material through a network of pipes. The process begins with the material being introduced into a hopper or feeder, where it is then conveyed by a stream of air under controlled pressure. The system typically employs a positive pressure or a combination of positive and negative pressure, depending on the distance and layout of the conveying line. As the material travels through the pipeline, it is suspended in the air stream, allowing for smooth and continuous movement. The system includes components such as air blowers, filters, and control valves that regulate the air flow and material transport, ensuring optimal performance and preventing blockages or material degradation.
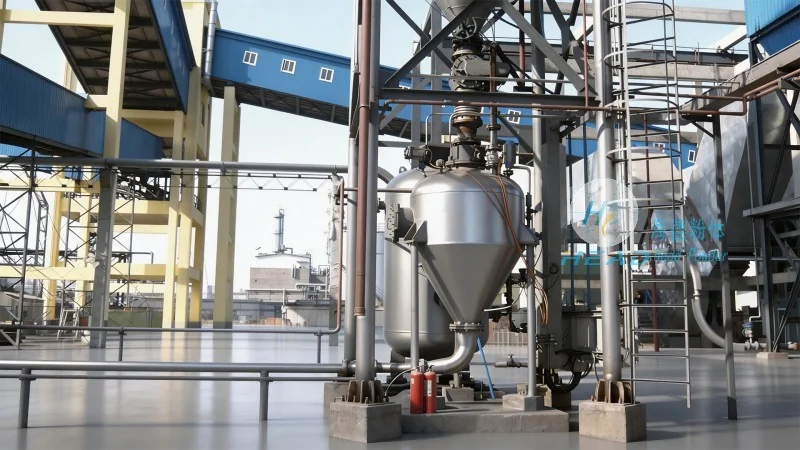
Key Features and Advantages of the System
The cobalt hydroxide pneumatic conveying system offers several distinct advantages that make it an ideal choice for industrial applications. One of the primary features is its ability to handle fine powders like cobalt hydroxide without causing segregation or agglomeration. The system's design minimizes material loss and contamination, which is crucial for maintaining product quality. Additionally, the system provides high transport efficiency, allowing for rapid and continuous material movement over long distances. Another key feature is its flexibility, as it can be easily integrated with existing production lines and adapted to different operational needs. The system also offers low maintenance requirements, with components that are durable and resistant to corrosion, ensuring long-term reliability. Furthermore, the pneumatic conveying method reduces the risk of dust exposure and improves workplace safety compared to traditional mechanical conveying methods.
Customization and Integration Capabilities
Shandong HeadPowder Engineering Co., Ltd. offers comprehensive customization options to suit the specific needs of each client. The company's engineers work closely with clients to design systems that align with their production processes, ensuring seamless integration and optimal performance. Whether for short or long-distance transport, the system can be configured to handle varying material volumes and flow rates. The integration of advanced control systems allows for real-time monitoring and adjustment of the conveying parameters, enhancing operational control and efficiency. Additionally, the system can be equipped with features such as dust collection and filtration, further improving environmental compliance and product purity.
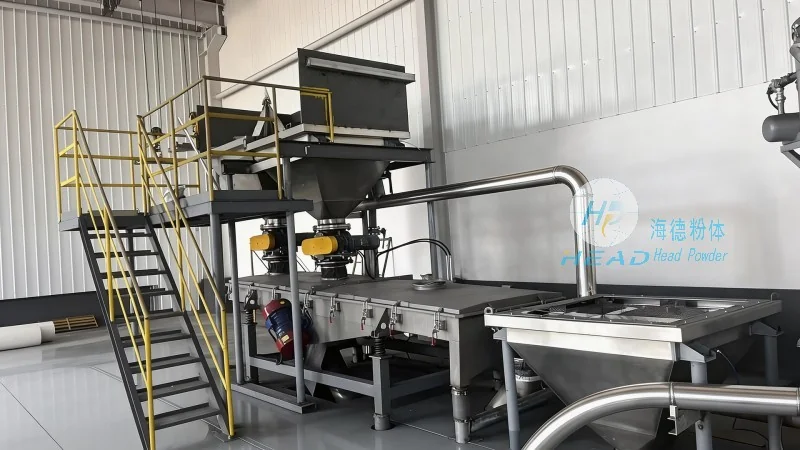
Operational Benefits and Performance Metrics
Implementing a cobalt hydroxide pneumatic conveying system from HeadPowder delivers significant operational benefits. The system's ability to maintain consistent material flow rates reduces downtime and improves production throughput. By minimizing material degradation and loss, the system helps preserve product quality, which is vital for meeting industry standards and customer expectations. The low maintenance design of the system translates to reduced operational costs over time, as fewer repairs and replacements are required. Furthermore, the system's energy efficiency, achieved through optimized air flow and blower selection, contributes to lower utility expenses. Performance metrics such as conveying velocity, pressure drop, and material handling capacity are carefully engineered to meet the specific demands of each application, ensuring reliable and consistent operation.
Quality Assurance and Compliance
HeadPowder adheres to stringent quality assurance protocols to ensure the reliability and performance of its pneumatic conveying systems. All components are manufactured using high-quality materials that are resistant to corrosion and wear, ensuring long-term durability. The system undergoes rigorous testing and validation to confirm compliance with industry standards and client specifications. This commitment to quality extends to the entire production process, from design and manufacturing to installation and commissioning. By maintaining strict quality control measures, HeadPowder ensures that its systems deliver consistent performance and meet the highest industry standards.