

Activated Carbon Particle Pneumatic Conveying System: Pioneering the Intelligent and Efficient New E
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional engineering company based in Shandong, China. The company specializes in the design, manufacturing, and installation of advanced material handling systems, with a focus on providing efficient solutions for the transportation of bulk materials like activated carbon particles.
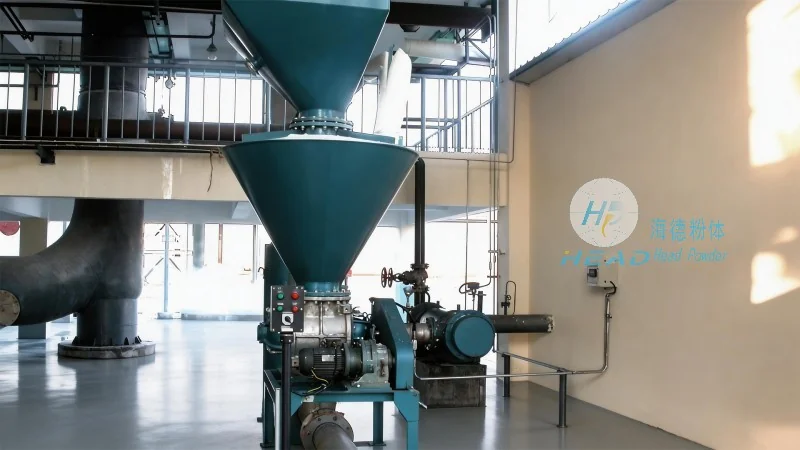
Activated Carbon Particle Pneumatic Conveying System
The Activated Carbon Particle Pneumatic Conveying System is a state-of-the-art solution developed by HeadPowder to address the challenges associated with transporting activated carbon particles. This system leverages pneumatic conveying technology to achieve seamless, dust-free, and highly efficient movement of activated carbon, ensuring minimal product degradation and optimal operational performance.
Key Features and Technical Advantages
The system incorporates several innovative features that enhance its performance and reliability. For instance, it utilizes advanced control systems that allow for precise regulation of air flow and pressure, ensuring consistent and stable conveying of activated carbon particles. Additionally, the design incorporates high-quality materials and components that are resistant to corrosion and wear, extending the system's service life and reducing maintenance costs.
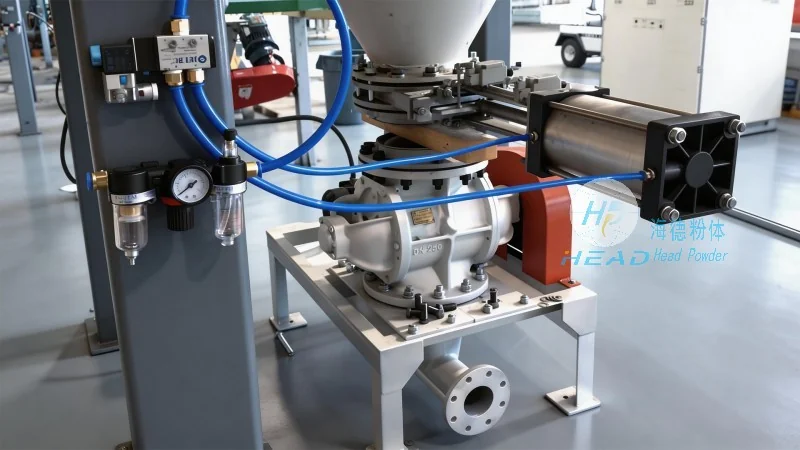
System Components and Operation Principle
The system typically consists of several key components, including a hopper for material storage, a rotary valve for controlled discharge, a conveying line with appropriate fittings and valves, and a receiver for the deposited material. The operation principle involves feeding activated carbon particles into the hopper, where they are then discharged through the rotary valve into the conveying line. Compressed air is then introduced into the line, creating a pressure differential that propels the particles through the system to the receiver. This process is highly efficient, as it eliminates the need for mechanical conveyors and reduces the risk of product contamination.
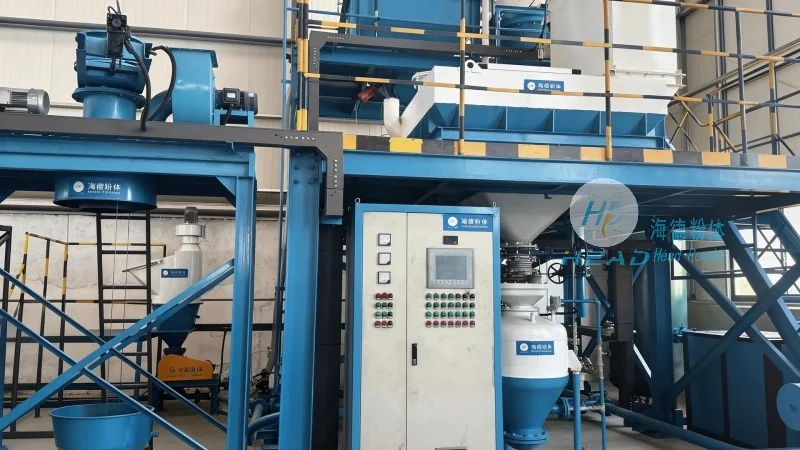
Application Scenarios
The Activated Carbon Particle Pneumatic Conveying System is widely used in various industrial applications where the efficient handling of activated carbon is critical. These include chemical plants, water treatment facilities, pharmaceutical manufacturing sites, and environmental remediation projects. The system's ability to handle fine particles without clogging or loss makes it an ideal choice for industries that require high-purity and consistent product quality.
Benefits and Advantages
By adopting the Activated Carbon Particle Pneumatic Conveying System, industries can achieve significant improvements in operational efficiency, product quality, and safety. The system's ability to convey activated carbon particles in a dust-free environment reduces health hazards and environmental pollution, while its precise control capabilities ensure minimal product loss and consistent quality. Furthermore, the system's compact design and low maintenance requirements make it a cost-effective solution for long-term material handling needs.