

Introduction to Tank Truck Pneumatic Conveying System Equipment and Structural Principles
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced tank truck pneumatic conveying systems. This article provides a comprehensive overview of the equipment, its structural principles, and key components, highlighting the technology's efficiency and reliability in material handling applications.
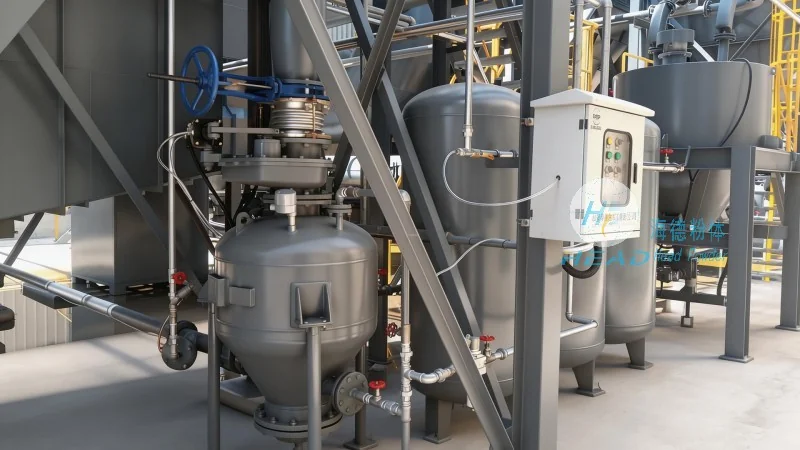
Overview of Tank Truck Pneumatic Conveying System Equipment
The tank truck pneumatic conveying system is a sophisticated industrial solution designed to transport bulk materials from a storage tank to a processing or packaging unit. At the core of this system is the tank truck itself, which serves as the primary container for the material. The system integrates various components that work in tandem to ensure smooth and efficient material transfer. These components include the tank truck's internal piping, the conveying pipeline, and the control system that regulates the flow of material and air.
Structural Principles of the Pneumatic Conveying System
The structural design of the tank truck pneumatic conveying system is built on the principle of pneumatic transport, which utilizes air pressure to move materials through a pipeline. The system typically operates under positive pressure, where compressed air is introduced into the material container to create a flow of material along the pipeline. Key structural elements include the tank truck's hopper, which funnels material into the conveying line, and the pipeline network that connects the truck to the receiving equipment. The control system, often equipped with sensors and valves, manages the air pressure and material flow to prevent blockages and ensure consistent performance.
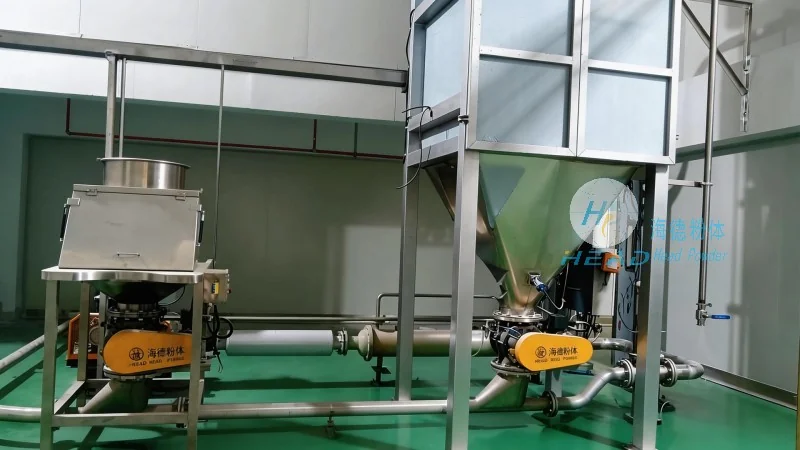
Key Components and Their Functions
Several critical components make up the tank truck pneumatic conveying system, each playing a vital role in the overall operation. The tank truck's tank, usually made of stainless steel or other corrosion-resistant materials, stores the bulk material. The hopper, located at the bottom of the tank, is designed with a specific angle to facilitate material discharge. The conveying pipeline, which may include bends, elbows, and expansion joints, is engineered to handle the material's characteristics, such as particle size and moisture content. The air compressor and associated air treatment equipment provide the necessary compressed air to drive the material through the system. The control panel, equipped with pressure gauges, flow meters, and safety valves, allows operators to monitor and adjust the system parameters in real-time. Additionally, the system may include filters and cyclones to separate the material from the air, ensuring clean and efficient operation.
Advantages of the Tank Truck Pneumatic Conveying System
Implementing a tank truck pneumatic conveying system offers numerous advantages for industrial operations. One of the primary benefits is the ability to transport materials over long distances without the need for intermediate storage or manual handling. The system reduces labor costs by automating the material transfer process and minimizes the risk of material contamination or spillage. Furthermore, the enclosed pipeline design prevents dust emissions, enhancing workplace safety and compliance with environmental regulations. The system's flexibility allows for easy integration with existing production lines and can be adapted to handle a wide range of materials, including powders, granules, and bulk solids. The reliability of the system, with proper maintenance, ensures consistent performance and reduces downtime, contributing to overall operational efficiency.
Application Examples and Industry Use Cases
The tank truck pneumatic conveying system is widely used across various industries, including chemical, pharmaceutical, food processing, and mining. In the chemical industry, it is commonly employed to transport powders like cement, plastics, and pigments from tank trucks to processing plants. The pharmaceutical sector utilizes this system to handle sensitive materials, ensuring contamination-free transfer and maintaining product quality. In food processing, the system is ideal for conveying ingredients such as flour, sugar, and spices, where hygiene and cleanliness are paramount. The mining industry benefits from the system's ability to transport bulk minerals and ores from mine sites to processing facilities, improving operational efficiency and reducing transportation costs. Each application leverages the system's ability to handle diverse materials and maintain consistent flow rates, making it a versatile solution for material handling needs.
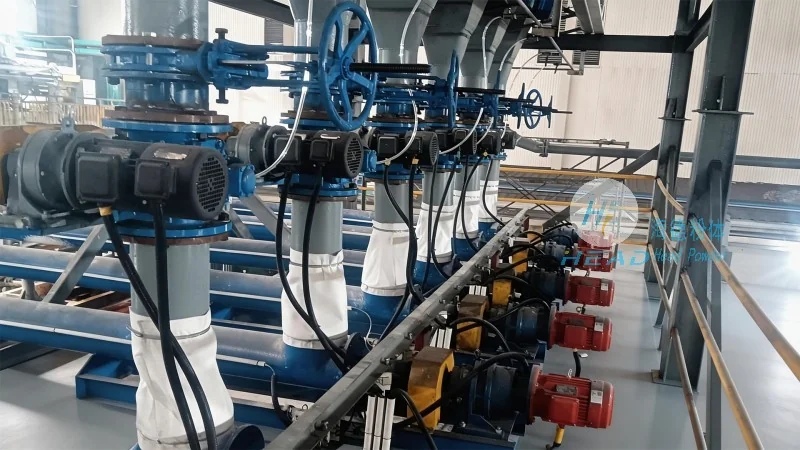
Maintenance and Operational Considerations
Proper maintenance is crucial to ensure the longevity and optimal performance of the tank truck pneumatic conveying system. Regular inspections of the tank truck's tank and hopper for signs of wear or corrosion are essential. The conveying pipeline should be checked for blockages or leaks, which can affect system efficiency. The air compressor and treatment equipment require routine maintenance, including filter changes and lubrication, to maintain air quality and prevent system failure. The control system's sensors and valves should be calibrated periodically to ensure accurate monitoring and control of the material flow. Operators should follow the manufacturer's guidelines for start-up and shutdown procedures to prevent damage to the system components. Additionally, training staff on proper operation and emergency procedures enhances safety and operational efficiency. By adhering to a comprehensive maintenance schedule, users can maximize the system's lifespan and minimize downtime, ensuring consistent performance in material handling operations.
Conclusion
The tank truck pneumatic conveying system, as exemplified by the products from Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated and efficient solution for bulk material transport. Its structural design, based on pneumatic principles, and integrated components provide reliable performance across various industrial applications. The system's advantages, including automation, reduced labor costs, and environmental compliance, make it a preferred choice for industries handling diverse materials. With proper maintenance and operational practices, this technology continues to enhance productivity and operational efficiency in material handling processes. HeadPowder's commitment to quality and innovation ensures that their tank truck pneumatic conveying systems meet the evolving needs of modern industrial operations, providing reliable and efficient solutions for material transport.