

Operation Process and Working Principle of Barley Material Handling System
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced material handling systems. This article provides a detailed overview of the operation process and working principles of a barley material handling system, highlighting the key components and their functions to ensure efficient and reliable barley processing.
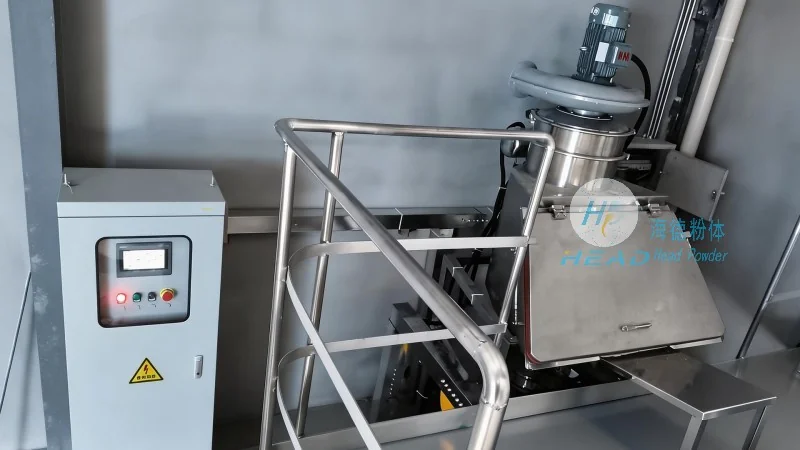
Introduction to Barley Material Handling Systems
Barley is a crucial raw material in the production of malt, beer, and other food and beverage products. Efficient handling of barley from receipt to processing is essential for maintaining product quality and operational efficiency. The barley material handling system designed by HeadPowder Engineering Co., Ltd. integrates various equipment and processes to streamline the flow of barley, from unloading to storage and preparation for further processing.
Key Components of the Barley Material Handling System
The system comprises several critical components that work in tandem to ensure smooth operation. These include:
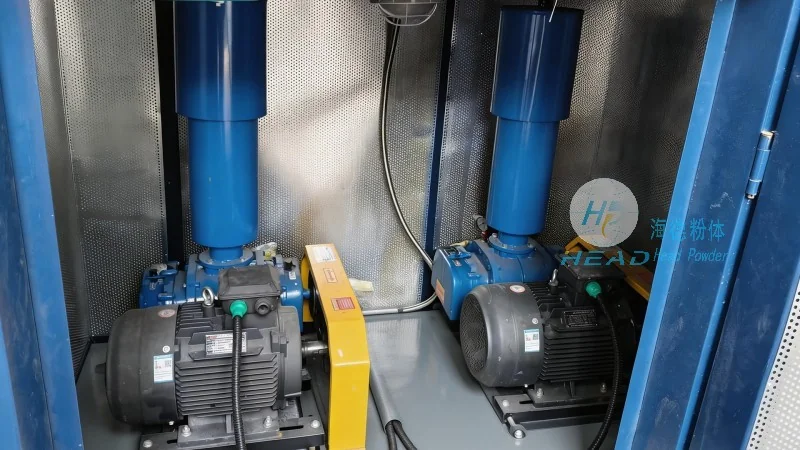
- Unloading Equipment: The process begins with the unloading of raw barley from trucks or railcars. This is typically achieved using hydraulic or mechanical unloaders that efficiently transfer the grain from the transport vehicle to the storage or processing area.
- Conveying Systems: Once unloaded, the barley is transferred to storage silos or processing units via a network of conveyors. These may include belt conveyors, screw conveyors, or pneumatic conveyors, depending on the system design and the specific requirements of the facility.
- Storage Silos: Large-capacity storage silos are used to store the barley until it is needed for processing. These silos are equipped with aeration systems to maintain optimal moisture and temperature levels, preventing spoilage and ensuring the grain remains in good condition.
- Processing Equipment: The system includes processing equipment such as cleaning machines, de-stoners, and graders to remove impurities and ensure the barley meets quality standards. This step is crucial for producing high-quality malt and other products.
- Control and Monitoring Systems: Advanced control systems are integrated into the operation to monitor and regulate the flow of barley through each stage. These systems use sensors and automation to ensure consistent performance and minimize downtime.
Operation Process of the Barley Material Handling System
The operation of the barley material handling system follows a systematic sequence of steps to ensure efficient processing. The process begins with the arrival of raw barley at the facility:
- Arrival and Unloading: Barley trucks or railcars arrive at the facility. The unloading equipment, such as a bucket elevator or a rotary unloader, is activated to transfer the grain from the vehicle to the initial conveyor system.
- Initial Cleaning and Screening: The barley is passed through a series of cleaning and screening equipment to remove dust, dirt, and other foreign materials. This step ensures that only clean, high-quality grain proceeds to the next stage.
- Storage in Silos: After cleaning, the barley is conveyed to the storage silos. The aeration system in the silos maintains the grain's moisture and temperature, preventing mold growth and maintaining its quality.
- Pre-processing: When the barley is needed for processing, it is retrieved from the silos and transferred to the processing equipment. This may involve further cleaning, de-stoning, or sorting to meet the specific requirements of the final product.
- Processing and Packaging: The processed barley is then used in the production of malt or other products. The system ensures that the grain is handled gently to preserve its quality and characteristics.
Working Principles of the Barley Material Handling System
The working principles of the barley material handling system are based on the principles of material flow and automation. The system is designed to minimize manual intervention and maximize efficiency by integrating various components into a cohesive operation. Key principles include:
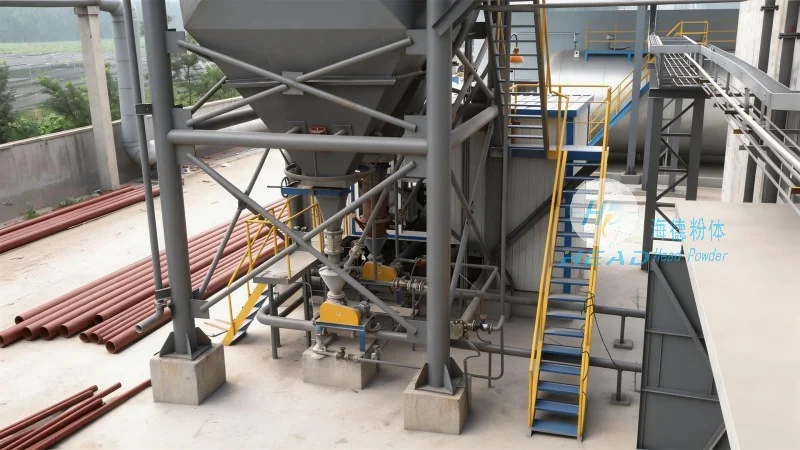
- Continuous Flow: The system operates on a continuous flow basis, ensuring that barley moves smoothly from one stage to the next without interruptions. This minimizes downtime and maximizes production output.
- Automation and Control: Advanced control systems monitor and regulate the operation of each component, ensuring that the system operates within optimal parameters. This includes monitoring temperature, moisture, and flow rates to maintain product quality.
- Energy Efficiency: The system is designed to be energy-efficient, using appropriate equipment and controls to minimize energy consumption while maintaining performance.
- Safety and Maintenance: The system incorporates safety features and regular maintenance schedules to ensure safe operation and minimize equipment downtime.
Benefits of the Barley Material Handling System
The barley material handling system developed by HeadPowder Engineering Co., Ltd. offers several benefits to manufacturers, including:
- Improved Efficiency: The integrated system streamlines the flow of barley, reducing processing time and increasing overall efficiency.
- Enhanced Product Quality: The cleaning and processing steps ensure that the barley meets high quality standards, resulting in better tasting and more consistent products.
- Reduced Labor Costs: Automation minimizes the need for manual labor, reducing labor costs and improving safety.
- Scalability: The system is designed to be scalable, allowing manufacturers to expand their operations as their needs grow.
Conclusion
HeadPowder Engineering Co., Ltd. provides comprehensive solutions for barley material handling systems, combining advanced technology with expert engineering to meet the specific needs of manufacturers. The operation process and working principles of the system ensure efficient, reliable, and high-quality barley processing, contributing to the success of food and beverage production. With a focus on innovation and customer satisfaction, HeadPowder continues to lead the industry in material handling solutions.