

Operation Process and Working Principle of Corn Kernel Powder Conveying Line
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of advanced corn kernel powder conveying systems. Our corn kernel powder conveying lines are engineered to efficiently handle the transportation of corn kernels from storage to processing units, ensuring smooth and reliable operation in agricultural and food processing industries.
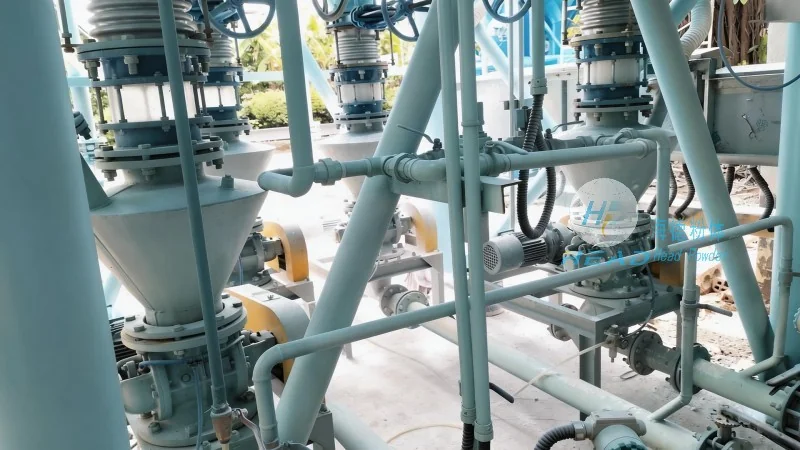
Overview of Corn Kernel Powder Conveying Line
The corn kernel powder conveying line is a comprehensive system designed to manage the flow of corn kernels from initial storage to subsequent processing stages. It integrates various components such as feeders, conveyors, control panels, and safety mechanisms to ensure optimal performance and minimal downtime. This system is crucial for industries that rely on consistent and efficient corn kernel handling, including feed mills, food processing plants, and biofuel production facilities.
Key Components and Their Functions
The operation of a corn kernel powder conveying line involves several key components, each playing a vital role in the overall process. The primary components include:
- Feeding Hopper: This component is responsible for storing and feeding the corn kernels into the system. It is typically equipped with a discharge gate or a rotary valve to regulate the flow rate, ensuring a steady supply of material to the conveyor.
- Pneumatic or Mechanical Conveyors: Depending on the specific application and material characteristics, the conveying line may use either pneumatic (air-assisted) or mechanical (belt or screw) conveyors. Pneumatic systems are ideal for long-distance or high-volume transport, while mechanical conveyors offer reliable performance for shorter distances and heavier loads.
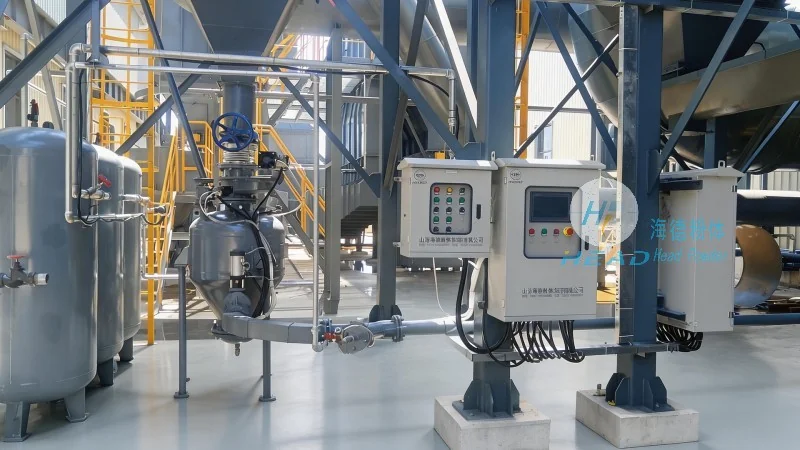
- Control Panel: The control panel houses the electrical and electronic systems that monitor and regulate the operation of the conveying line. It includes sensors for level detection, flow monitoring, and safety interlocks to prevent accidents and ensure compliance with operational standards.
- Safety and Maintenance Features: To enhance operational safety and longevity, the system incorporates features such as emergency stop buttons, overload protection, and regular maintenance indicators. These features help minimize downtime and reduce the risk of equipment failure.
Operation Process of the Conveying Line
The operation of the corn kernel powder conveying line follows a systematic sequence of steps, ensuring the efficient movement of corn kernels from the storage hopper to the processing unit. The process typically begins with the loading of corn kernels into the feeding hopper. Once the hopper is filled, the discharge gate or rotary valve opens, allowing the kernels to flow into the conveyor system.
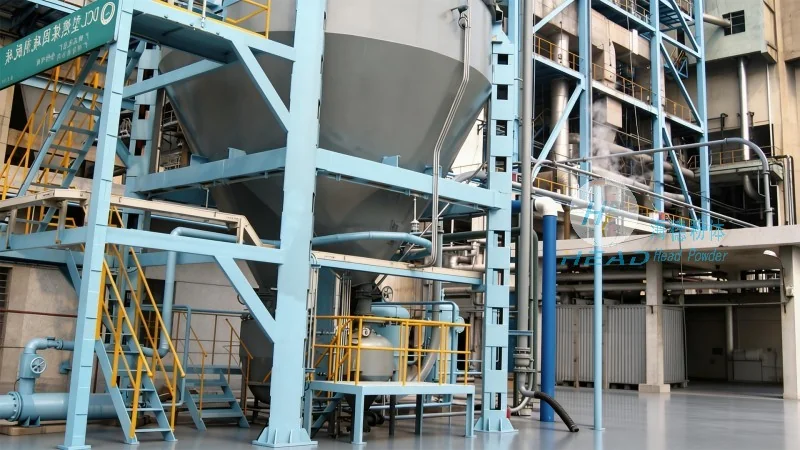
For pneumatic conveying systems, the corn kernels are mixed with air and transported through a network of pipes. The air pressure and flow rate are carefully controlled to maintain the desired velocity and prevent material buildup or blockages. In mechanical conveying systems, the kernels are moved along a belt or screw, with the speed and tension adjusted to handle the specific load and distance.
As the corn kernels travel through the conveyor, they pass through various sections, including bends, elevators, and transition points. These components are designed to minimize friction and energy loss, ensuring the kernels reach the destination without damage or degradation. The control panel continuously monitors the system's performance, adjusting parameters as needed to maintain optimal flow rates and pressure levels.
Working Principle of the Conveying Line
The working principle of the corn kernel powder conveying line is based on the principles of fluid dynamics and mechanical motion. In pneumatic systems, the corn kernels are suspended in a stream of air, which provides the necessary force to move the material through the pipeline. The air pressure is generated by a blower or compressor, and the system is designed to maintain a consistent pressure gradient to ensure smooth transport.
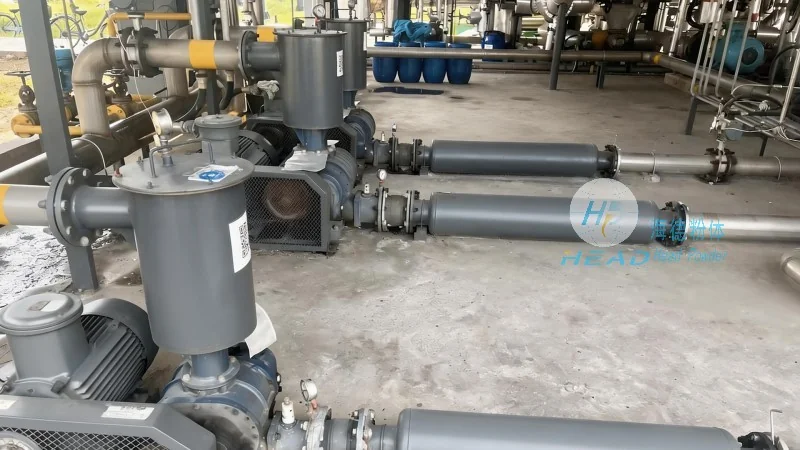
In mechanical systems, the corn kernels are conveyed by the movement of a belt or screw, which applies a continuous force to move the material forward. The speed of the conveyor is controlled by a motor, and the tension is adjusted to prevent slippage or breakage. The system is equipped with sensors that detect the position and speed of the material, providing real-time feedback to the control panel.
The overall working principle is to create a continuous and controlled flow of corn kernels from the source to the destination, minimizing energy consumption and maximizing efficiency. The system is designed to handle varying loads and conditions, ensuring reliable operation under different operational scenarios.
Advantages and Applications
The corn kernel powder conveying line offers several advantages that make it an ideal solution for industries requiring efficient and reliable corn kernel handling. These advantages include:
- High Efficiency: The system is designed to handle high volumes of corn kernels with minimal energy consumption, reducing operational costs.
- Reliability and Durability: The components are constructed from high-quality materials and designed to withstand the rigors of continuous operation, ensuring long service life.
- Flexibility: The system can be customized to meet the specific requirements of different applications, including varying distances, load capacities, and environmental conditions.
- Safety: The incorporation of safety features and monitoring systems ensures that the operation is safe for personnel and the environment.
Applications of the corn kernel powder conveying line include feed mills, where corn kernels are processed into animal feed; food processing plants, where corn is used in the production of cereals, snacks, and other food products; and biofuel facilities, where corn is converted into ethanol or other renewable energy sources.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides advanced corn kernel powder conveying lines that combine efficiency, reliability, and safety. Our systems are designed to meet the specific needs of various industries, ensuring smooth and consistent operation. By leveraging our expertise in engineering and manufacturing, we deliver solutions that enhance productivity and reduce operational costs for our clients.