

Principle and Working Scene Characteristics of Air-Driven Transport for Water Glass Materials
HeadPowder, a leading provider in the field of material handling solutions, specializes in advanced air-driven transport systems tailored for the efficient and reliable movement of water glass materials. This article delves into the fundamental principles behind air-driven transport technology and explores the key characteristics of its application scenarios, offering insights into how such systems enhance operational efficiency in industrial settings.
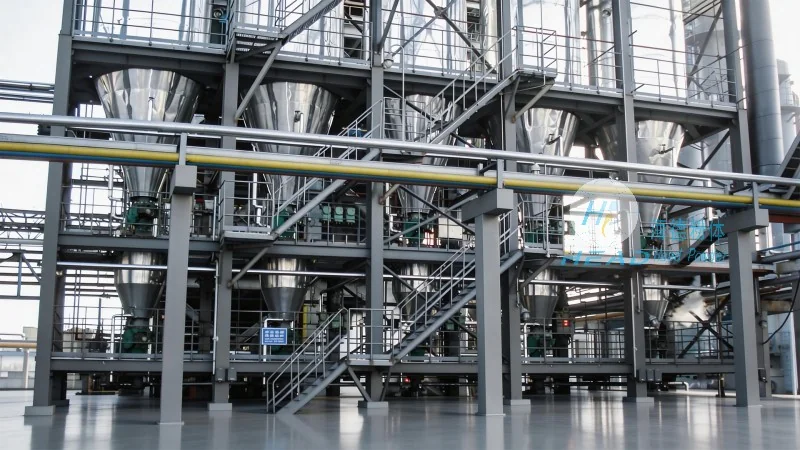
Understanding the Core Principles of Air-Driven Transport for Water Glass Materials
At the heart of air-driven transport systems lies the utilization of air as the primary medium to convey materials through a network of pipes or ducts. For water glass materials, which often present unique challenges in terms of moisture content, viscosity, and particle size distribution, the design of these systems must address specific physical and chemical properties. The fundamental principle involves creating a pressure differential—either through suction (negative pressure) or pressure (positive pressure)—to generate airflow that propels the material along the transport path. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and minimizing the risk of material contamination. The transport process typically involves feeding the water glass material into a hopper or feeder, where it is then introduced into the air stream. The air velocity and pressure are carefully controlled to ensure consistent material flow without causing excessive wear on the system components. Key parameters such as air flow rate, pressure drop, and material feed rate are optimized to achieve stable and efficient transport, ensuring that the water glass material reaches its destination without degradation or loss of quality.
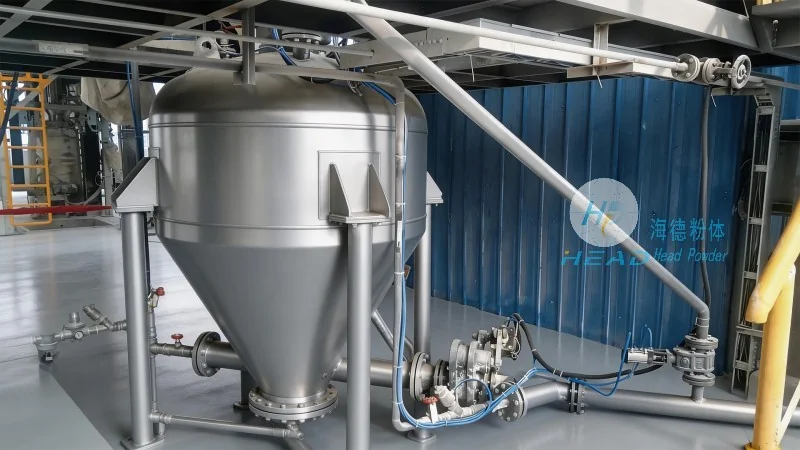
Key Working Scene Characteristics of Air-Driven Transport Systems
The application of air-driven transport for water glass materials is characterized by several distinct features that make it suitable for various industrial environments. First, the system’s ability to handle materials with high moisture content or sticky properties is a significant advantage. Unlike traditional mechanical conveyors, which may suffer from blockages or increased friction due to moisture, air-driven systems rely on airflow to maintain material movement, reducing the risk of clogs and ensuring continuous operation. Second, the flexibility of the system in terms of layout and integration is another critical characteristic. Air-driven transport can be easily adapted to complex plant layouts, with pipes and ducts installed in overhead or underground configurations to accommodate space constraints. This adaptability allows for seamless integration with existing production lines, minimizing downtime during installation and operation. Third, the system’s low maintenance requirements and energy efficiency contribute to its cost-effectiveness. By eliminating moving parts that require regular lubrication or replacement, the air-driven transport system reduces operational costs and enhances overall productivity. Additionally, the use of compressed air as the power source provides a clean and reliable energy input, which is particularly beneficial in environments where electrical safety or explosion-proofing is a concern. The noise level of these systems is also relatively low compared to mechanical conveyors, making them suitable for applications where noise control is essential.
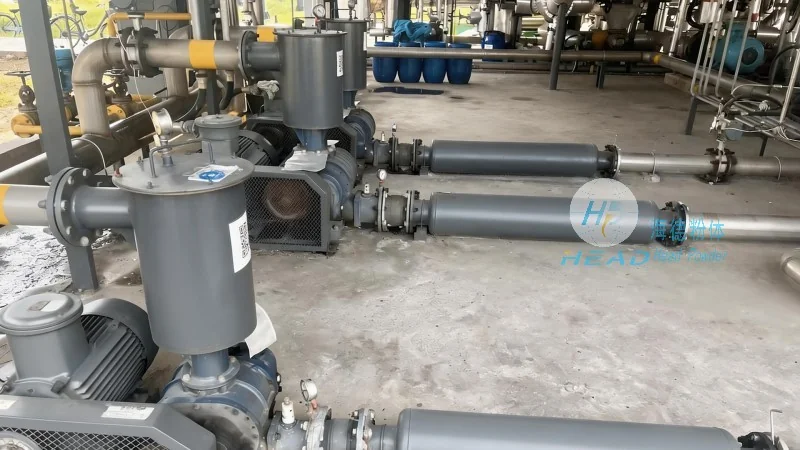
HeadPowder: Your Trusted Partner in Water Glass Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent manufacturer and supplier of advanced material handling equipment, including air-driven transport systems for water glass materials. With a strong commitment to innovation and customer satisfaction, HeadPowder has established itself as a leader in the industry, providing tailored solutions that meet the specific needs of clients across various sectors. The company’s expertise lies in the design, manufacturing, and installation of high-quality air-driven transport systems, which are engineered to deliver superior performance and reliability. HeadPowder’s products are manufactured using premium materials and advanced technologies, ensuring durability and long service life. The company’s technical team provides comprehensive support, including system design, installation, and maintenance services, to ensure that clients achieve optimal performance and minimal downtime. HeadPowder’s commitment to quality and customer service has earned it a reputation for excellence in the market, making it the preferred choice for businesses seeking reliable and efficient material handling solutions. With a focus on continuous improvement and customer-centric approaches, HeadPowder remains dedicated to delivering cutting-edge solutions that enhance operational efficiency and support sustainable industrial practices.