

Principle and Working Scene Characteristics of Copper Sulfate Powder Conveying System Equipment
The copper sulfate powder conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., is a specialized device designed to handle the transportation of copper sulfate powder efficiently and safely. This system is crucial in various industrial applications where the reliable and controlled movement of this chemical is essential. The equipment is engineered to meet the specific demands of industries dealing with copper sulfate, ensuring optimal performance and operational safety.
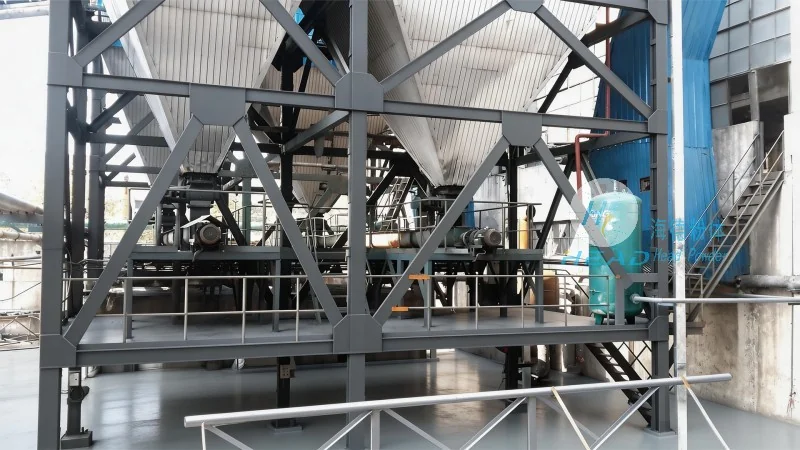
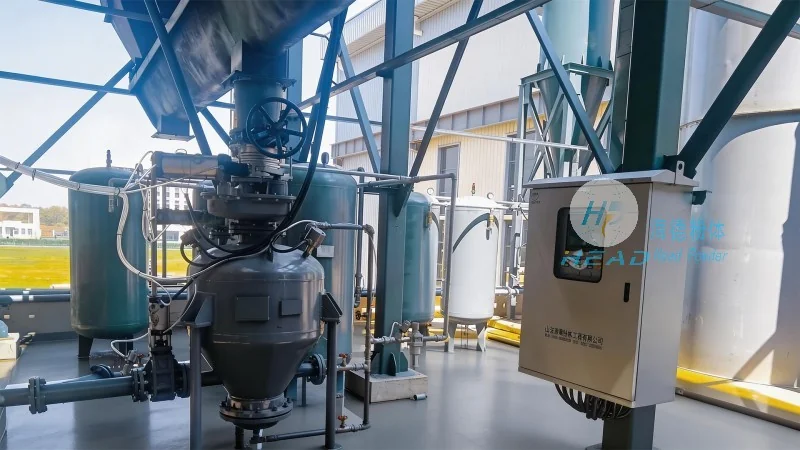
Principle of Operation for the Powder Conveying System
The core principle of the copper sulfate powder conveying system lies in its ability to transport dry powders like copper sulfate through a sealed pipeline system. The system typically employs a combination of positive displacement pumps, air-operated diaphragm pumps, or screw conveyors, depending on the specific requirements of the application. The sealed design prevents dust contamination and environmental exposure, which is critical for maintaining product quality and adhering to safety regulations. The equipment ensures that the copper sulfate powder is moved without degradation, maintaining its chemical properties throughout the conveying process. The system's control mechanisms allow for precise flow rate adjustment, enabling operators to manage the material transport according to production needs. This precision is vital in industries where the consistency of the copper sulfate powder is paramount, such as in chemical manufacturing, agriculture, and water treatment applications.
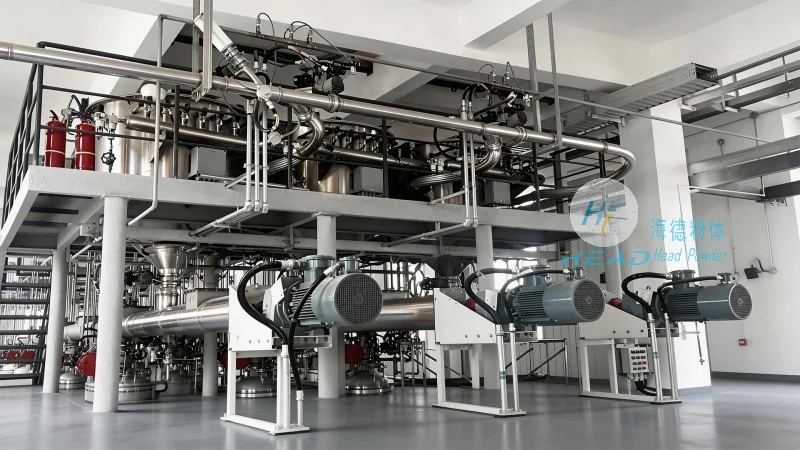
Working Scene Characteristics and Application Scenarios
The copper sulfate powder conveying system is widely used in diverse industrial settings, each with unique characteristics that the equipment addresses effectively. In chemical manufacturing plants, the system is employed to transport copper sulfate from storage silos to processing units, ensuring a continuous and uninterrupted supply of raw material. The sealed conveying process minimizes the risk of dust inhalation by workers and prevents contamination of the powder with external particles, which is essential for maintaining the purity of the chemical. In agricultural settings, the equipment is used to deliver copper sulfate as a fungicide or nutrient supplement, where the ability to handle the powder in a controlled manner is crucial for accurate dosage and application. The system's design allows for easy integration into existing agricultural machinery and storage facilities, making it a practical solution for farmers and agricultural cooperatives. Additionally, in water treatment facilities, the copper sulfate powder conveying system plays a key role in delivering the chemical for algae control and water purification processes. The system's ability to handle the powder in a hygienic and controlled manner ensures that the water treatment process is efficient and effective, meeting regulatory standards for water quality. The working scene characteristics of the system, such as its adaptability to different powder properties and its ability to operate in various environmental conditions, make it a versatile solution for a wide range of industrial applications.
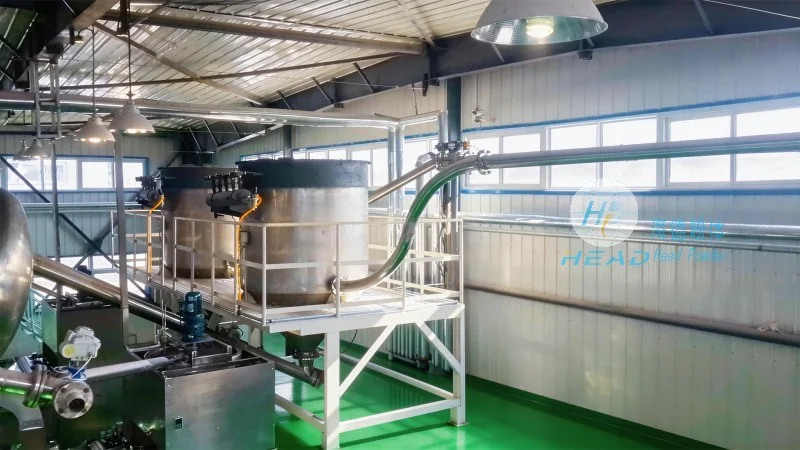
Key Features and Advantages of the Conveying System
Shandong HeadPowder Engineering Co., Ltd. has incorporated several key features into the copper sulfate powder conveying system to enhance its performance and usability. The system is equipped with advanced control systems that allow for real-time monitoring of the conveying process, providing operators with immediate feedback on flow rates, pressure, and other critical parameters. This enables quick adjustments to maintain optimal operation and prevent system failures. The equipment is also designed with durable materials that are resistant to corrosion and wear, ensuring long-term reliability and minimal maintenance costs. The sealed design of the system prevents dust leakage and environmental pollution, which is in line with environmental regulations and promotes a safe working environment. The system's compact design makes it suitable for installation in limited spaces, which is beneficial for facilities with space constraints. Furthermore, the system is easy to maintain, with accessible components that can be serviced without extensive downtime. These features collectively contribute to the overall efficiency and effectiveness of the copper sulfate powder conveying system, making it a preferred choice for industries dealing with this chemical.