

Principle and Working Scene Characteristics of Stone Aggregate Powder Conveying System
Stone aggregate powder conveying systems are specialized equipment designed to transport bulk materials such as stone aggregates, powders, and granular substances efficiently and reliably. These systems are crucial in various industrial applications, including construction, mining, and material processing, where the need to move large volumes of raw materials or finished products is essential. The core principle of these systems involves the use of mechanical or pneumatic methods to move material from one location to another, ensuring minimal loss, contamination, and energy consumption.
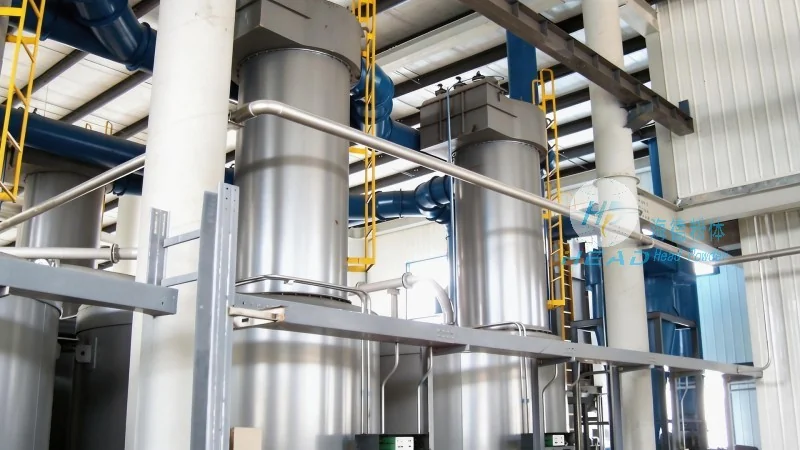
Key Components and Working Principle
The operation of a stone aggregate powder conveying system typically relies on a combination of components that work in tandem to achieve effective material transport. The main components include a hopper or feeding device to collect the material, a conveyor mechanism (either screw, belt, or pneumatic), and a control system to regulate the flow. The system's working principle is based on the conversion of energy—whether mechanical, pneumatic, or gravitational—into motion to move the material through the system. For instance, in pneumatic conveying systems, compressed air is used to create a pressure differential that propels the material through pipes. In mechanical systems, rotating screws or belts push the material forward. The design of these components is critical to ensure the system operates efficiently, with minimal maintenance and maximum throughput.
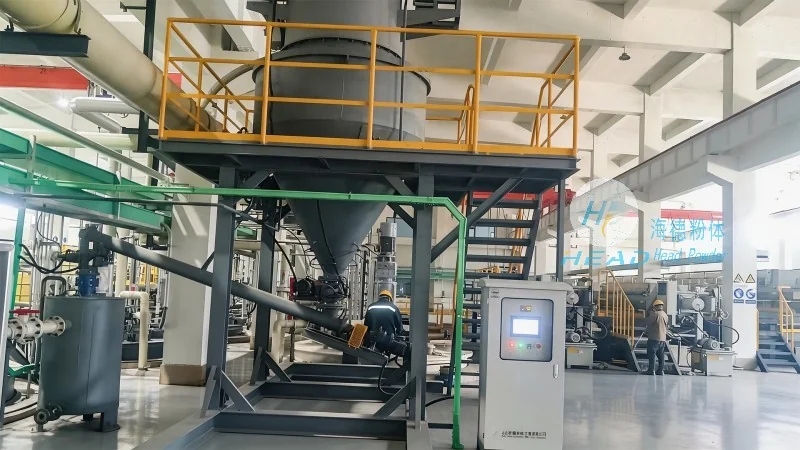
Working Scene Characteristics and Applications
The working scene characteristics of stone aggregate powder conveying systems are tailored to meet the specific demands of different industrial environments. These systems are commonly used in construction sites where stone aggregates are transported from storage to mixing plants or on-site storage areas. In mining operations, they help move crushed stone or ore from processing facilities to storage or transport vehicles. Additionally, in material processing industries, such as cement or chemical production, these systems are essential for transporting raw materials to production lines. The key characteristics of these working scenes include high-volume material handling, the need for dust control (as many stone aggregates are powdery), and the requirement for systems that can operate in harsh, outdoor environments. The systems are designed to be robust and durable, with features like weather-resistant enclosures and corrosion-resistant materials to withstand the challenges of industrial settings.
Advantages and Performance Metrics
Stone aggregate powder conveying systems offer several advantages that make them a preferred choice in many industries. One of the primary benefits is their ability to handle large volumes of material with high efficiency, reducing labor costs and increasing production throughput. The systems are also designed to minimize material loss and contamination, which is critical in applications where the quality of the material is paramount. Additionally, modern systems incorporate advanced control technologies that allow for precise regulation of material flow, ensuring consistent performance and reducing waste. Performance metrics such as throughput capacity, energy consumption per ton of material, and system downtime are key indicators of the system's efficiency. Companies like Shandong HeadPowder Engineering Co., Ltd. specialize in designing and manufacturing these systems, providing customized solutions that meet the specific needs of their clients.
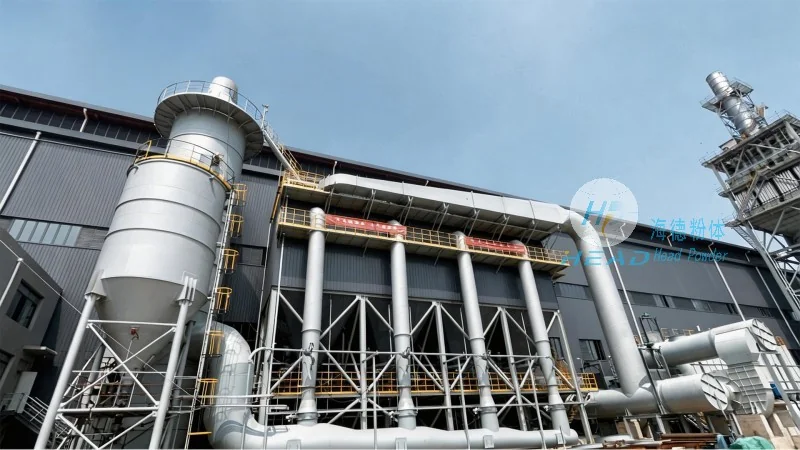
Customization and Maintenance Considerations
Due to the diverse nature of industrial applications, stone aggregate powder conveying systems are often customized to fit specific requirements. Factors such as the type of material (e.g., fine powders vs. coarse aggregates), the distance to be covered, and the operating environment influence the system's design. For example, a system transporting fine powders may require a more enclosed, dust-tight design to prevent air pollution, while a system handling coarse aggregates might use a larger hopper and a robust screw conveyor. Maintenance is another critical aspect of these systems. Regular inspections, cleaning of components, and replacement of worn parts are essential to ensure long-term operation. The systems are designed with easy access to components, facilitating maintenance and reducing downtime. Shandong HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, offers comprehensive support, including maintenance services and spare parts, to ensure their systems operate at optimal performance.