

Principle and Working Scene Characteristics of Bentonite Pneumatic Conveying System Equipment
HeadPowder, a leading enterprise in the field of material handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. This article focuses on the principles and working scene characteristics of the Bentonite Pneumatic Conveying System Equipment, highlighting its technical features and practical applications.
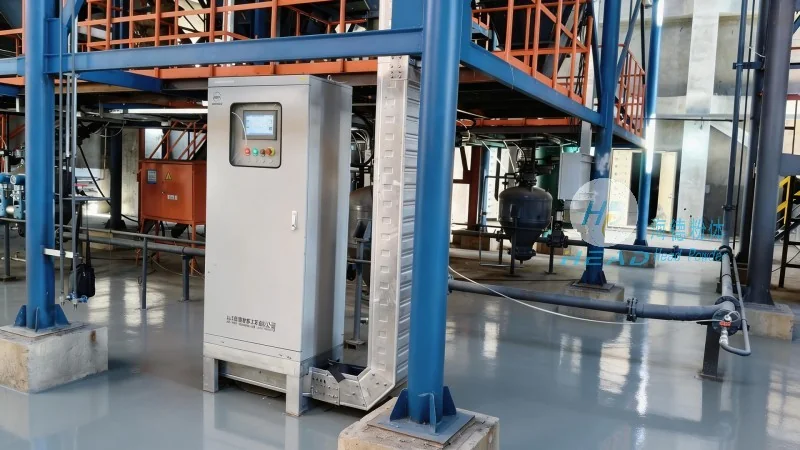
Introduction to Bentonite Pneumatic Conveying Systems
Bentonite, a natural clay mineral with excellent swelling and water retention properties, is widely used in various industrial sectors such as construction, oil drilling, and environmental remediation. The Bentonite Pneumatic Conveying System is engineered to efficiently transport this material from storage to processing or application sites. This system combines the advantages of pneumatic conveying technology with specialized equipment designed to handle the unique physical and chemical properties of bentonite, ensuring reliable and low-maintenance operation.
The Working Principle of the Equipment
The core of the Bentonite Pneumatic Conveying System lies in its air-driven mechanism. The system typically consists of a blower, a hopper for material storage, a conveying line, and a discharge unit. The process begins when bentonite is fed into the hopper. The blower then generates a high-pressure air stream that draws the material into the conveying line. As the air and material travel through the pipeline, the system maintains a consistent flow rate, preventing blockages and ensuring smooth transport. The discharge unit at the destination point separates the material from the air, allowing for precise delivery to the target location.
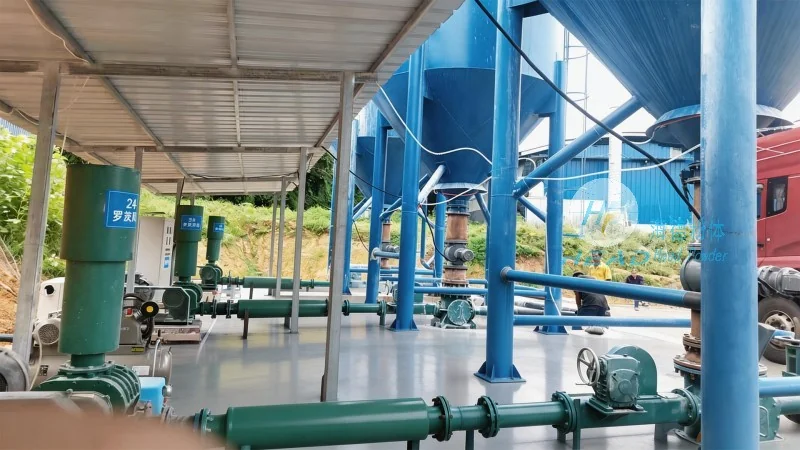
Key Working Scene Characteristics
The Bentonite Pneumatic Conveying System is particularly suited for industrial environments where traditional bulk material handling methods may be impractical or inefficient. Its key characteristics include high efficiency in material transport, minimal space requirements compared to traditional methods like trucks or conveyor belts, and reduced labor costs due to automated operation. The system is also designed for durability, with components resistant to the abrasive nature of bentonite, ensuring long-term reliability. Additionally, the system can be customized to accommodate varying production volumes and operational requirements, making it adaptable to different working scenarios.
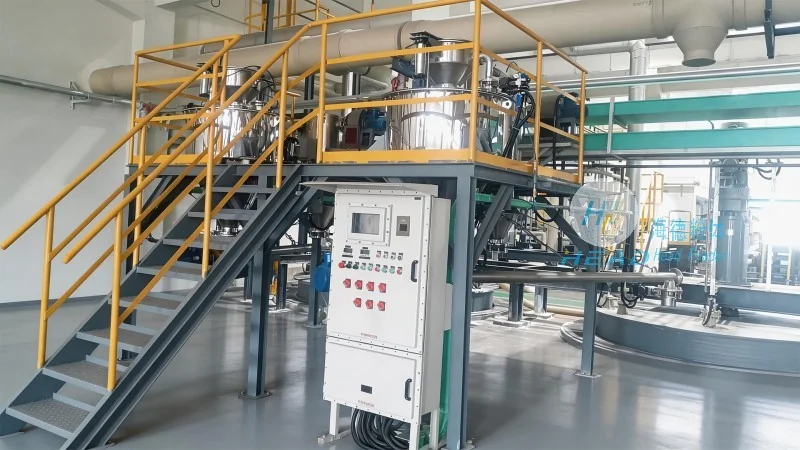
Applications and Operational Benefits
HeadPowder's Bentonite Pneumatic Conveying System is deployed in diverse working scenes, including construction sites for mixing concrete and soil stabilization, oil fields for drilling fluid preparation, and environmental projects for soil remediation. The system's ability to handle large volumes of bentonite with minimal human intervention enhances operational efficiency and safety. Furthermore, the system's low energy consumption and reduced environmental impact compared to traditional transport methods align with modern industrial sustainability goals.
Conclusion and Company Overview
Shandong HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, has established itself as a trusted provider of specialized material handling solutions. The company's expertise in designing and implementing Bentonite Pneumatic Conveying Systems reflects its commitment to delivering high-quality, reliable equipment tailored to the needs of its clients. By leveraging advanced technology and rigorous quality control, HeadPowder ensures that its systems meet the highest industry standards, providing long-term value and operational excellence to businesses across various sectors.