

Principles and Application Scenarios of Magnesium Oxide Powder Pneumatic Conveying
For industrial operations involving the handling of magnesium oxide powder, efficient and reliable material transport is crucial. Pneumatic conveying systems offer a solution that combines precision, control, and safety for transporting fine powders like magnesium oxide. This article explores the fundamental principles behind magnesium oxide powder pneumatic conveying and highlights key application scenarios where such systems excel.
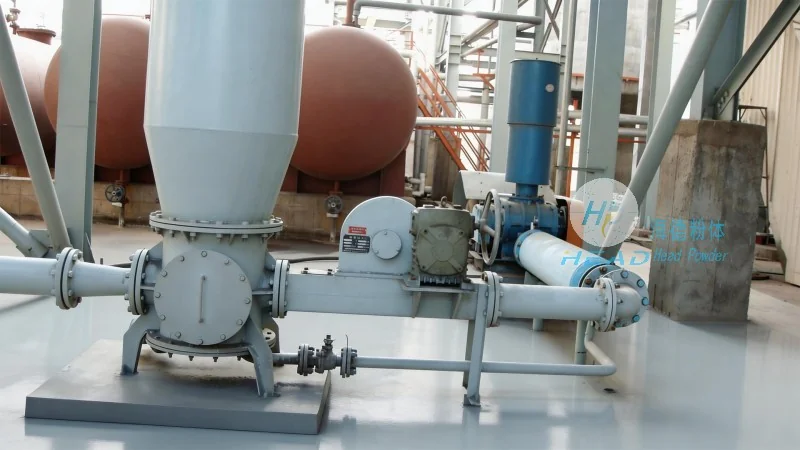
Understanding Pneumatic Conveying Principles
Pneumatic conveying relies on the use of air or gas to transport solid particles through a pipeline. In the case of magnesium oxide powder, the system typically involves a combination of positive and negative pressure or a vacuum to move the material from a source to a destination. The core components of a pneumatic conveying system include a feeder, a conveying line, a receiver, and often a filter or dust collector to ensure environmental compliance and material integrity. The principle of operation involves creating a flow of air that carries the powder particles, with the velocity and pressure maintained to prevent particle separation or degradation.
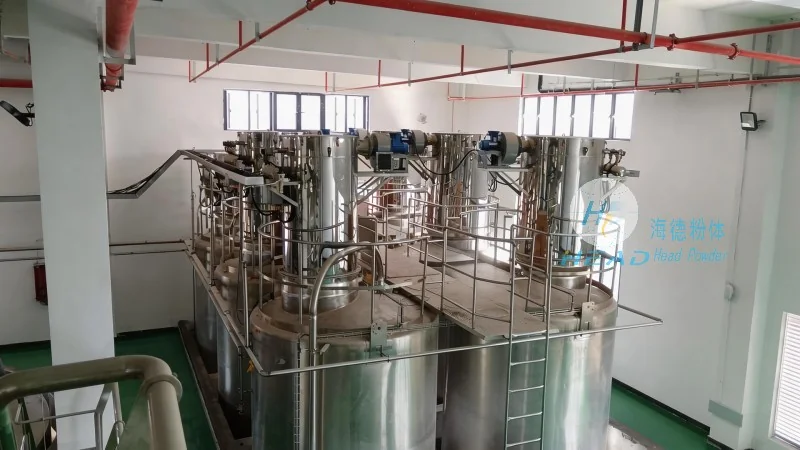
Key Components and Their Function in Magnesium Oxide Powder Conveying
The effectiveness of a magnesium oxide powder pneumatic conveying system depends on several critical components. The feeder is responsible for introducing the powder into the conveying line at a consistent rate, ensuring a smooth flow without blockages. The conveying line, usually made of materials resistant to corrosion and abrasion, transports the powder and air mixture. The receiver collects the conveyed material and may include a hopper or storage vessel. A filter or dust collection system is essential to capture any fine particles that escape the conveying line, protecting the environment and maintaining material purity. Each component must be designed to handle the specific characteristics of magnesium oxide powder, such as its fine particle size and potential reactivity.
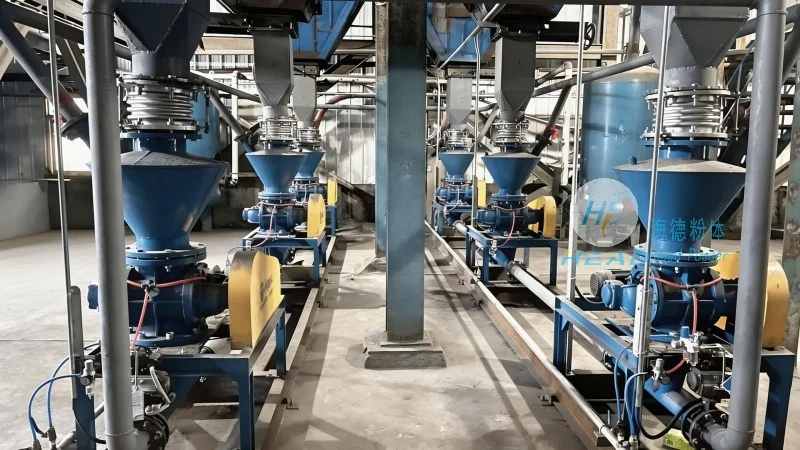
Application Scenarios for Magnesium Oxide Powder Pneumatic Conveying
Magnesium oxide powder pneumatic conveying is widely used in various industrial sectors due to its ability to handle fine powders efficiently. One common application is in the production of refractory materials, where magnesium oxide is a key ingredient. The system allows for precise dosing and transport of the powder to mixing and processing equipment, ensuring consistent product quality. Another application is in the chemical industry, where magnesium oxide is used as a filler or catalyst. Pneumatic conveying enables safe and controlled transport of the powder between processing stages, minimizing exposure risks and maintaining material integrity. Additionally, in the pharmaceutical and food industries, where purity is paramount, pneumatic conveying systems provide a hygienic and dust-free method for transporting magnesium oxide powder, adhering to strict regulatory standards.
Advantages of Using Pneumatic Conveying for Magnesium Oxide Powder
Compared to traditional methods like belt conveyors or bucket elevators, pneumatic conveying offers several advantages for magnesium oxide powder handling. One significant benefit is the ability to transport materials in a closed system, which reduces dust emissions and improves workplace safety. This is particularly important for magnesium oxide, which can be a respiratory irritant if inhaled. Another advantage is the flexibility of the system, as it can handle varying flow rates and distances without significant changes to the infrastructure. Pneumatic conveying also minimizes material degradation, as the powder is not subjected to high impact or abrasion during transport. Furthermore, the system can be integrated with other processing equipment, such as mixers or reactors, allowing for seamless material transfer and improved overall process efficiency.
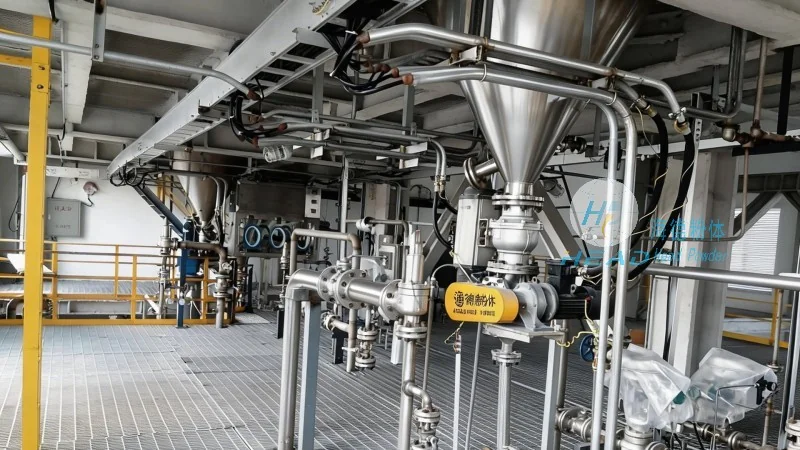
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading provider of industrial material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of various industries. With a focus on innovation and customer satisfaction, HeadPowder offers customized solutions for handling fine powders like magnesium oxide. The company's expertise lies in understanding the unique properties of different powders and designing systems that ensure efficient, safe, and reliable transport. HeadPowder's commitment to quality and service has made it a trusted partner for businesses seeking to optimize their material handling processes.