

[WOKING PRINCIPLE AND FEATURES OF BICARBONATE OF SODA MATERIAL PNEUMATIC CONVEYING SYSTEMS]
For industrial applications involving the transport of bicarbonate of soda, a specialized pneumatic conveying system is often employed to ensure efficient and safe material handling. This article explores the working principle and key features of such systems, highlighting how they enhance operational efficiency in material processing.
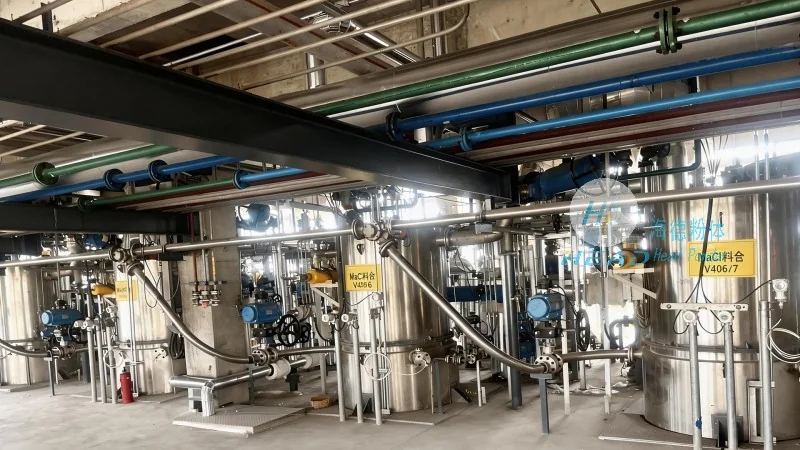
About the Company: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced material handling solutions. With a strong presence in China, particularly in Shandong province, the company specializes in designing, manufacturing, and installing pneumatic conveying systems tailored to the unique needs of various industries. HeadPowder's commitment to quality and innovation has established it as a trusted partner for businesses seeking reliable and efficient material transport solutions.
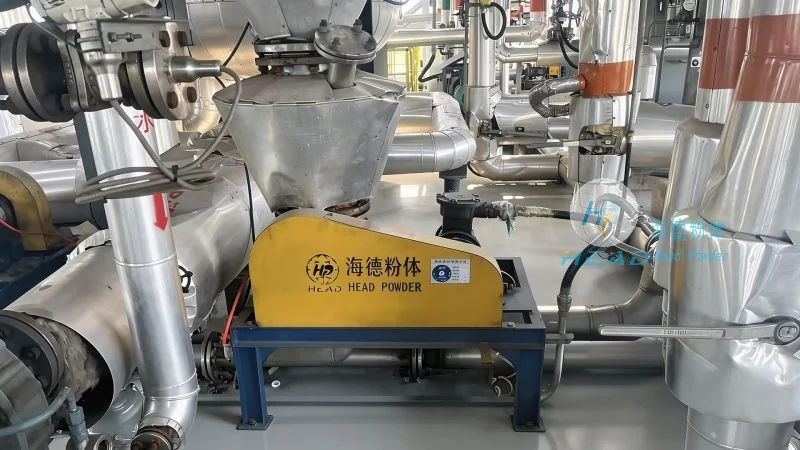
Working Principle of Bicarbonate of Soda Pneumatic Conveying Systems
The core of a bicarbonate of soda pneumatic conveying system lies in its ability to transport dry powder materials using air as the conveying medium. The system typically operates on the principle of air pressure or vacuum, where compressed air or a vacuum is used to create a flow that moves the powder from the source to the destination. The process begins with the material being fed into a hopper or feeder, where it is then mixed with the air stream. As the air and powder mixture travels through the pipeline, the air provides the necessary force to propel the material forward, ensuring consistent and controlled transport. The system may include components such as a blower, cyclone separator, and filter to manage the air flow and separate the powder from the air at the end of the line. This mechanism allows for a continuous and automated process, reducing manual labor and minimizing the risk of material spillage or contamination.
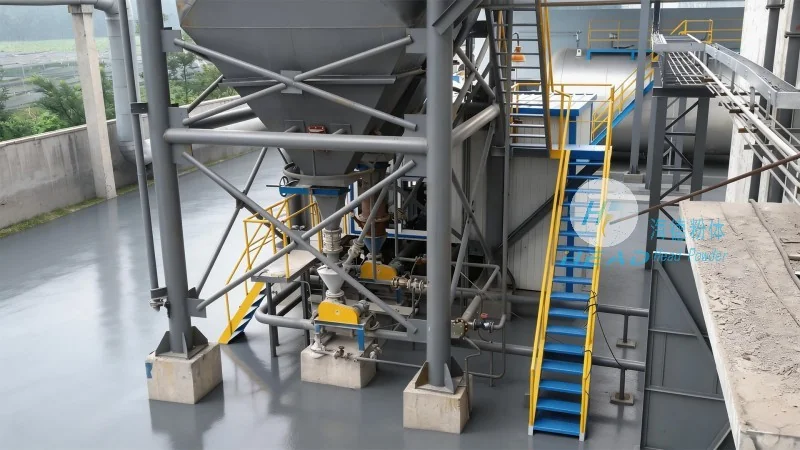
Key Features of Bicarbonate of Soda Pneumatic Conveying Systems
Several distinct features make bicarbonate of soda pneumatic conveying systems an ideal choice for industrial applications. Firstly, these systems offer high efficiency in material transport, capable of moving large volumes of powder over considerable distances with minimal energy consumption. The use of air as the conveying medium eliminates the need for mechanical components like belts or chains, reducing maintenance requirements and extending the lifespan of the equipment. Secondly, the systems are designed to minimize material loss and degradation, which is crucial for sensitive materials like bicarbonate of soda. The gentle handling of the powder through the air stream prevents clumping or breakage, ensuring that the material retains its quality and properties throughout the transport process. Thirdly, the systems are highly adaptable and can be customized to suit specific operational requirements. This includes the ability to adjust the air pressure, flow rate, and pipeline configuration to optimize performance for different production scales. Additionally, the systems are often equipped with advanced control systems that allow for real-time monitoring and adjustment, enhancing operational flexibility and reliability. Finally, the environmental benefits of pneumatic conveying systems are significant, as they reduce the need for manual handling and minimize dust emissions, contributing to a safer and more sustainable workplace.
Conclusion
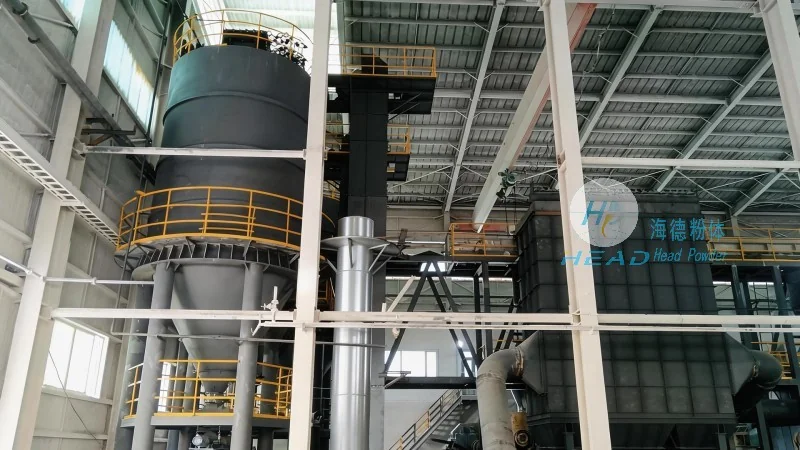
In summary, the working principle and features of bicarbonate of soda pneumatic conveying systems, as exemplified by solutions from Shandong HeadPowder Engineering Co., Ltd., provide a robust and efficient method for material transport. By leveraging air as the primary conveying medium, these systems offer advantages such as high efficiency, low maintenance, and environmental sustainability. For industries dealing with bicarbonate of soda, investing in a well-designed pneumatic conveying system can significantly improve operational productivity and material handling capabilities. HeadPowder's expertise in engineering and manufacturing ensures that clients receive tailored solutions that meet their specific needs, supporting their long-term success in the market.