

Working Principle and Features of Red Mud Powder Pneumatic Conveying System
Red mud, a byproduct of the bauxite refining process used to extract aluminum, poses significant challenges in handling and disposal due to its fine particle size and high moisture content. Traditional methods for transporting red mud powder, such as belt conveyors or trucks, often suffer from issues like dust pollution, material blockage, and operational inefficiencies. To address these challenges, the red mud powder pneumatic conveying system has emerged as a sophisticated solution that leverages air to transport the material efficiently and safely. This article explores the working principle and key features of such a system, highlighting its advantages in industrial applications.
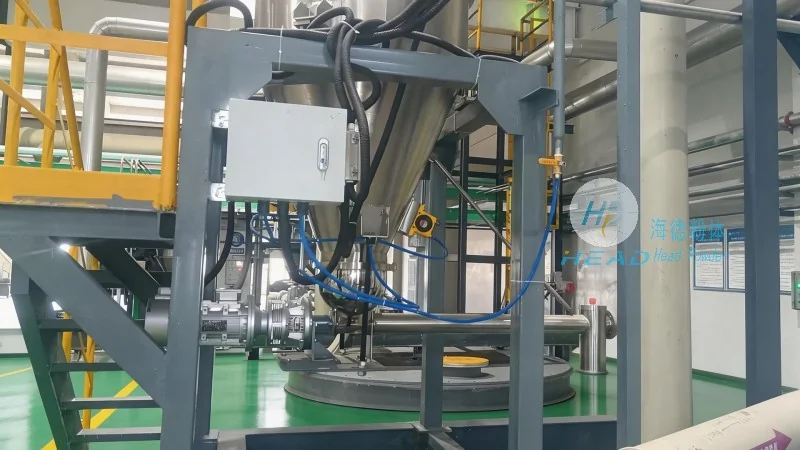
Understanding the Working Principle of Red Mud Powder Pneumatic Conveying System
The core of a red mud powder pneumatic conveying system is the pneumatic transport mechanism, which operates on the principle of using compressed air to move particulate materials through a pipeline. The system typically consists of a series of components, including a material feeder, a compressor, a pipeline network, and a discharge unit. The process begins with the red mud powder being fed into the system, where it is mixed with a controlled amount of air. The air, under pressure, creates a flow that propels the powder particles through the pipeline. The velocity of the air is critical; it must be sufficient to overcome the gravitational and frictional forces acting on the particles while maintaining a stable flow to prevent particle separation or blockage. The system may use either positive pressure (where air is blown into the pipeline) or negative pressure (where air is drawn out), depending on the specific application and the distance the material needs to be transported. For red mud, which is often fine and cohesive, positive pressure systems are commonly preferred as they provide better control over the material flow and reduce the risk of clogging.
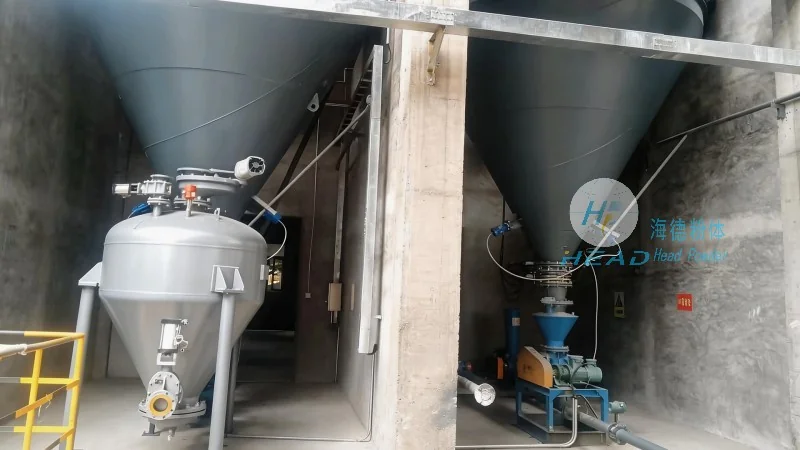
Key Features of Red Mud Powder Pneumatic Conveying System
The red mud powder pneumatic conveying system offers several distinct advantages that make it an ideal choice for industrial handling of this challenging material. First, it provides a dust-free and enclosed transport environment, which significantly reduces environmental pollution and improves workplace safety. Unlike open conveyors, the system confines the material within a sealed pipeline, preventing dust emissions that can affect air quality and pose health risks to workers. Second, the system is highly efficient in terms of energy consumption and operational speed. By using compressed air to transport the material, the system can move large volumes of red mud over long distances with minimal labor and maintenance requirements. This efficiency is particularly valuable in large-scale industrial operations where continuous material handling is required. Third, the system is highly adaptable to varying conditions. It can handle different particle sizes and moisture contents of red mud, making it suitable for diverse applications, from processing plants to disposal sites. The flexibility of the system also allows for easy integration with other industrial processes, such as storage and treatment facilities. Fourth, the system offers improved material handling safety. By eliminating the need for manual handling or open transport methods, it reduces the risk of accidents and injuries associated with handling fine powders. The enclosed design also protects the material from contamination and degradation, ensuring that the red mud remains in its original state until it reaches its destination.
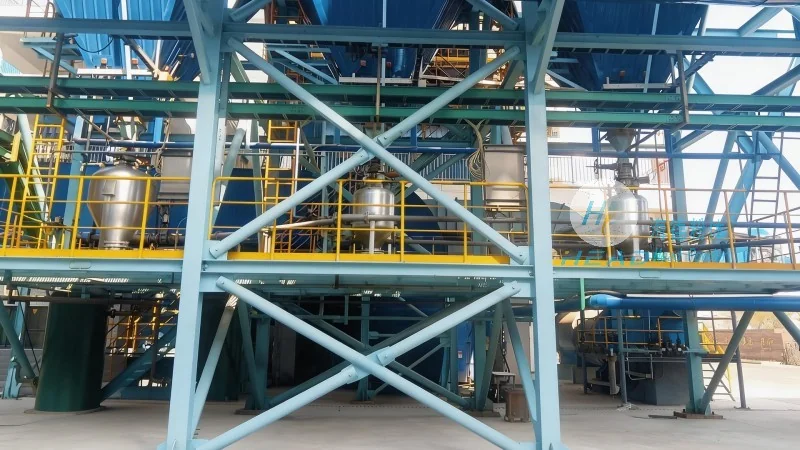
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, as the name suggests, specializes in engineering solutions for powder handling and material transport. With a focus on innovative and efficient systems, the company has developed the red mud powder pneumatic conveying system as a key product to address the challenges faced by industries dealing with red mud. HeadPowder's expertise lies in designing and manufacturing systems that are tailored to the specific needs of clients, ensuring optimal performance and reliability. The company's commitment to quality and customer satisfaction has made it a trusted partner in the industry, providing solutions that enhance operational efficiency and environmental compliance. HeadPowder's systems are built with durable materials and advanced technology, ensuring long-term performance and minimal maintenance costs. The company's headquarters is located in Shandong, China, where it continues to innovate and expand its product offerings to meet the evolving needs of the market.