

Working Principle and Features of the Intelligent Tonne Bag Filling Station for Powder Pneumatic Con
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced powder handling systems. The intelligent tonne bag filling station with pneumatic conveying is a sophisticated solution tailored for efficient bulk powder transfer from large tonne bags to processing equipment. This system integrates cutting-edge technology to enhance operational efficiency, safety, and reliability in industrial powder handling applications.
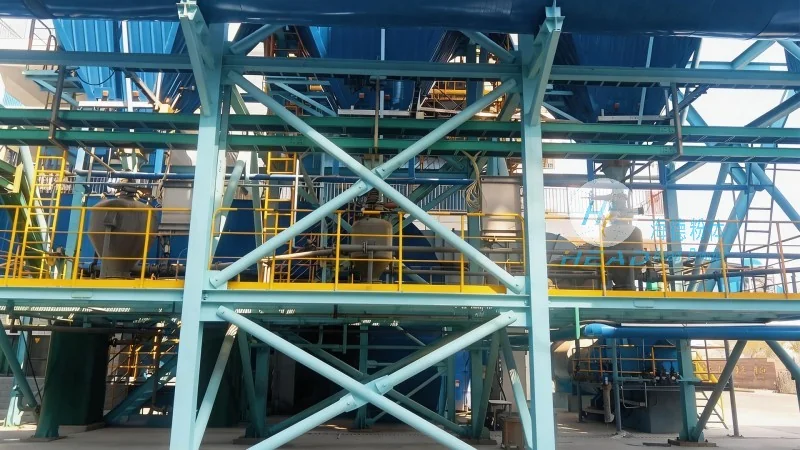
Overview of the Intelligent Tonne Bag Filling Station
The intelligent tonne bag filling station is engineered to automate the process of transferring bulk powders from tonne bags into processing lines. It combines the functionality of a tonne bag discharging system with a pneumatic conveying network, ensuring seamless and controlled material flow. This system is particularly suitable for industries such as food, pharmaceuticals, chemicals, and minerals, where precision and hygiene are critical.
Working Principle of the Pneumatic Conveying System
The core of the system is the pneumatic conveying mechanism, which utilizes air pressure to transport powders. The process begins with the opening of a tonne bag, typically via a valve or a mechanical opening device. The powder is then discharged into a hopper or a collection chamber. From there, a blower or a compressor generates a flow of air that carries the powder particles through a pipeline network. The system may employ different conveying modes, such as positive pressure or negative pressure, depending on the material characteristics and the distance to be covered. The air-powder mixture travels through the pipeline, and the powder is deposited at the destination point, while the air is either filtered and recirculated or vented to the atmosphere. The intelligent control system monitors the pressure, flow rate, and material level, ensuring optimal performance and preventing blockages or overloading.
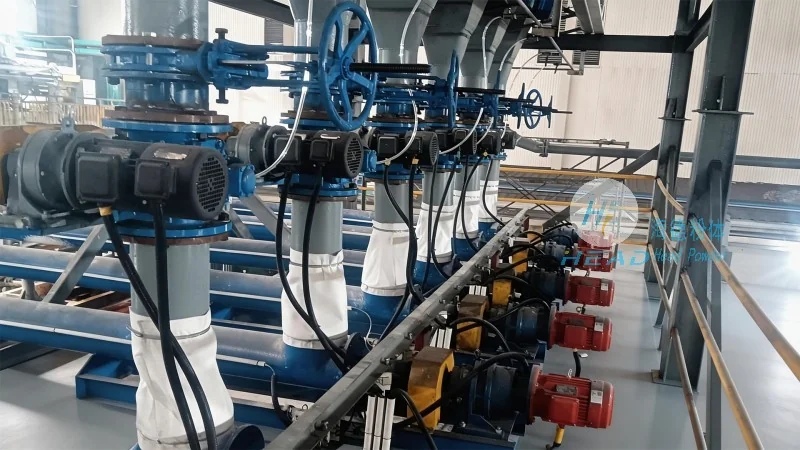
Key Features of the Intelligent Tonne Bag Filling Station
1. Automated Tonne Bag Handling: The system automates the entire process from bag opening to material discharge, reducing manual labor and minimizing the risk of contamination. It can handle multiple tonne bags simultaneously, increasing throughput and operational efficiency.
2. Pneumatic Conveying Flexibility: The pneumatic conveying system offers flexibility in material transport, allowing for horizontal, vertical, or mixed-direction conveying. It can handle a wide range of powder types, including fine powders, granules, and bulk materials, with minimal product degradation.
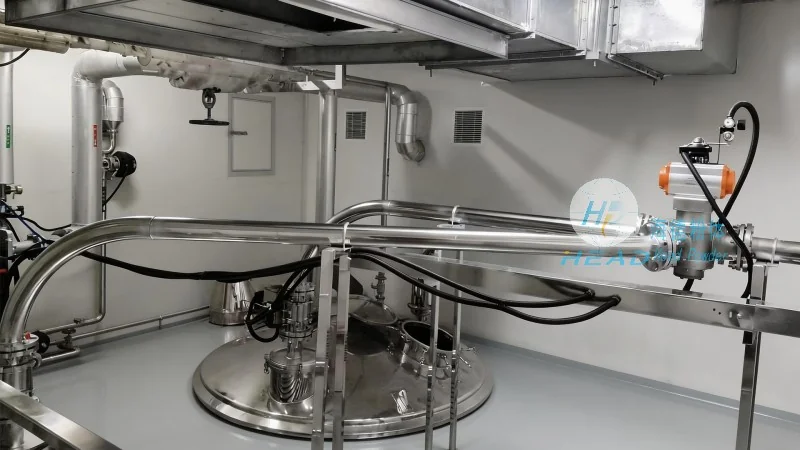
3. Intelligent Control and Monitoring: Advanced control systems provide real-time monitoring of key parameters, such as pressure, flow rate, and material level. This enables proactive maintenance, reduces downtime, and ensures consistent product quality. The system can also be integrated with other process equipment for a fully automated production line.
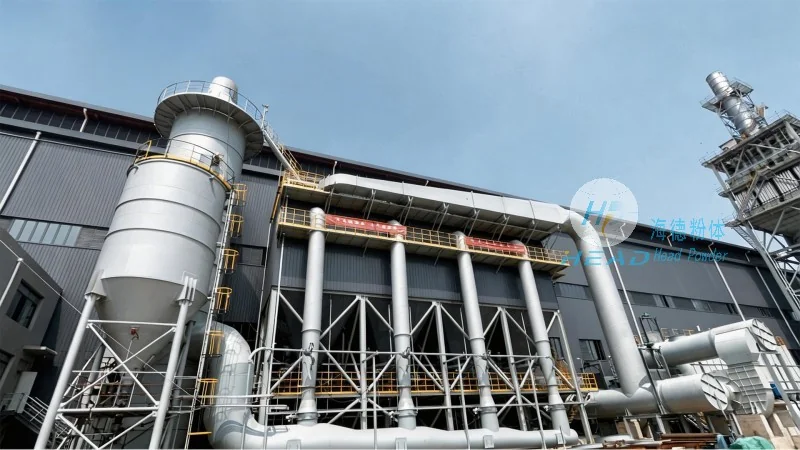
4. Enhanced Safety and Hygiene: The design incorporates safety features like explosion-proof components, dust collection systems, and sealed conveying lines to prevent dust emissions and ensure a safe working environment. The system is also easy to clean and maintain, meeting stringent hygiene standards required in food and pharmaceutical industries.
5. Customizable and Scalable: HeadPowder offers customized solutions tailored to specific customer requirements, including different bag sizes, conveying distances, and material types. The system can be scaled to accommodate varying production volumes, from small-scale operations to large industrial facilities.