

Working Principle and Features of Tonne Bag Unloading Station Material Conveying Lines
HeadPowder, a renowned enterprise based in Shandong, China, specializes in the design and manufacturing of advanced material handling systems. This article delves into the working principle and key features of the tonne bag unloading station material conveying line, a critical solution for efficient bulk material processing in various industrial applications.
About HeadPowder: Leading Provider of Material Handling Solutions
HeadPowder Engineering Co., Ltd. is a professional manufacturer and supplier of material handling equipment. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in the industry. Headquartered in Shandong, China, HeadPowder leverages decades of experience to deliver customized solutions tailored to the specific needs of clients across diverse sectors, including chemical, food, and pharmaceutical industries.
Working Principle of Tonne Bag Unloading Station Material Conveying Lines
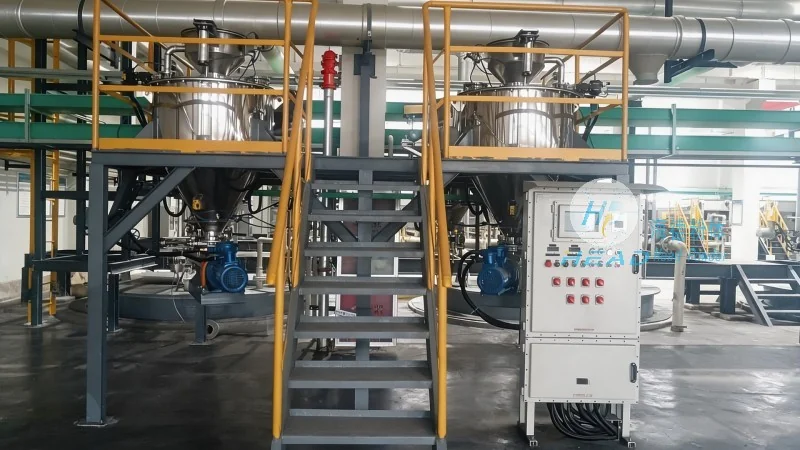
The tonne bag unloading station material conveying line is engineered to streamline the entire process of handling bulk materials from the unloading of tonne bags to their subsequent transport and processing. The system typically operates through a series of integrated components, each playing a crucial role in ensuring smooth and efficient material flow. The process begins with the arrival of tonne bags at the unloading station, where they are positioned for opening. A specialized opening mechanism, such as a hydraulic or mechanical cutter, is used to break the bag open, allowing the contents to be released into a hopper or collection bin. This step is critical for preventing material spillage and ensuring a clean transfer.
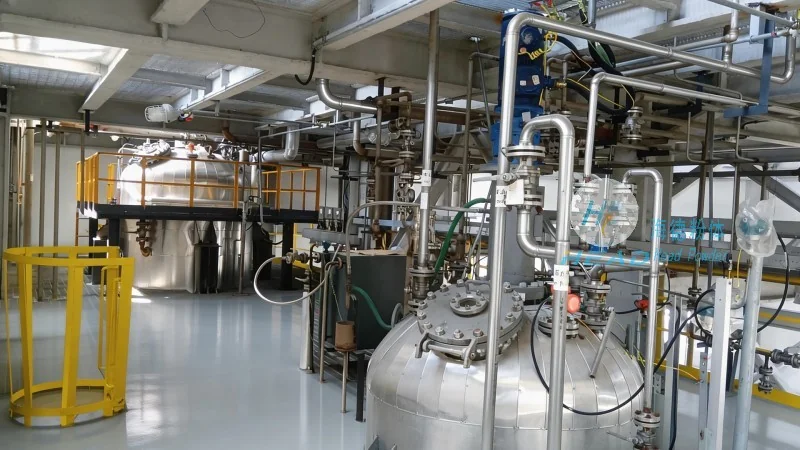
Once the material is in the hopper, it is transferred to a conveyor system. The conveying line may consist of various types of conveyors, including belt conveyors, screw conveyors, or pneumatic conveying systems, depending on the material characteristics and processing requirements. The conveyor components are designed to handle the bulk density and flow characteristics of the material, ensuring consistent and reliable transport. The system may also include a feeding mechanism that regulates the flow rate, preventing overloading or underloading of downstream equipment. In some configurations, a weighing or batching unit is integrated to provide precise measurement of the material being conveyed, enabling accurate dosing for production processes.
Key Features and Advantages of the System
The tonne bag unloading station material conveying line offered by HeadPowder is characterized by several key features that enhance its performance and usability. One of the primary advantages is its high efficiency, which significantly reduces the time required for material handling operations. The system is designed to handle large volumes of material with minimal downtime, thereby increasing overall productivity. Additionally, the equipment is built with durability and reliability in mind, featuring robust construction and high-quality components that can withstand harsh industrial environments and heavy usage.
Another notable feature is the system's adaptability. HeadPowder's engineers can customize the conveying line to accommodate various types of tonne bags and material properties, ensuring compatibility with different production processes. The modular design allows for easy integration with existing infrastructure, minimizing installation time and costs. Furthermore, the system incorporates advanced control systems that enable precise monitoring and adjustment of the conveying parameters, such as speed and flow rate, ensuring optimal performance under varying conditions.
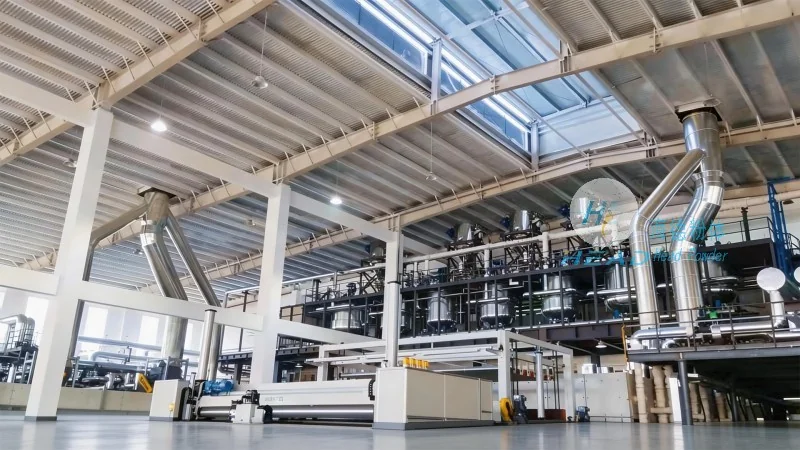
The safety features integrated into the system are also a significant advantage. The design includes safety guards and emergency stop mechanisms to protect operators and prevent accidents during operation. The use of automated controls reduces the need for manual intervention, minimizing the risk of human error and enhancing workplace safety. Additionally, the system may include dust suppression and filtration components to maintain a clean and safe working environment, which is particularly important in industries where material dust is a concern.
Conclusion: Enhancing Material Handling Efficiency with HeadPowder's Solutions
In conclusion, the tonne bag unloading station material conveying line from HeadPowder Engineering Co., Ltd. represents a sophisticated and efficient solution for bulk material handling. By combining advanced engineering with robust construction, the system ensures reliable operation and high performance in demanding industrial settings. HeadPowder's commitment to quality and customization makes this equipment an ideal choice for businesses seeking to optimize their material handling processes and improve overall operational efficiency. With its headquarters in Shandong, China, HeadPowder continues to provide innovative solutions that meet the evolving needs of the industry, supporting clients in achieving their production goals with precision and reliability.