

Working Principle and Features of Metering Bin Pump Material Conveying Lines
Understanding the operational mechanics and key attributes of metering bin pump material conveying lines is crucial for industries that rely on efficient bulk material handling. This article delves into the core functions, technical design, and practical advantages of such systems, providing a comprehensive overview for professionals seeking to optimize their material transport processes.
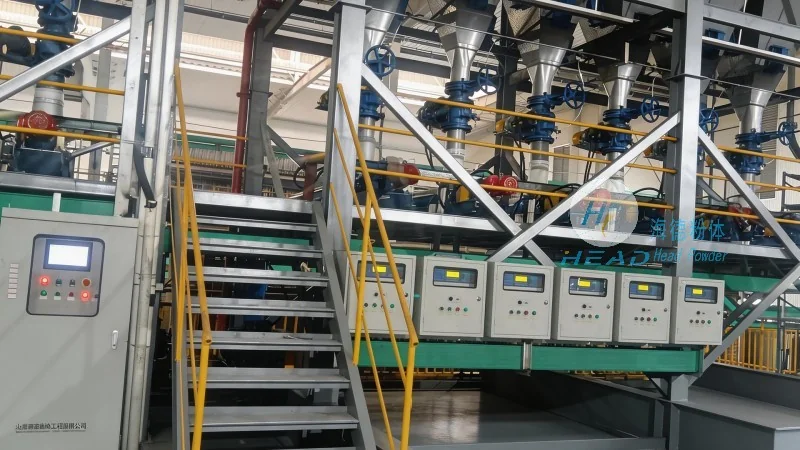
HeadPowder, a leading manufacturer based in Shandong, China, specializes in developing advanced material handling solutions. With a focus on precision and reliability, their metering bin pump systems are engineered to meet the demanding requirements of various industrial applications, including mining, construction, and chemical processing.
Working Principle of Metering Bin Pump Material Conveying Lines
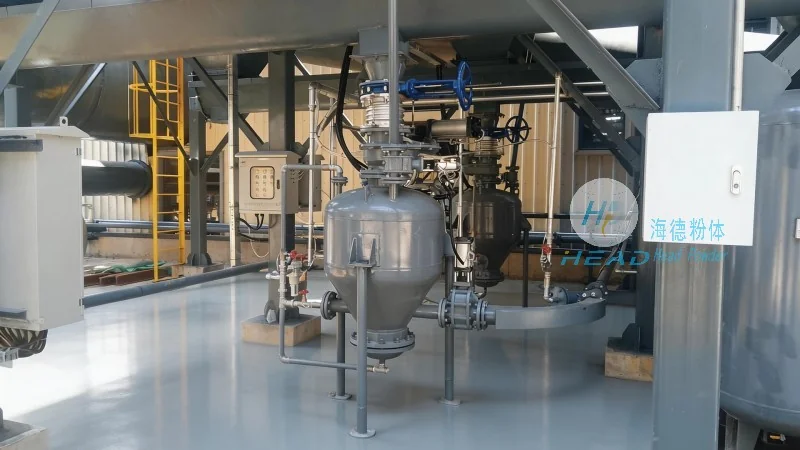
The metering bin pump operates on a principle that combines the functions of a hopper, a pump, and a conveyor. At its core, the system uses a hopper to store bulk materials, which are then metered and transferred through a pump mechanism to the discharge point. The pump, typically a positive displacement type, ensures a consistent flow rate by controlling the volume of material released per cycle. This controlled discharge is then directed to the target location, such as a silo, storage tank, or processing unit.
Key components of the metering bin pump include the hopper, which is designed with a specific geometry to facilitate material flow and prevent clogging. The pump chamber, equipped with rotating or reciprocating parts, creates the necessary pressure to move the material. A control valve or regulator adjusts the flow rate, allowing for precise metering of the material. The discharge outlet is connected to a pipeline or conveyor system, ensuring the material reaches its destination efficiently.
Key Features of Metering Bin Pump Material Conveying Lines
HeadPowder's metering bin pump systems are distinguished by several key features that enhance performance and reliability. One of the primary advantages is the ability to handle a wide range of materials, from fine powders to coarse granules, with minimal maintenance. The system's design minimizes material degradation and contamination, preserving the quality of the product during transport.
Another notable feature is the precise control over material flow. The pump's adjustable speed and volume settings enable operators to match the conveying rate with the processing capacity of downstream equipment. This ensures optimal efficiency and reduces the risk of overloading or underloading the receiving system. Additionally, the system is equipped with safety features, such as pressure relief valves and overload protection, to prevent equipment damage and ensure safe operation.
The robust construction of the metering bin pump, using high-quality materials like stainless steel or corrosion-resistant alloys, ensures durability in harsh industrial environments. The compact design allows for easy integration into existing facilities, while the modular components facilitate maintenance and replacement of parts without extensive downtime. These features collectively contribute to the long service life and low operational costs of the system.
Applications and Benefits in Industrial Settings
Metering bin pump material conveying lines are widely used in industries where consistent and controlled material transport is essential. In mining operations, they are used to transfer ore from storage bins to processing plants, ensuring a steady supply of raw materials. In the construction industry, they facilitate the delivery of cement, sand, and other aggregates to mixing sites, improving productivity and reducing labor costs. The chemical industry benefits from the system's ability to handle corrosive materials safely, with sealed components preventing leaks and contamination.
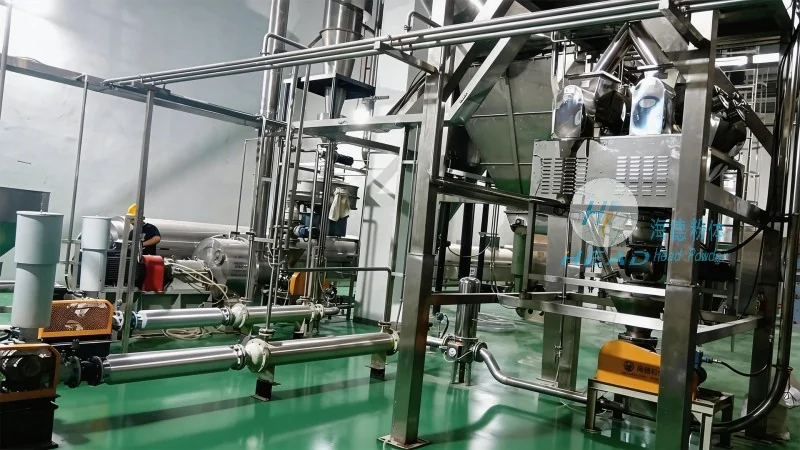
The benefits of using metering bin pump systems extend beyond efficiency. By maintaining a consistent flow rate, the system reduces the need for manual intervention and minimizes the risk of material buildup or blockages. This leads to increased production throughput and lower maintenance expenses. The precise metering capability also supports process control, allowing manufacturers to adjust the material input based on real-time production needs.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of metering bin pump material conveying lines. With years of experience in the material handling industry, the company has developed innovative solutions that combine advanced technology with practical design. Their systems are engineered to deliver reliable performance, high efficiency, and low maintenance, making them an ideal choice for industries seeking to optimize their material transport processes.
By understanding the working principle and features of metering bin pump material conveying lines, businesses can make informed decisions about their material handling infrastructure. The combination of precise control, robust construction, and versatile application makes these systems a valuable asset in modern industrial operations. HeadPowder continues to lead the way in providing high-quality material handling solutions that meet the evolving needs of the industry.