

Working Principle and Characteristics of Compound Fertilizer Powder Conveying
Compound fertilizer powder conveying is a critical process in the fertilizer manufacturing industry, ensuring efficient and safe transportation of bulk powders from production lines to storage or packaging areas. The technology behind this process involves advanced engineering solutions that address the unique challenges of handling fine, dry, and often abrasive materials. Understanding the working principle and key characteristics of such systems is essential for optimizing production efficiency and maintaining product quality.
Working Principle of Compound Fertilizer Powder Conveying
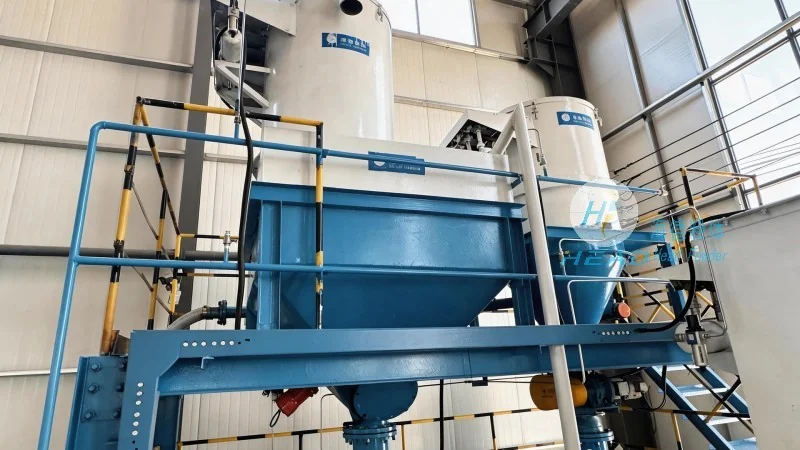
The primary working principle of compound fertilizer powder conveying systems is based on the application of air or gas to transport the powder through a pipeline. There are two main types of gas conveying systems: positive pressure (pressure) and negative pressure (suction) systems. Positive pressure systems utilize a blower or fan to generate compressed air, which is then introduced into the conveying line. This pressurized air pushes the powder particles forward, creating a continuous flow. Negative pressure systems, on the other hand, use a vacuum pump to create a low-pressure environment at the inlet, drawing the powder and air mixture into the system. Both methods rely on the principle of fluidization, where the powder particles are suspended in the air stream, allowing them to be transported over long distances.
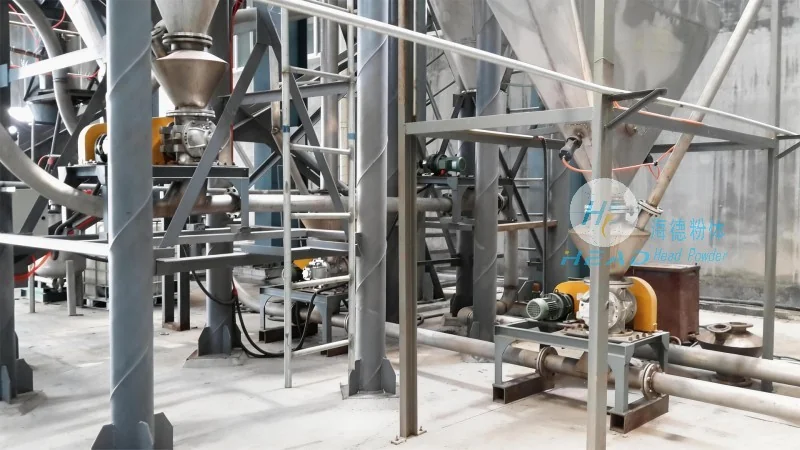
For compound fertilizers, which often consist of multiple nutrient components like nitrogen, phosphorus, and potassium, the conveying system must be designed to handle varying particle sizes and densities. The system typically includes several key components: a feeder to control the flow rate of the powder, a conveying line (usually made of stainless steel or other corrosion-resistant materials to prevent material degradation), a separator to separate the powder from the air at the receiving end, and a filter to clean the exhaust air. The selection of the appropriate conveying method depends on factors such as the distance to be covered, the volume of material to be transported, and the required speed of delivery.
Key Characteristics of Compound Fertilizer Powder Conveying
Compound fertilizer powder conveying systems exhibit several distinct characteristics that make them suitable for industrial applications. Firstly, they offer high efficiency in terms of material throughput, capable of transporting large volumes of powder in a short period. This is particularly important in large-scale fertilizer production, where continuous operation is essential to meet market demands. Secondly, these systems are designed to minimize material loss and contamination, ensuring that the final product remains pure and free from foreign particles. The use of sealed pipelines and proper filtration helps maintain the integrity of the fertilizer.
Another significant characteristic is the environmental friendliness of gas conveying systems. Unlike mechanical systems that may generate dust and cause air pollution, gas conveying minimizes dust emissions, contributing to a cleaner working environment. This is achieved through the use of enclosed pipelines and efficient air filtration systems. Additionally, the systems are energy-efficient, with modern blowers and fans designed to operate at optimal power consumption levels, reducing operational costs for the manufacturer.
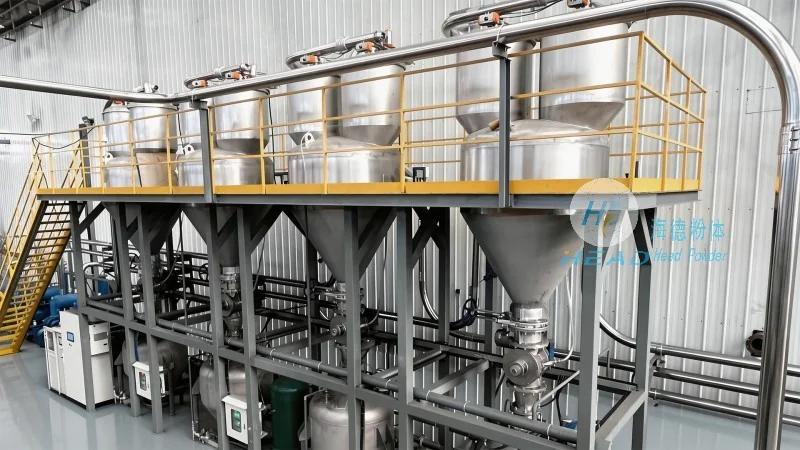
Flexibility is another key characteristic of compound fertilizer powder conveying. The systems can be easily adjusted to accommodate changes in production volume or the type of fertilizer being processed. For example, the speed of the blower or the feed rate can be modified to match the requirements of different batches. This adaptability makes the systems versatile and suitable for various production scenarios, from small-scale local farms to large industrial fertilizer plants.
Technical Advantages and Application Scenarios
Compound fertilizer powder conveying systems offer several technical advantages that enhance their performance and reliability. One of the main advantages is the ability to handle a wide range of powder characteristics, including fine powders, granules, and even wet or sticky materials, with minimal blockage or degradation. The air flow in the system helps prevent material buildup and ensures smooth operation. Another advantage is the reduced risk of mechanical wear and tear compared to mechanical conveyors, as there are fewer moving parts in contact with the powder. This leads to lower maintenance costs and longer equipment lifespan.
Application scenarios for compound fertilizer powder conveying are diverse and widespread. In fertilizer plants, these systems are used to transport raw materials such as urea, phosphate rock, and potassium chloride from storage silos to the production reactors. They are also employed in the final stages of production, moving the finished compound fertilizer from the granulation or drying units to the packaging lines. Additionally, they are used in warehouse management, transferring bulk fertilizer from storage areas to loading docks for distribution. The systems are particularly useful in areas where space is limited or where vertical lifting is required, as they can be designed to move materials vertically as well as horizontally.
Company Information and Service
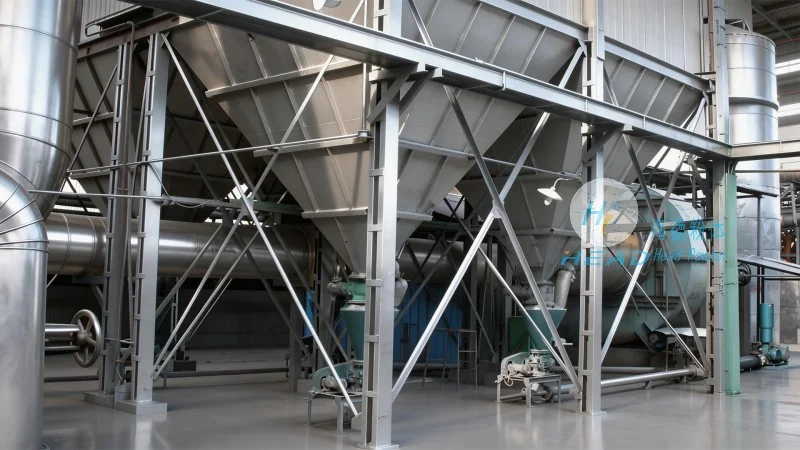
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading provider of specialized engineering solutions for powder handling and conveying systems. HeadPowder is headquartered in Shandong, China, and has established itself as a trusted partner in the fertilizer industry, offering comprehensive services from system design and manufacturing to installation and after-sales support. The company's team of experienced engineers and technicians brings deep expertise in the field of powder technology, ensuring that each project is tailored to meet the specific needs of the client.
HeadPowder specializes in designing and manufacturing compound fertilizer powder conveying systems that are robust, efficient, and compliant with industry standards. The company uses advanced design software and rigorous testing protocols to ensure that its products meet the highest quality and safety requirements. By leveraging its local presence in Shandong, China, HeadPowder can offer competitive pricing and quick delivery times, making it an attractive choice for both domestic and international clients. The company's commitment to innovation and customer satisfaction has earned it a reputation as a reliable and professional partner in the fertilizer processing sector.