

Working Principle and Features of Vacuum Negative Pressure Pneumatic Conveying Systems
Vacuum negative pressure pneumatic conveying systems represent a sophisticated method for transporting bulk materials over short to medium distances. These systems are widely utilized in various industrial sectors due to their efficiency, flexibility, and ability to handle a diverse range of materials. The core of such systems lies in the use of negative pressure to draw material from a source and deliver it to a destination, making them an essential solution for material handling in many applications.
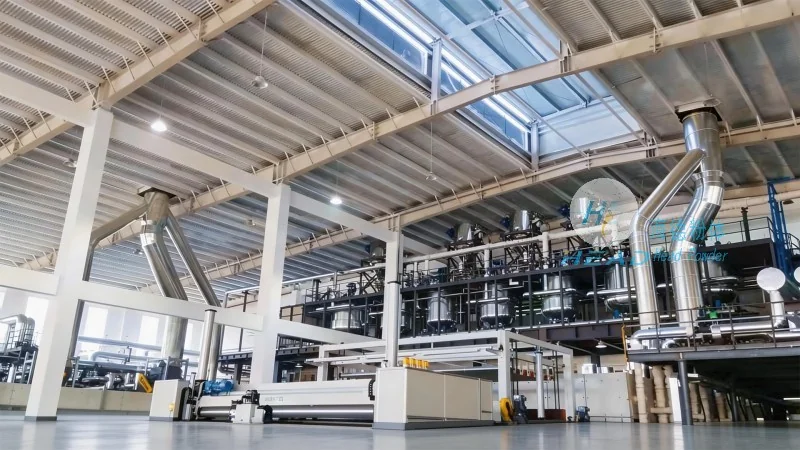
Working Principle of Vacuum Negative Pressure Pneumatic Conveying Systems
The operation of a vacuum negative pressure pneumatic conveying system is based on the principle of creating a pressure differential between the conveying line and the ambient environment. The system typically consists of a vacuum pump, a hopper or material feed point, a conveying line, and a discharge point. The vacuum pump generates a low-pressure environment within the conveying line, which causes air and the material to be drawn from the source into the line. As the material is drawn into the system, it is carried along by the air flow, moving through the pipeline to the discharge point where the material is released. The system maintains a continuous flow by maintaining the vacuum level, ensuring that material is consistently conveyed without the need for mechanical components like augers or belts in the main conveying line.
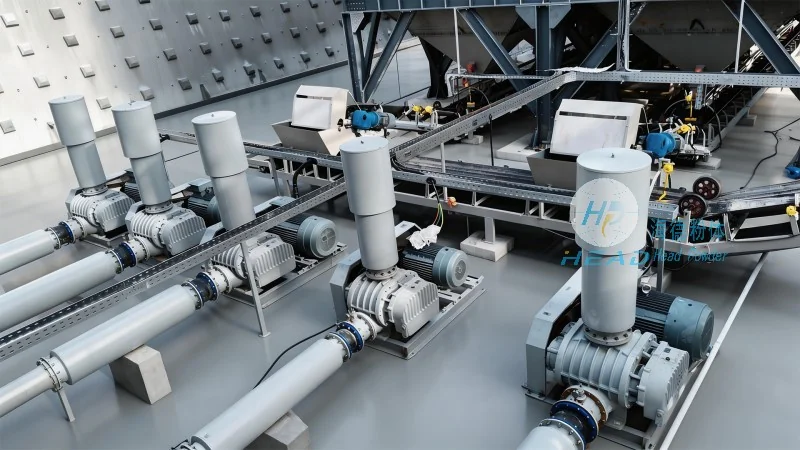
Key Features of Vacuum Negative Pressure Pneumatic Conveying Systems
Several distinct features make vacuum negative pressure pneumatic conveying systems highly effective for material handling. Firstly, they are capable of transporting materials that are difficult to handle by other means, such as powders, granules, and fine particles. The negative pressure environment prevents dust and material from escaping, enhancing safety and environmental compliance. Secondly, these systems are relatively simple in design, with fewer moving parts compared to positive pressure systems, which reduces maintenance requirements and operational costs. Thirdly, they can operate over longer distances compared to some other pneumatic conveying methods, making them suitable for applications where the source and destination are separated by a significant distance. Additionally, the systems are adaptable to various material types and can be customized to meet specific process requirements, providing flexibility in industrial settings.
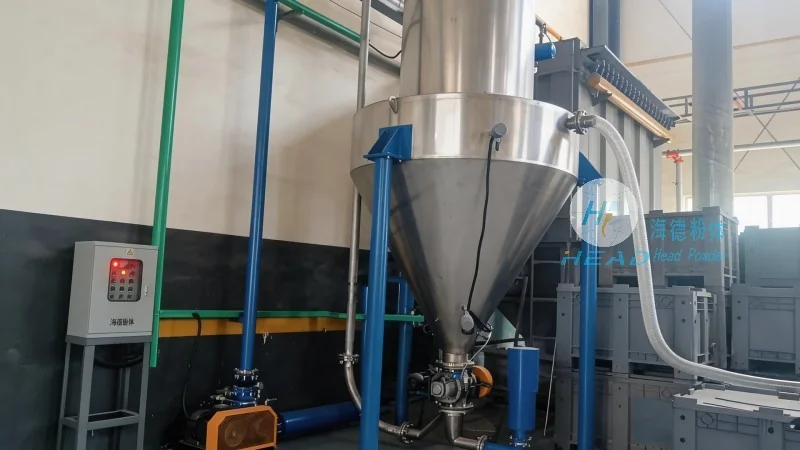
Applications and Benefits in Industrial Settings
Vacuum negative pressure pneumatic conveying systems find extensive applications across multiple industries. In the pharmaceutical and food processing sectors, they are used to transport ingredients and products that require strict contamination control, as the sealed system prevents cross-contamination and maintains product integrity. In the chemical industry, these systems handle powders and granules that may be hazardous or sensitive to moisture, ensuring safe and efficient material transfer. The construction and mining industries also benefit from these systems for transporting raw materials and waste products. The primary benefits include improved safety by containing dust and material, reduced labor costs due to automated operation, and enhanced process efficiency by minimizing material loss and downtime. Moreover, the systems contribute to environmental sustainability by reducing the need for manual handling and minimizing material spillage.
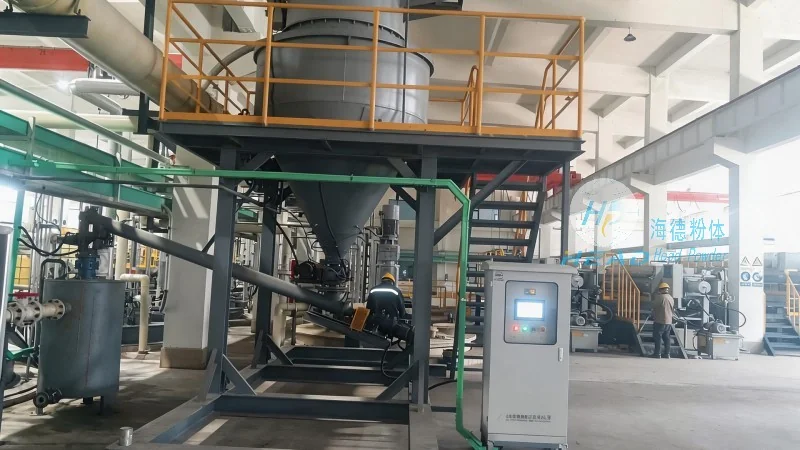
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of advanced material handling solutions. With a focus on innovation and quality, the company specializes in designing and manufacturing vacuum negative pressure pneumatic conveying systems tailored to the diverse needs of industrial clients. HeadPowder's expertise lies in understanding the unique challenges of material handling and developing customized solutions that enhance operational efficiency and safety. The company's commitment to customer satisfaction and technological advancement has established it as a trusted partner in the industry, delivering reliable and efficient systems that meet the highest standards of performance and durability.