

What is a Corn Granular Material Handling System? What are its Design Principles?
For industries dealing with corn processing, the efficient and reliable transportation of corn granules is a critical operational requirement. A corn granular material handling system is a specialized equipment setup designed to move, store, and manage corn kernels in bulk. This system is essential for optimizing workflow in corn milling, feed production, and other agricultural processing applications.
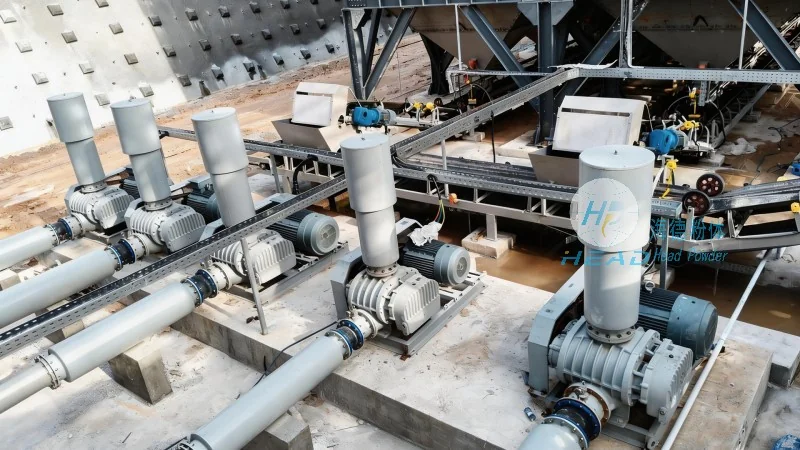
Understanding the Core Components of a Corn Granular Material Handling System
The corn granular material handling system typically consists of several key components that work in concert to ensure smooth material flow. These components include feeders, conveyors, storage silos, and control systems. Each part plays a vital role in maintaining the integrity of the corn granules and ensuring consistent processing speeds.
Design Principles Behind Corn Granular Material Handling Systems
The design of a corn granular material handling system is guided by several fundamental principles aimed at maximizing efficiency, minimizing material loss, and ensuring safety. These principles include:
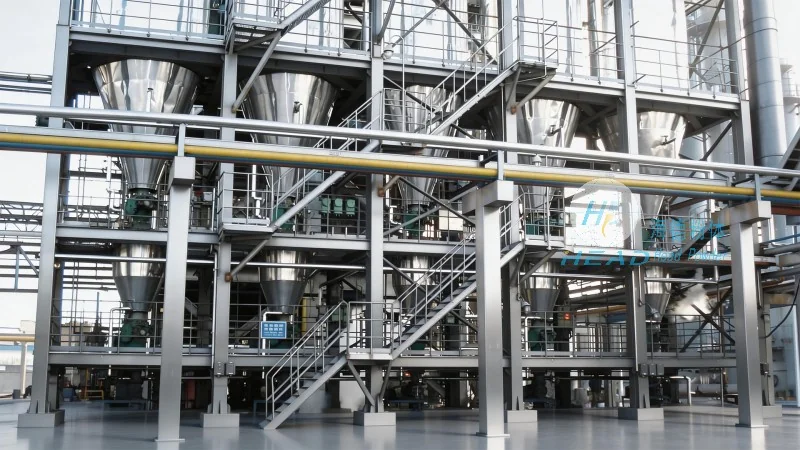
- Material Flow Optimization: The system is engineered to minimize friction and prevent material degradation during transport. This involves selecting appropriate conveyor types, such as screw conveyors or bucket elevators, based on the characteristics of the corn granules.
- Space Efficiency: Given the high volume of corn granules, the system is designed to maximize vertical and horizontal space utilization. This is crucial for industrial settings where floor space is limited.
- Durability and Corrosion Resistance: The equipment is constructed from materials that can withstand the abrasive nature of corn kernels and potential moisture exposure. This ensures long-term reliability and reduces maintenance costs.
- Integration with Processing Lines: The system is designed to seamlessly integrate with existing corn processing lines, allowing for a continuous flow from raw material reception to final product packaging.
Key Features of a Reliable Corn Granular Material Handling System
Effective corn granular material handling systems from manufacturers like Shandong HeadPowder Engineering Co., Ltd. incorporate several advanced features that enhance performance and user experience. These features include:
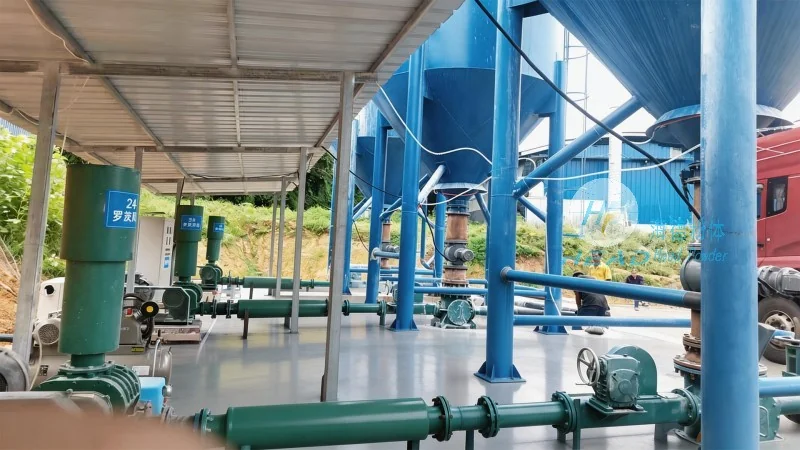
- Variable Speed Control: The ability to adjust conveyor speeds based on processing demands allows for precise control over material flow rates.
- Material Level Monitoring: Sensors and indicators provide real-time feedback on silo and hopper levels, preventing overfilling and ensuring optimal inventory management.
- Easy Maintenance Access: Design elements that facilitate regular maintenance, such as removable components and clear access points, help reduce downtime and operational costs.
- Energy Efficiency: Modern systems are engineered to minimize energy consumption while maintaining high throughput, aligning with sustainability goals.
Applications of Corn Granular Material Handling Systems
Corn granular material handling systems are widely used in various industries, including:
- Corn Milling: For transporting raw corn kernels to grinding and milling equipment.
- Animal Feed Production: To move corn as a primary ingredient in feed formulations.
- Food Processing: In the production of corn-based products like corn syrup and starch.
- Agricultural Storage: For bulk storage and distribution of corn for both domestic and international markets.
Choosing the Right Corn Granular Material Handling System
When selecting a corn granular material handling system, it is essential to consider factors such as production capacity, space availability, and specific processing requirements. Working with a reputable manufacturer like Shandong HeadPowder Engineering Co., Ltd. ensures that the system is tailored to meet these needs, providing a reliable and efficient solution for corn handling operations.