

What is a Positive Pressure Dilute Phase Powder Conveying System? And What Are Its Design Principles
Understanding the Positive Pressure Dilute Phase Powder Conveying System and Its Design Principles
Introduction to Positive Pressure Dilute Phase Powder Conveying
The positive pressure dilute phase powder conveying system is a specialized industrial solution designed for the efficient transportation of bulk powders over long distances. This technology operates by creating a positive pressure environment within the conveying line, ensuring that the powder is continuously moved through the system with minimal pressure loss and optimal flow characteristics. The system is widely used in various industries, including chemical, food, pharmaceutical, and mining, where the reliable and safe transfer of powders is critical to operational efficiency.
Key Components of the System
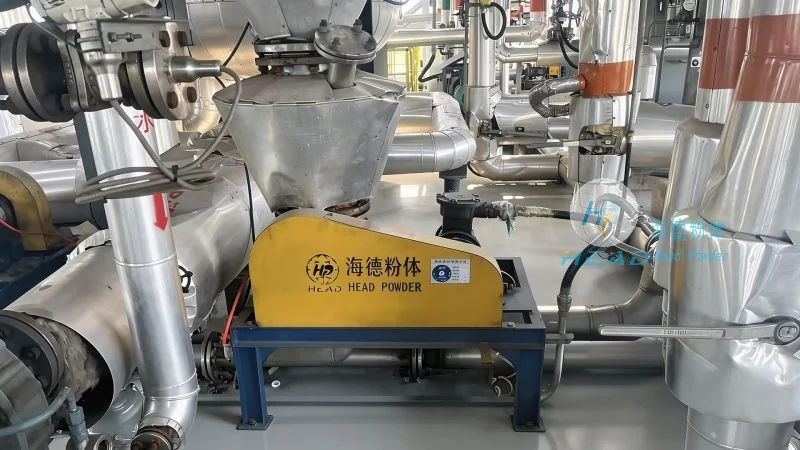
At the core of a positive pressure dilute phase powder conveying system are several key components that work in tandem to ensure effective operation. These components include the material feed hopper, which provides a consistent supply of powder to the system; the air compressor or blower, which generates the necessary positive pressure to move the powder; the conveying line, typically made of durable materials such as stainless steel or plastic, which houses the powder and air mixture; and the control system, which monitors and regulates the flow of material and air to maintain optimal performance. Each component is carefully selected and integrated to ensure the system operates efficiently and reliably under various operating conditions.
Design Principles of the System
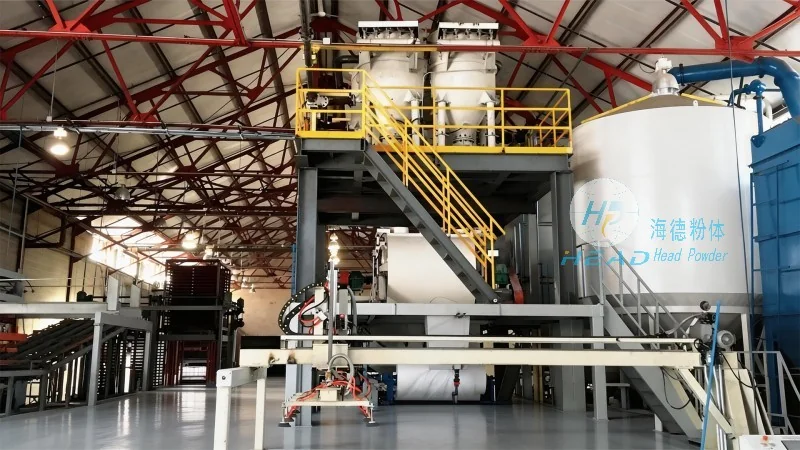
The design principles of a positive pressure dilute phase powder conveying system are centered on maintaining a dilute phase of powder in the conveying line, which minimizes the risk of blockages and ensures smooth material flow. The system operates by introducing a high-velocity air stream into the conveying line, which suspends the powder particles and carries them through the system. The design must consider factors such as the particle size distribution of the powder, the air velocity required to keep the powder suspended, and the overall system pressure to prevent excessive energy consumption or equipment wear. Engineers at Shandong HeadPowder Engineering Co., Ltd. apply advanced engineering principles to optimize these parameters, ensuring that the system meets the specific requirements of each application while maintaining high efficiency and reliability.
Advantages of Positive Pressure Dilute Phase Conveying
Compared to other powder conveying methods, such as vacuum systems or dense phase conveying, the positive pressure dilute phase system offers several distinct advantages. One of the primary benefits is its ability to handle a wide range of powder types, including fine, abrasive, and corrosive materials, without causing damage to the equipment. The system also provides a high degree of flexibility in terms of conveying distance and layout, as the positive pressure allows for longer lines and more complex routing without significant pressure drops. Additionally, the system is generally more energy-efficient than vacuum systems, as it requires less power to maintain the positive pressure and move the material. These advantages make the positive pressure dilute phase system an ideal choice for many industrial applications where reliable and efficient powder transfer is essential.
Applications and Industries
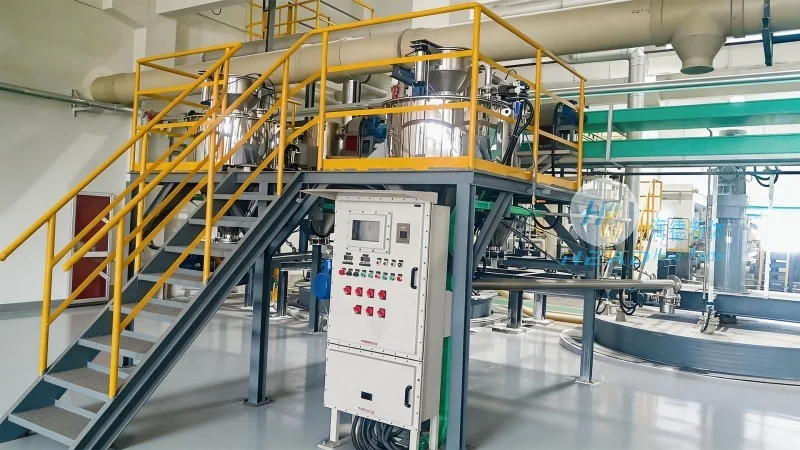
The positive pressure dilute phase powder conveying system is used in a variety of industries where bulk powder handling is a critical part of the production process. In the chemical industry, it is commonly used to transport raw materials and finished products between processing units, ensuring a continuous and safe supply chain. In the food and pharmaceutical industries, the system is employed to handle powders that require strict hygiene and contamination control, as the positive pressure environment minimizes the risk of external contamination. The mining industry also utilizes this technology to transport ore and other minerals from processing plants to storage facilities or for further processing. The versatility of the system makes it suitable for a wide range of applications, from small-scale operations to large-scale industrial facilities.
Customization and Integration
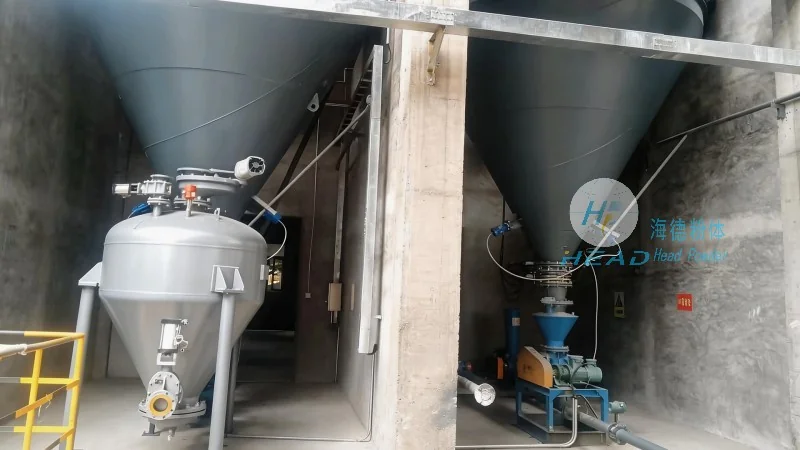
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized positive pressure dilute phase powder conveying systems tailored to the specific needs of each client. The company's engineers work closely with clients to understand their operational requirements, including the type of powder, conveying distance, and required flow rate, to develop a system that meets all specifications. The systems are designed with modular components, allowing for easy installation and maintenance, and can be integrated with existing production lines or new facilities. The company also provides comprehensive support, including installation, commissioning, and ongoing maintenance services, to ensure that the system operates at peak performance throughout its lifecycle.
Conclusion
In conclusion, the positive pressure dilute phase powder conveying system is a highly effective and reliable technology for the transportation of bulk powders. Its design principles, which focus on maintaining a dilute phase of powder and utilizing positive pressure, ensure efficient and safe operation. The system offers numerous advantages over other conveying methods, including flexibility, energy efficiency, and the ability to handle a wide range of powder types. As a leading provider in the industry, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and improve its systems to meet the evolving needs of its clients, providing high-quality solutions that enhance operational efficiency and productivity.