

What is a Bulk Bag Unpacking and Powder Conveying Line? And What Are Its Design Principles?
For industries dealing with bulk powders, the efficient handling and transportation of materials from large-scale packaging like bulk bags are critical. A bulk bag unpacking and powder conveying line is a specialized system designed to automate the process of unloading, transferring, and distributing powder materials from bulk bags into processing or storage areas. This system integrates multiple components to ensure a seamless workflow, enhancing productivity and reducing manual labor in powder handling operations.
Understanding the Core Components of a Bulk Bag Unpacking and Powder Conveying Line
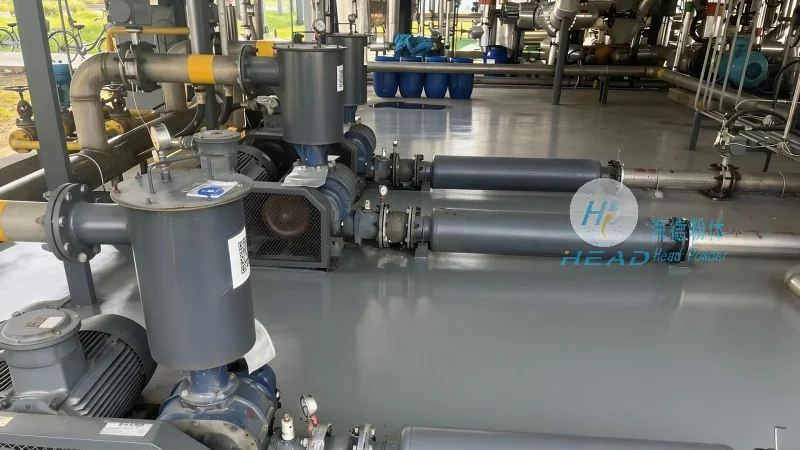
The design of a bulk bag unpacking and powder conveying line is built around several key components that work in tandem to achieve efficient material handling. At the heart of the system is the bulk bag unloader, which is typically equipped with a discharge spout or a bottom opening mechanism to allow the powder to flow out. This component is often connected to a hopper or a buffer tank that collects the material before it is transferred to the conveying system. The conveying system itself may include various types of equipment such as screw conveyors, pneumatic conveying lines, or bucket elevators, depending on the specific requirements of the application. Additionally, the line may incorporate a dust collection system to maintain air quality and prevent powder contamination, which is essential for both safety and product integrity.
Design Principles for Optimal Performance and Reliability
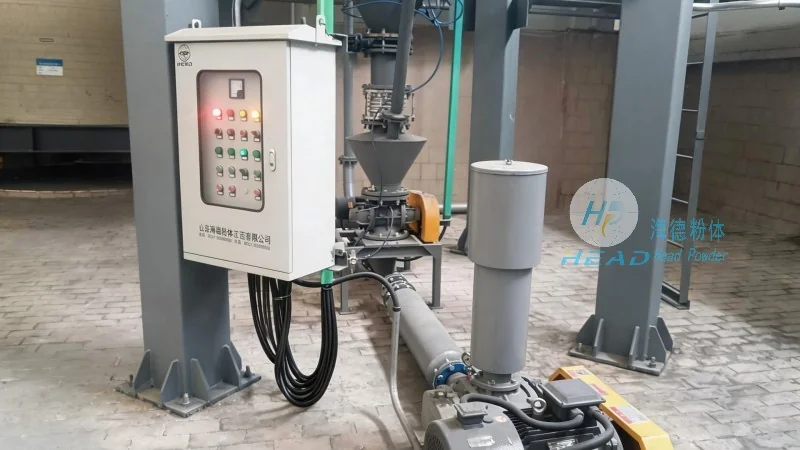
The design principles behind a bulk bag unpacking and powder conveying line focus on maximizing efficiency, minimizing downtime, and ensuring the safety of operators and the integrity of the material. One of the primary design considerations is the need for a dust-free environment, as many powders are fine and can cause respiratory issues or clog equipment if not properly contained. Therefore, the system is often enclosed or equipped with a dust extraction system that captures airborne particles and returns them to the hopper or a collection container. Another key principle is the integration of automation, which reduces the need for manual intervention and minimizes the risk of human error. This includes features like automatic bulk bag opening, level sensors to monitor material levels, and control systems that adjust the flow rate based on demand. The design also prioritizes material compatibility, ensuring that all components are constructed from materials that are resistant to the specific powders being handled, such as stainless steel or special coatings to prevent corrosion or contamination.
Applications and Industries Benefiting from This Technology
Bulk bag unpacking and powder conveying lines are widely used across various industries where bulk powders are a key component. These include pharmaceutical manufacturing, food processing, chemical production, and agricultural applications. In the pharmaceutical industry, for example, the system must meet stringent regulatory requirements for cleanliness and contamination control, making it essential to use materials and designs that prevent cross-contamination and ensure product safety. In food processing, the system is designed to handle food-grade powders while maintaining hygiene standards, often incorporating stainless steel components and easy-to-clean surfaces. Chemical manufacturers benefit from the ability to handle a wide range of chemical powders, from corrosive substances to fine powders that require gentle handling to prevent agglomeration. Agricultural industries use these systems to handle fertilizers, pesticides, and other agricultural chemicals, ensuring efficient distribution and minimizing waste.
Advantages of Implementing a Bulk Bag Unpacking and Powder Conveying Line
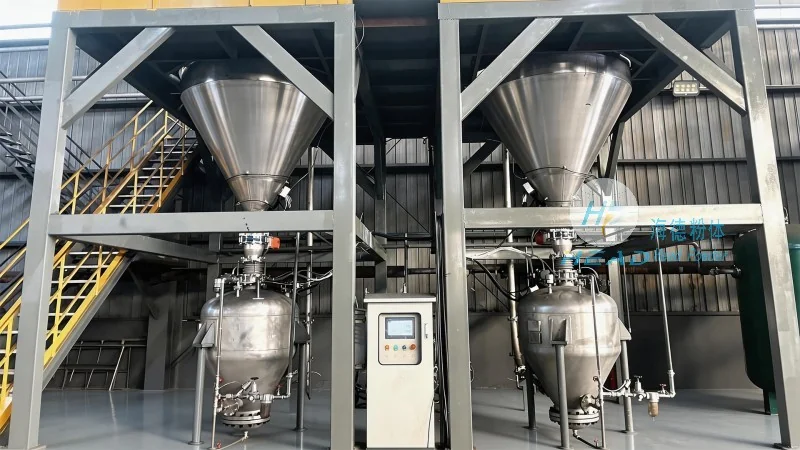
Adopting a bulk bag unpacking and powder conveying line offers numerous advantages for businesses dealing with bulk powders. The most significant benefit is the improvement in operational efficiency, as the system automates the entire process from unloading to conveying, reducing the time and labor required for manual handling. This leads to increased productivity and lower labor costs. Additionally, the system enhances safety by minimizing the exposure of operators to dust and heavy lifting, reducing the risk of workplace accidents. The enclosed design and dust collection systems also help maintain a clean and healthy working environment, which is crucial for industries where product quality and worker health are paramount. Another advantage is the reduction in material waste, as the system ensures that the entire contents of the bulk bag are transferred without spillage or loss. This not only saves costs but also contributes to environmental sustainability by minimizing the amount of material that needs to be disposed of or reprocessed.
Customization and Scalability: Tailoring the System to Specific Needs
One of the key strengths of a bulk bag unpacking and powder conveying line is its ability to be customized to meet the specific needs of different applications. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this field, offers tailored solutions that can be scaled to accommodate varying production volumes and material types. The company's expertise lies in designing systems that integrate seamlessly with existing production lines, ensuring minimal disruption during installation. For example, a system can be configured with different conveying speeds, hopper sizes, or discharge mechanisms to handle a wide range of bulk bag sizes and powder characteristics. The company also provides after-sales support and maintenance services to ensure the long-term reliability and performance of the system. This level of customization and support makes the bulk bag unpacking and powder conveying line a versatile solution for businesses looking to optimize their powder handling processes.