

Design of Rare Earth Negative Pressure Pneumatic Conveying Equipment
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and development of advanced negative pressure pneumatic conveying systems tailored for handling rare earth materials. This article delves into the technical aspects and design considerations of such equipment, highlighting how it addresses the unique challenges associated with rare earth ore and concentrate processing.
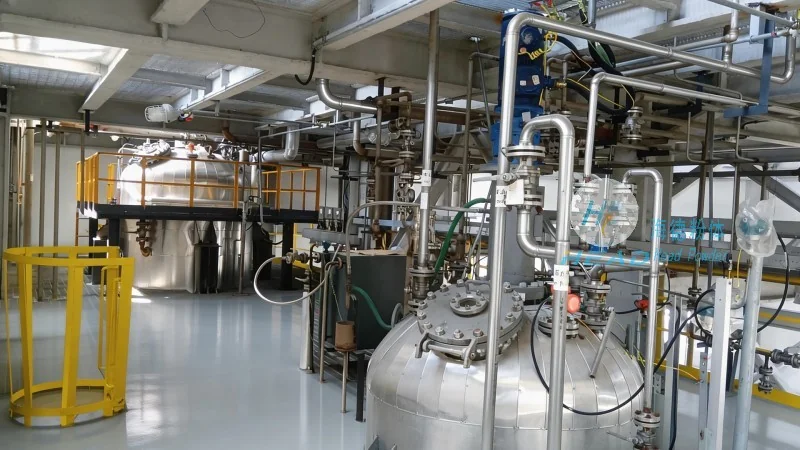
Key Features of the Negative Pressure Pneumatic Conveying System
The negative pressure pneumatic conveying equipment designed by HeadPowder is engineered to efficiently transport rare earth powders and granules over long distances while maintaining product integrity. The system operates under a vacuum environment, which draws material from the source to the destination, eliminating the need for positive pressure systems that may cause material degradation or contamination. This design ensures a gentle handling process, preserving the physical and chemical properties of the rare earth materials, which is critical for downstream processing and quality control.
A core component of the system is the airlock feeder, which regulates the flow of material into the conveying line, preventing blockages and ensuring consistent feed rates. The conveying pipeline is constructed from corrosion-resistant materials, such as stainless steel or specialized alloys, to withstand the acidic and abrasive nature of rare earth compounds. Additionally, the system incorporates advanced filtration and dust collection mechanisms to maintain air quality and comply with environmental regulations.
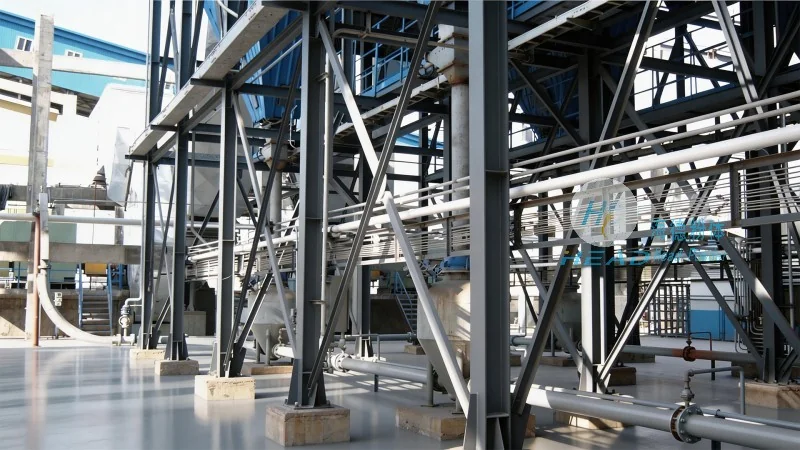
Design Considerations for Rare Earth Material Handling
When designing a pneumatic conveying system for rare earth materials, several factors must be carefully considered to optimize performance and longevity. First, the material's particle size distribution and flow characteristics are analyzed to determine the appropriate air velocity and pipeline diameter. The system is designed to operate within the "inertial" or "travelling" range, where particles are fully suspended by the air stream, minimizing wear on the pipeline and reducing the risk of clogging. This is particularly important for fine rare earth powders, which are prone to agglomeration.
Another critical consideration is the prevention of material degradation due to heat or friction. The conveying system incorporates cooling mechanisms, such as insulated pipelines or temperature-controlled zones, to maintain the material at an optimal temperature. Furthermore, the use of low-friction materials for pipeline components and the implementation of smooth, curved bends reduce the risk of particle attrition, ensuring that the final product meets stringent purity standards.
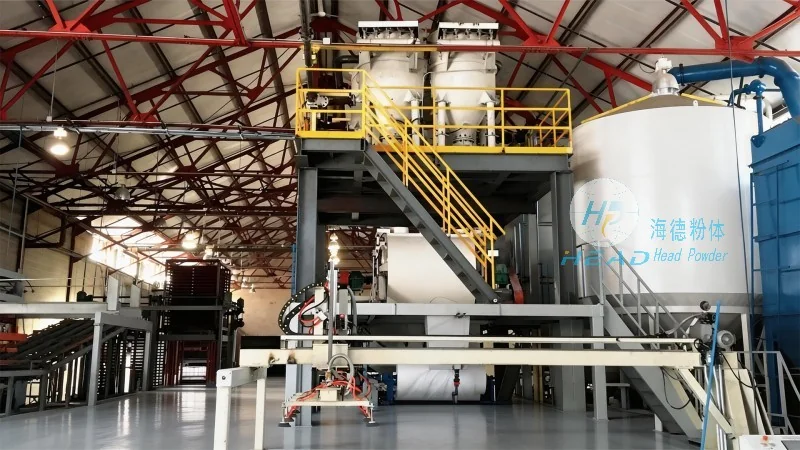
Company Background and Expertise
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, has established itself as a trusted provider of customized material handling solutions for the rare earth industry. With years of experience in designing and manufacturing pneumatic conveying systems, the company leverages its deep understanding of rare earth material properties and processing requirements to deliver tailored solutions that meet the specific needs of clients. The company's engineering team employs state-of-the-art design software and rigorous testing protocols to ensure that each system is optimized for efficiency, reliability, and safety.
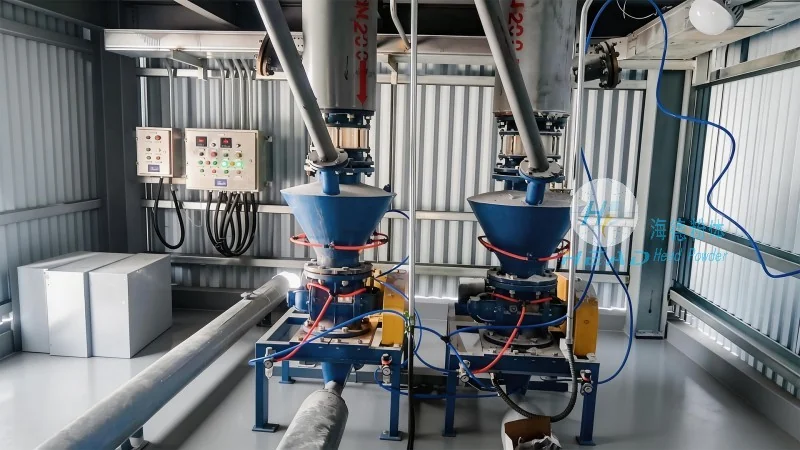
HeadPowder's commitment to quality and innovation is reflected in its adherence to international standards and continuous research and development efforts. The company collaborates closely with clients to understand their operational challenges and provides comprehensive support, from system design and installation to maintenance and troubleshooting. This customer-centric approach has earned HeadPowder a reputation for delivering reliable and efficient negative pressure pneumatic conveying equipment that enhances productivity and reduces operational costs in rare earth processing facilities.
Conclusion
The negative pressure pneumatic conveying equipment designed by HeadPowder represents a sophisticated solution for the efficient and safe handling of rare earth materials. By integrating advanced engineering principles, corrosion-resistant materials, and precise control systems, the system ensures optimal performance while preserving the integrity of the product. As a leading provider in the industry, HeadPowder continues to innovate and adapt its solutions to meet the evolving demands of the rare earth sector, providing clients with reliable and high-performance material handling systems.