

Airborne Transport of Heptahydrate Magnesium Sulfate: An Efficient and Environmentally Friendly Material Handling Solution
Heptahydrate magnesium sulfate, commonly known as Epsom salt, is a widely used chemical compound in various industrial and agricultural applications. The efficient and safe transportation of this material is crucial for optimizing production processes and ensuring compliance with environmental standards. This article explores the advantages of using pneumatic conveying systems for the transport of heptahydrate magnesium sulfate, highlighting the benefits offered by Shandong HeadPowder Engineering Co., Ltd. as a leading provider in the field.
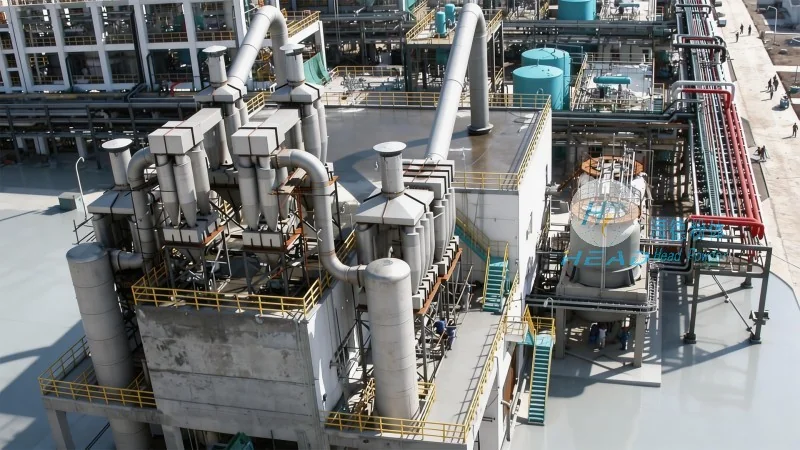
Understanding Heptahydrate Magnesium Sulfate and Its Handling Requirements
Heptahydrate magnesium sulfate (MgSO₄·7H₂O) is a hygroscopic, white crystalline solid that is commonly used in pharmaceuticals, fertilizers, and water treatment. Due to its granular or powder form, traditional bulk material handling methods such as belt conveyors or bucket elevators may pose challenges related to dust generation, material degradation, and operational inefficiencies. Pneumatic conveying offers a solution by transporting the material in a sealed system using air or other gases, minimizing exposure to the environment and reducing the risk of contamination.
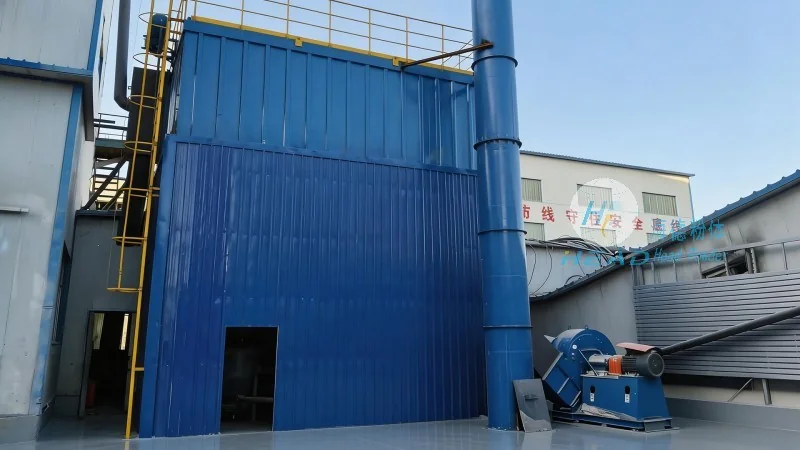
Efficiency and Environmental Benefits of Pneumatic Conveying
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing advanced pneumatic conveying systems tailored to the unique properties of heptahydrate magnesium sulfate. The company’s solutions are engineered to enhance material flow, reduce energy consumption, and minimize environmental impact. By utilizing positive or negative pressure systems, the conveying process can be optimized for different material characteristics, ensuring consistent performance and reliability. The sealed nature of pneumatic conveying also helps in controlling dust emissions, aligning with modern environmental regulations and promoting a cleaner working environment.
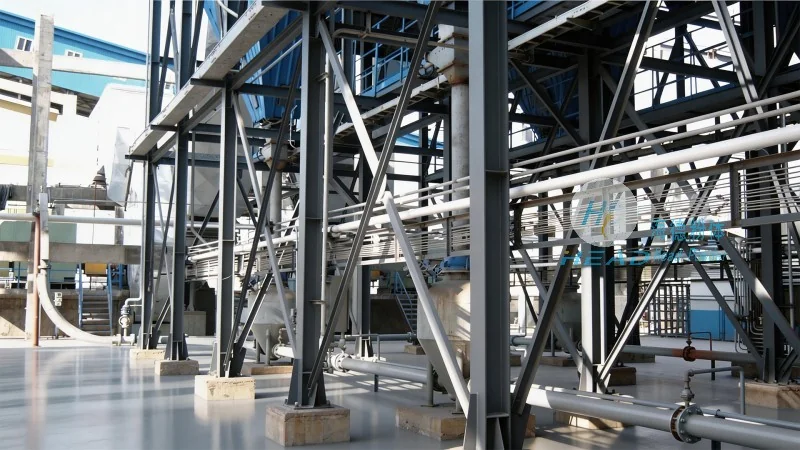
Customized Solutions for Diverse Application Needs
HeadPowder provides customized pneumatic conveying solutions that address the specific requirements of clients in the heptahydrate magnesium sulfate industry. Whether for small-scale laboratory applications or large-scale industrial production, the company’s systems are designed to handle varying flow rates, material densities, and processing conditions. The integration of advanced control technologies allows for real-time monitoring and adjustment of the conveying process, ensuring optimal performance and minimizing downtime. Additionally, the modular design of the systems enables easy scalability and adaptability to changing production needs.
Reliability and Maintenance Considerations
Investing in a pneumatic conveying system for heptahydrate magnesium sulfate requires consideration of long-term reliability and maintenance. Shandong HeadPowder Engineering Co., Ltd. offers durable components and robust system designs that are built to withstand the challenges of handling hygroscopic materials. The company provides comprehensive maintenance services and technical support to ensure the longevity of the equipment and maintain consistent operational efficiency. Regular inspections and preventive maintenance programs are recommended to keep the system in optimal condition, reducing the risk of breakdowns and ensuring uninterrupted production.
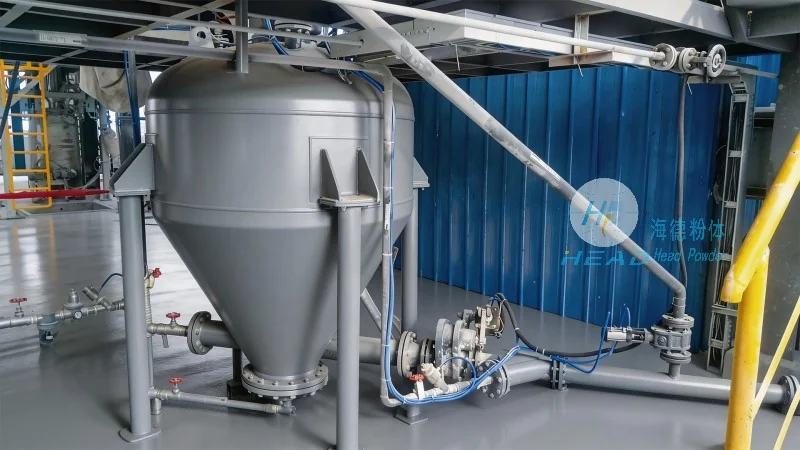
Conclusion: A Sustainable Approach to Material Handling
For industries dealing with heptahydrate magnesium sulfate, pneumatic conveying represents a forward-thinking solution that combines efficiency, environmental responsibility, and operational reliability. Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner in delivering customized pneumatic conveying systems that meet the evolving needs of the market. By prioritizing innovation and customer satisfaction, the company continues to contribute to the advancement of sustainable material handling practices in the chemical and industrial sectors.