

Operation Process and Working Principle of a Dust Removal Coke Powder Material Pneumatic Conveying S
HeadPowder, a leading engineering company based in Shandong, China, specializes in providing advanced solutions for material handling, particularly in the field of dust removal and pneumatic conveying systems for coke powder. The company's expertise lies in designing and manufacturing efficient systems that ensure safe, reliable, and environmentally friendly transportation of fine powders like coke, which are critical in various industrial applications.
Working Principle of the Pneumatic Conveying System
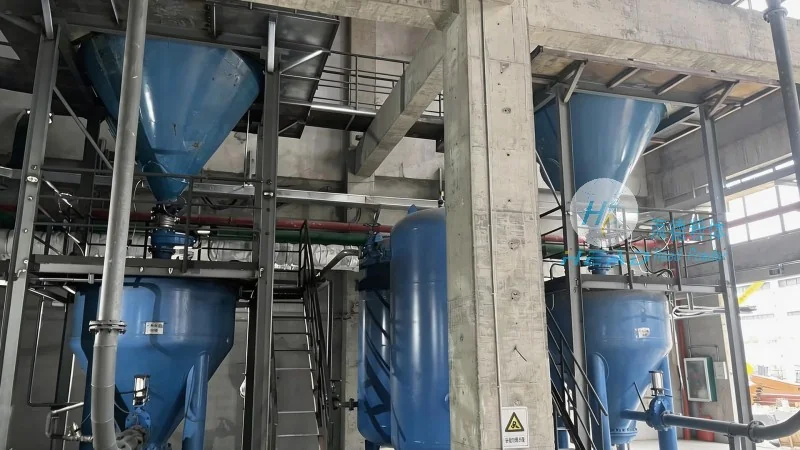
The core of the dust removal coke powder material pneumatic conveying system is the utilization of air flow to transport particulate materials. The system operates on the principle of creating a pressure differential or vacuum to move the coke powder through a network of pipes. Key components include a feed hopper, an air compressor or vacuum pump, a conveying line, a separation unit, and a discharge outlet. The feed hopper holds the coke powder, and as air is introduced, it creates a flow that lifts and transports the powder particles. The separation unit then separates the powder from the air, ensuring that the powder is delivered to the intended destination while the air is filtered and recycled or vented, minimizing dust emissions and maintaining environmental compliance.
Operation Process of the System
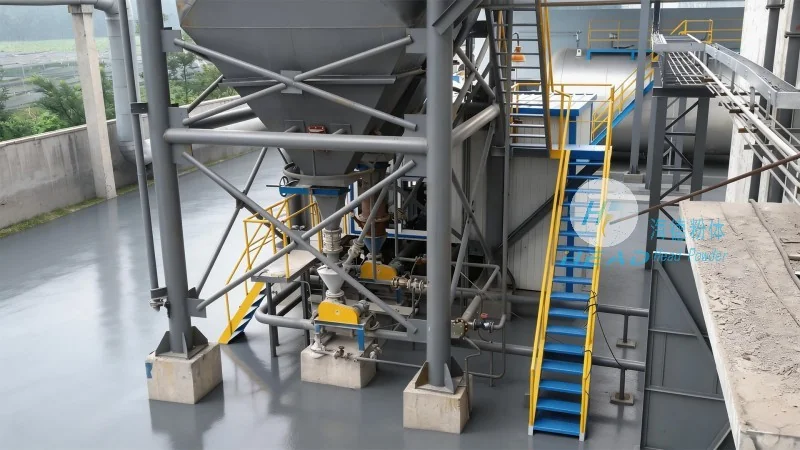
The operation of the HeadPowder dust removal coke powder pneumatic conveying system follows a systematic process. Initially, the coke powder is fed into the hopper from the source, such as a storage silo or a production line. The system then activates the air compressor, which generates the necessary pressure or vacuum to initiate the conveying process. As the air flows through the conveying line, it carries the coke powder particles, moving them from the feed point to the discharge point. The separation unit, typically a cyclone or a bag filter, captures the powder from the air stream. The separated powder is collected in a discharge bin, while the air is either filtered and recirculated back into the system or released safely. This process ensures continuous and efficient operation, with minimal downtime and consistent performance.
Technical Features and Advantages
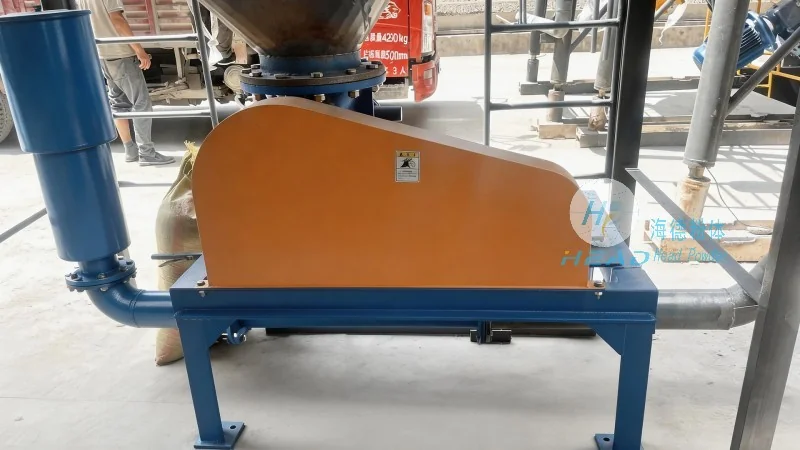
HeadPowder's dust removal coke powder pneumatic conveying system is equipped with several technical features that enhance its performance and reliability. The system utilizes advanced control systems that monitor and adjust air pressure, flow rate, and particle velocity in real-time, optimizing the conveying efficiency. The use of high-quality materials, such as stainless steel or corrosion-resistant alloys, ensures durability and resistance to the abrasive nature of coke powder. Additionally, the system incorporates dust collection and filtration mechanisms that comply with environmental regulations, reducing particulate emissions and improving workplace safety. The compact design and modular construction allow for easy installation and maintenance, reducing operational costs and increasing the system's lifespan.
Application Scenarios
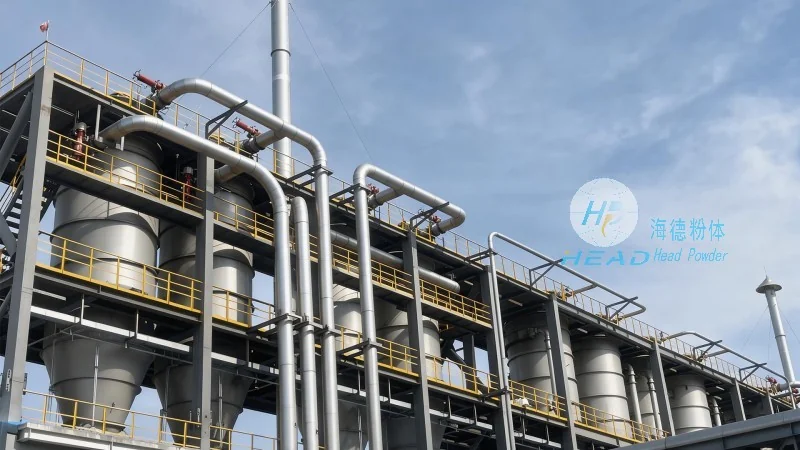
The dust removal coke powder pneumatic conveying system is widely used in various industrial sectors, particularly in the steel and chemical industries. In steel mills, it is employed to transport coke from storage facilities to blast furnaces or other processing units, ensuring a continuous supply of raw materials. In chemical plants, the system is used to handle coke powder during the production of chemicals, such as in the manufacturing of carbon black or other carbon-based products. The system's ability to handle fine, abrasive powders while maintaining low dust emissions makes it an ideal solution for applications where material purity and environmental compliance are critical. HeadPowder's systems have been successfully implemented in numerous projects across China, demonstrating their effectiveness and reliability in meeting the demanding requirements of modern industrial operations.