

Operation Process and Working Principle of Intelligent Centralized Powder Conveying Machine
HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced powder handling solutions. The intelligent centralized powder conveying machine is a sophisticated system designed to efficiently manage the transportation of bulk powders in industrial settings. This equipment integrates cutting-edge technology to ensure reliable, safe, and efficient operation, addressing the complex challenges of powder handling in various industries such as pharmaceuticals, food processing, and chemical manufacturing. The system is engineered to handle a wide range of powder types, from fine powders to bulk materials, while maintaining high standards of hygiene and material integrity.
Working Principle of the Intelligent Centralized Powder Conveying Machine
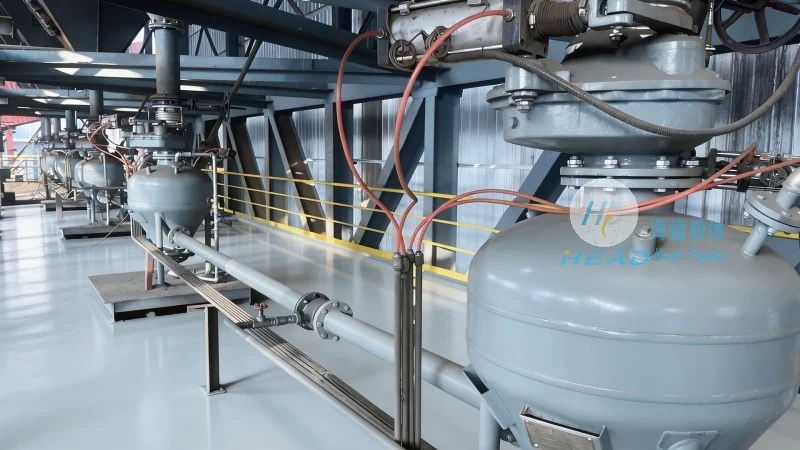
The intelligent centralized powder conveying machine operates on a centralized control system that coordinates multiple components to achieve seamless powder transport. The system typically includes a main conveyor, feeding mechanisms, and control units that work in tandem to move powders from storage to processing or packaging areas. Key components such as rotary valves, pneumatic or mechanical conveyors, and sensors are integrated to monitor and regulate the flow of material. The control system uses real-time data to adjust parameters like pressure, speed, and flow rate, ensuring optimal performance and minimizing downtime. This centralized approach allows for better management of inventory, reduces the risk of material loss or contamination, and enhances overall operational efficiency. The machine also incorporates safety features, including emergency stop buttons and overload protection, to safeguard both personnel and equipment during operation.
Operation Process of the Intelligent Centralized Powder Conveying Machine
The operation process of the intelligent centralized powder conveying machine begins with the preparation of the powder material. The system is designed to handle various types of powders, including fine powders, granules, and bulk materials, by adjusting the feeding mechanisms and conveyor settings. The initial step involves loading the powder into the storage hopper, which is equipped with a level sensor to monitor the material level. Once the hopper is filled, the feeding device, such as a rotary valve or screw feeder, starts to transport the powder into the main conveyor. The conveyor then moves the material through the system, with intermediate storage or processing units as needed. The control panel allows operators to monitor the entire process, adjust settings, and receive alerts for any anomalies. The system continues to operate until the target destination is reached, ensuring a continuous and reliable flow of powder. At the end of the process, the powder is discharged into the receiving container, completing the cycle. The intelligent features of the machine enable automatic adjustments based on real-time conditions, such as changes in material density or conveyor load, maintaining consistent performance throughout the operation. The system also supports remote monitoring and diagnostics, allowing for proactive maintenance and reducing the likelihood of unexpected failures.
Key Features and Benefits
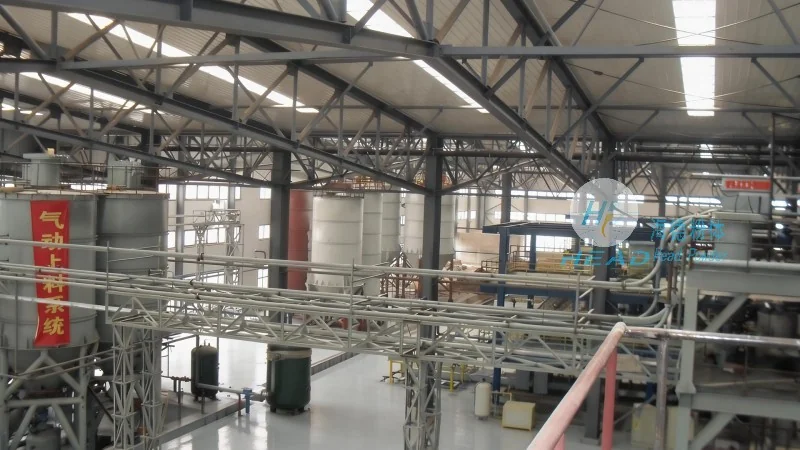
The intelligent centralized powder conveying machine from HeadPowder offers several key features that enhance its performance and usability. These include advanced control systems with user-friendly interfaces, real-time monitoring capabilities, and automated adjustment functions. The machine is designed for high efficiency, with minimal energy consumption and low maintenance requirements. It also ensures high levels of hygiene and material purity, making it suitable for industries with strict quality standards. Additionally, the system is scalable, allowing for easy expansion or integration with existing production lines. The benefits of using this equipment include improved productivity, reduced labor costs, enhanced safety, and better control over the powder handling process.
Application Scenarios
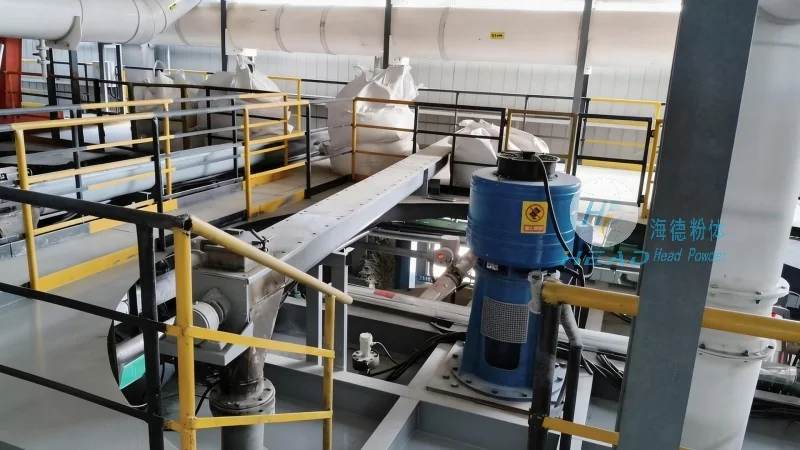
The intelligent centralized powder conveying machine is widely used in various industrial applications. In the pharmaceutical industry, it is used to transport active pharmaceutical ingredients (APIs) and excipients with high precision and minimal contamination. In the food processing sector, it handles ingredients like flour, sugar, and spices, ensuring consistent quality and safety. The machine is also employed in the chemical industry for transporting raw materials and intermediates, supporting efficient production processes. Its versatility makes it suitable for a range of industries where reliable and efficient powder handling is critical to operational success.
Conclusion
HeadPowder's intelligent centralized powder conveying machine represents a significant advancement in powder handling technology. By integrating intelligent control systems and advanced components, the machine provides reliable, efficient, and safe operation for various industrial applications. The system's ability to adapt to different powder types and operating conditions, combined with its user-friendly interface and remote monitoring capabilities, makes it an ideal solution for modern industrial needs. As a leading manufacturer based in Shandong, China, HeadPowder continues to innovate and provide high-quality equipment that meets the evolving demands of the industry.