

Principles and Application Scenarios of Intelligent Centralized Material Pneumatic Conveying Systems
Intelligent centralized material pneumatic conveying systems represent a sophisticated solution for material handling in industrial settings. Developed by Shandong HeadPowder Engineering Co., Ltd., these systems integrate advanced technology to enhance efficiency, safety, and operational control in material transport processes. This article explores the fundamental principles behind these systems and highlights key application scenarios where they deliver significant advantages.
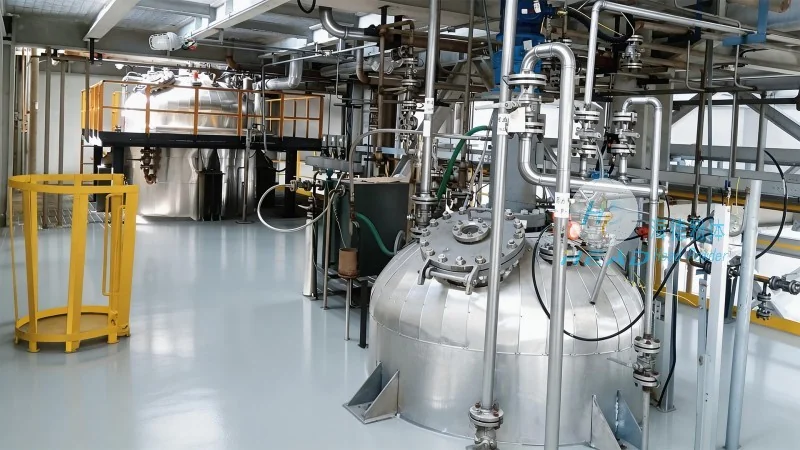
Company Overview: HeadPowder
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in material handling equipment. With a strong presence in China, particularly in Shandong province, the company has built a reputation for delivering high-quality, reliable pneumatic conveying solutions tailored to diverse industrial needs. The company’s commitment to innovation and customer-centric design ensures that their products, including intelligent centralized material pneumatic conveying systems, meet the evolving demands of modern manufacturing and processing industries.
Principles of Pneumatic Conveying
The core principle of pneumatic conveying is the use of air or gas to transport bulk materials through a pipeline system. In intelligent centralized systems, this process is enhanced with advanced control mechanisms and monitoring capabilities. The system typically operates by drawing material from a storage hopper or silo and transporting it to a destination point, such as a processing unit or storage area. The intelligent features may include real-time monitoring of flow rates, pressure, and material levels, as well as automated adjustments to optimize performance and prevent system failures. This integration of traditional pneumatic conveying with smart technology enables more precise control and reduces downtime, making the system highly efficient for various material types.
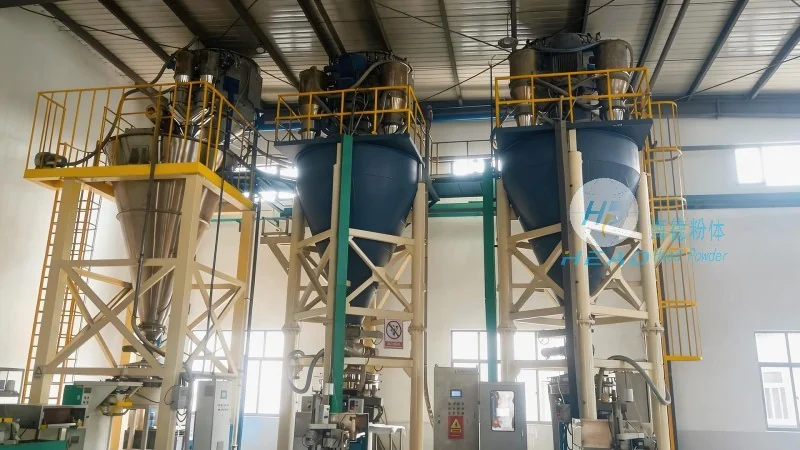
Key Working Scenarios and Applications
Intelligent centralized material pneumatic conveying systems are widely used in several industrial sectors, each benefiting from the system’s ability to handle different materials with precision and reliability. One common application is in the pharmaceutical and food processing industries, where hygiene, contamination control, and product purity are critical. The systems can be designed to meet stringent sanitary standards, ensuring that materials are transported without cross-contamination. Another significant application is in the chemical and petrochemical industries, where handling abrasive or corrosive materials requires robust and durable equipment. The intelligent features allow for real-time monitoring of material properties and system conditions, helping to prevent equipment damage and ensure safe operation.
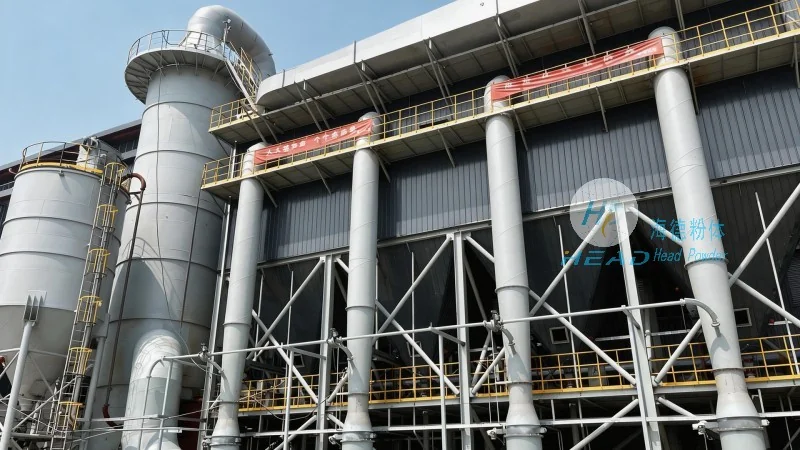
Advantages in Industrial Operations
Implementing intelligent centralized material pneumatic conveying systems offers several key advantages that contribute to improved operational efficiency and cost savings. Firstly, the centralized design reduces the need for multiple individual conveying lines, simplifying the overall system layout and reducing installation and maintenance costs. The intelligent control systems enable automated operation, minimizing the need for manual intervention and reducing labor costs. Additionally, the real-time monitoring capabilities provide early detection of system issues, allowing for proactive maintenance and reducing unexpected downtime. This leads to increased productivity and lower operational costs over the system’s lifecycle. Furthermore, the systems are designed to handle a wide range of materials, from fine powders to bulk solids, making them versatile for various industrial applications.
Conclusion and Future Outlook
Intelligent centralized material pneumatic conveying systems, as developed by Shandong HeadPowder Engineering Co., Ltd., represent a significant advancement in material handling technology. By combining traditional pneumatic conveying principles with modern intelligent control systems, these solutions enhance efficiency, safety, and operational control in industrial settings. The systems are particularly valuable in industries where material transport requires precision, reliability, and minimal human intervention. As technology continues to evolve, these systems are likely to become even more sophisticated, integrating with other industrial automation systems to create fully integrated material handling solutions. For industries seeking to optimize their material transport processes, intelligent centralized pneumatic conveying systems offer a robust and efficient solution.