

Principle and Working Scene Characteristics of Sodium Carbonate Powder Conveying Line
Sodium carbonate, commonly known as soda ash, is a widely used chemical in various industrial processes. The efficient and reliable transportation of sodium carbonate powder is crucial for maintaining production efficiency and ensuring product quality. This article explores the principle and working scene characteristics of a specialized powder conveying line designed for sodium carbonate, highlighting its technical advantages and practical applications.
The Core Principle of the Conveying System
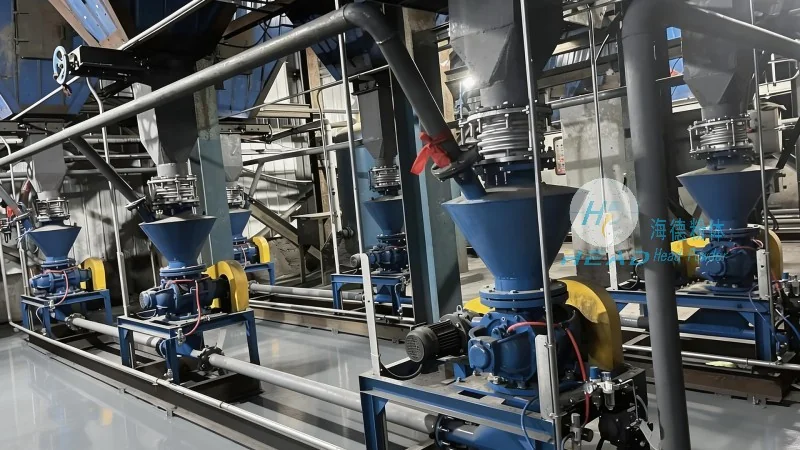
The sodium carbonate powder conveying line operates on the principle of pneumatic or mechanical conveying, depending on the specific design and application requirements. For headpowder, a leading manufacturer in the field, the system typically integrates advanced components such as rotary valves, airlocks, and flexible hoses or pipes to ensure a continuous and controlled flow of the powder. The core mechanism involves the creation of a pressure differential that propels the powder particles through the conveying line, minimizing dust generation and optimizing material handling efficiency.
Key Working Scene Characteristics
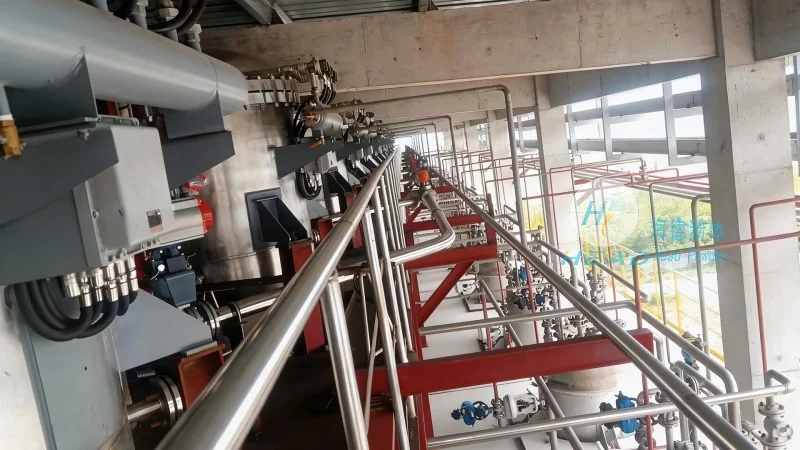
The working scene characteristics of the sodium carbonate powder conveying line are tailored to meet the demands of industrial environments where sodium carbonate is processed or used. These characteristics include high conveying capacity, low energy consumption, and the ability to handle varying particle sizes and moisture levels. The system is designed to operate in both indoor and outdoor settings, adapting to different production scales from small-scale laboratory applications to large-scale industrial manufacturing. Additionally, the conveying line is equipped with safety features and maintenance-friendly components, ensuring long-term reliability and minimal downtime.
Company Overview and Technical Expertise
Headpowder, or Shandong HeadPowder Engineering Co., Ltd., is a reputable company based in Shandong, China, specializing in the design, manufacturing, and installation of advanced powder handling systems. With years of experience in the chemical and material processing industries, the company has developed a deep understanding of the unique challenges associated with transporting sodium carbonate and other fine powders. HeadPowder's technical team leverages cutting-edge engineering solutions and rigorous quality control measures to deliver customized conveying solutions that meet the specific needs of each client.
Application Advantages and Industry Standards
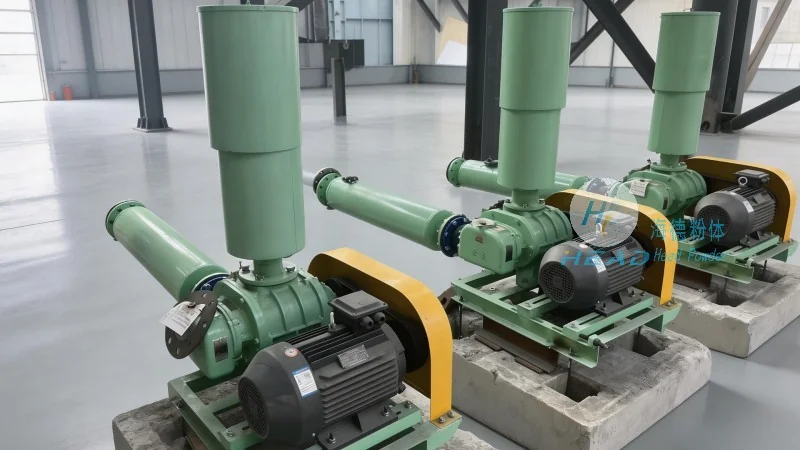
The sodium carbonate powder conveying line offers several advantages in industrial applications, including improved safety by reducing manual handling of powders, enhanced product purity through minimized contamination, and increased operational efficiency through automated control systems. The system adheres to international industry standards for powder handling, ensuring compliance with safety regulations and environmental requirements. Whether used in chemical manufacturing, food processing, or other sectors that rely on sodium carbonate, the conveying line provides a robust and reliable solution for material transport, contributing to overall process optimization and cost reduction.