

Principle and Working Scene Characteristics of Continuous Bulk Material Feeding and Conveying System
Continuous bulk material feeding and conveying systems represent a critical advancement in material handling technology, designed to address the challenges of efficient, reliable, and continuous transfer of powders and granules in industrial settings. These systems are engineered to replace traditional batch-based methods, offering significant improvements in productivity, safety, and operational consistency. The core principle revolves around the seamless integration of feeding mechanisms, conveying components, and control systems to ensure a steady flow of material from source to destination.
Working Principle of the System
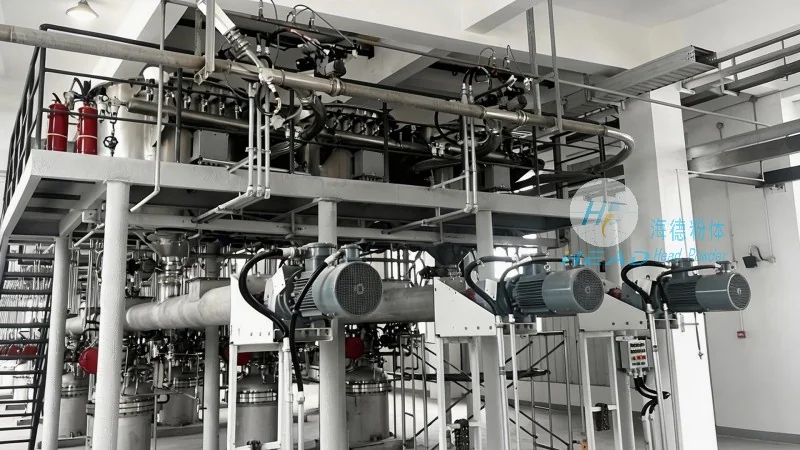
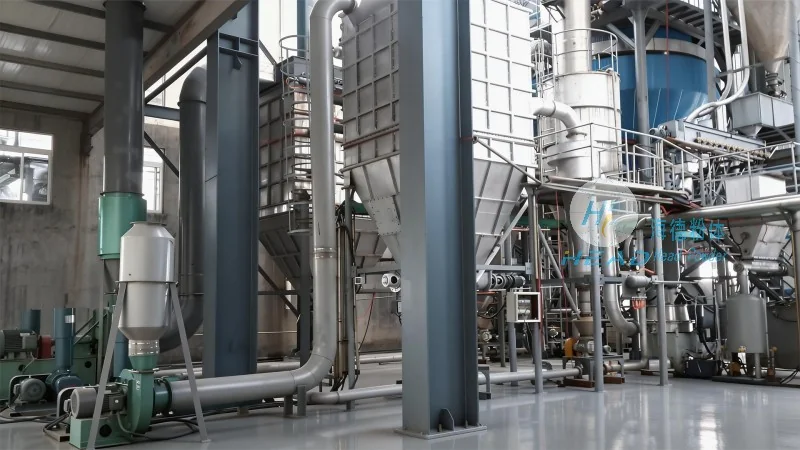
The fundamental operation of a continuous bulk material feeding and conveying system is based on the principle of consistent material movement. At its heart, the system typically comprises a feeding hopper that stores the bulk material, a feeding device (such as a screw feeder or rotary valve) that regulates the flow rate, and a conveying component (like a screw conveyor, pneumatic conveyor, or belt conveyor) that transports the material to the desired location. The feeding device ensures that material is discharged at a controlled rate, preventing overloading or underflow, while the conveying component moves the material through the system with minimal interruption. Control systems, often integrated with sensors and automation, monitor parameters such as flow rate, pressure, and level, adjusting the operation in real-time to maintain optimal performance. This closed-loop control ensures that the system operates efficiently, adapting to variations in material properties or process demands without manual intervention.
Key Working Scene Characteristics
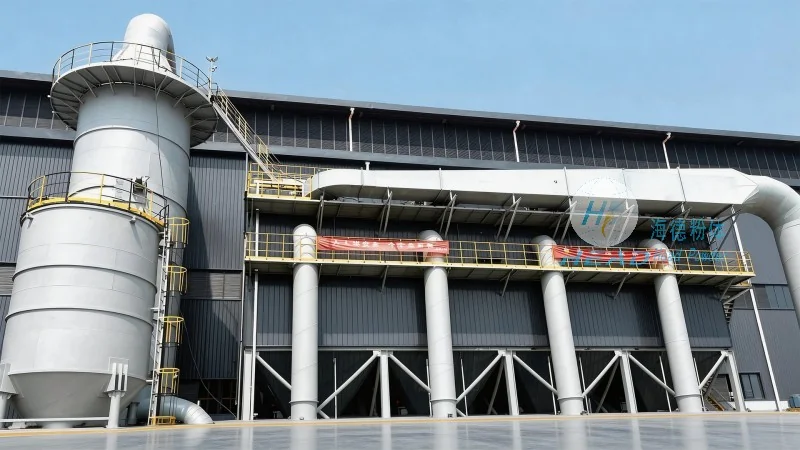
The application of continuous bulk material feeding and conveying systems spans a wide range of industrial sectors, each with distinct requirements and operational characteristics. In the chemical industry, for instance, these systems are essential for handling reactive powders and granules, where precise control over material flow is crucial to prevent contamination or accidents. The systems are designed to maintain a consistent flow rate, minimizing the risk of dust generation and ensuring compliance with safety regulations. In the pharmaceutical sector, where product purity and sterility are paramount, the equipment is constructed from materials that are easy to clean and sterilize, often featuring sealed components to prevent cross-contamination. The food processing industry also benefits from these systems, as they can handle a variety of food-grade powders and granules, with features like sanitary design and hygienic materials to meet regulatory standards. Additionally, in the mining and minerals processing industries, the systems are used to transport raw materials from storage to processing units, where high capacity and durability are required to withstand harsh operating conditions. The versatility of these systems allows them to adapt to different working environments, from indoor processing facilities to outdoor storage and transfer operations.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
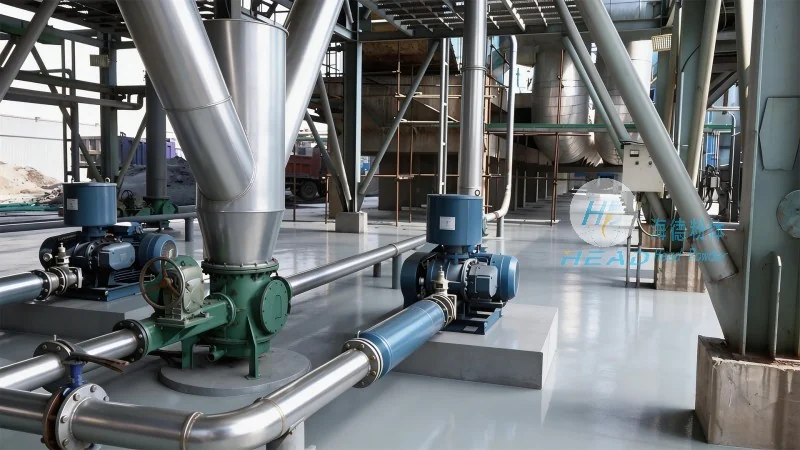
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of specialized engineering solutions for bulk material handling. With a focus on innovation and customer-centric design, the company has developed a range of continuous feeding and conveying systems tailored to meet the diverse needs of industrial clients. HeadPowder's expertise lies in the integration of advanced technologies, such as automated control systems, material flow sensors, and durable construction materials, to deliver reliable and efficient solutions. The company's facilities are located in Shandong, China, where it leverages local manufacturing capabilities and industry knowledge to produce high-quality equipment. By combining technical expertise with practical application experience, HeadPowder ensures that its systems not only meet but exceed industry standards, providing long-term value to its customers. The company's commitment to quality and customer satisfaction has established it as a trusted partner in the bulk material handling sector, serving clients across various industries with tailored solutions that enhance operational efficiency and safety.