

Inert Dust-Free Powder Conveying System: Principles and Application Scenario Features
For industries that require precise control of powder materials, especially in environments where dust contamination is a critical concern, inert dust-free powder conveying systems offer a reliable solution. These systems are designed to transport powders without exposing them to external contaminants, ensuring product purity and operational safety. The core principle behind such systems involves creating a sealed environment where the powder is conveyed under controlled conditions, often using inert gases to maintain a dust-free atmosphere.
Core Principles of Dust-Free Powder Conveying
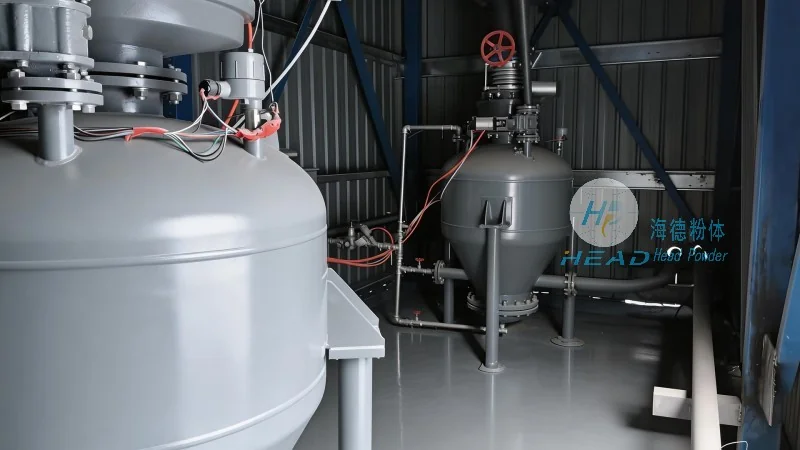
The fundamental principle of inert dust-free powder conveying is to isolate the powder from the external environment. This is achieved by using a closed pipeline system where the powder is transported under a slight overpressure of an inert gas, such as nitrogen or carbon dioxide. The inert gas not only prevents external air from entering the system but also helps in controlling the moisture content of the powder, which is crucial for maintaining its quality. The system typically includes components like feeders, conveyors, and dust collectors, all integrated to work in a synchronized manner to ensure efficient and clean powder handling.
Key Components and Their Functions
Several key components make up an inert dust-free powder conveying system. The first is the powder feeder, which is responsible for accurately measuring and feeding the powder into the conveying line. This component ensures a consistent flow rate, which is vital for maintaining the system's performance and preventing blockages. Next are the conveying lines, which are usually made of materials like stainless steel or PTFE to prevent corrosion and ensure durability. The lines are equipped with valves and bends that allow for flexible routing while maintaining the sealed environment. Additionally, the system includes a dust collector that captures any fine particles that might escape, further enhancing the dust-free operation. The inert gas supply system is another critical part, as it provides the necessary gas to maintain the overpressure and protect the powder from oxidation or moisture absorption.

Application Scenarios and Industry Use Cases
Inert dust-free powder conveying systems are widely used across various industries where powder handling is essential. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients, ensuring that the final products meet stringent purity standards. The food industry also relies on such systems for handling ingredients like flour, sugar, and spices, where contamination can affect product quality and safety. The chemical industry uses them for transporting reactive powders, preventing unwanted reactions with atmospheric elements. Additionally, in the cosmetics industry, these systems are employed to convey raw materials like pigments and powders, maintaining the color and texture integrity of the final products. Each application scenario requires specific adjustments to the system, such as varying the inert gas flow rate or modifying the conveyor speed, to suit the unique properties of the powder being handled.
Advantages of Inert Dust-Free Powder Conveying
Implementing an inert dust-free powder conveying system offers several advantages over traditional open conveying methods. The primary benefit is the enhanced product purity, as the sealed environment prevents contamination from dust, moisture, or other external factors. This is particularly important for industries where product quality directly impacts consumer health or regulatory compliance. Another advantage is improved operational safety, as the system reduces the risk of dust explosions by maintaining an inert atmosphere. The sealed design also minimizes the risk of powder loss and cross-contamination between different batches of materials. Furthermore, these systems are more energy-efficient compared to traditional methods, as they use less power to maintain the overpressure and control the flow. The long-term cost savings from reduced maintenance and product waste also make them a cost-effective solution for businesses.
Customization and Scalability
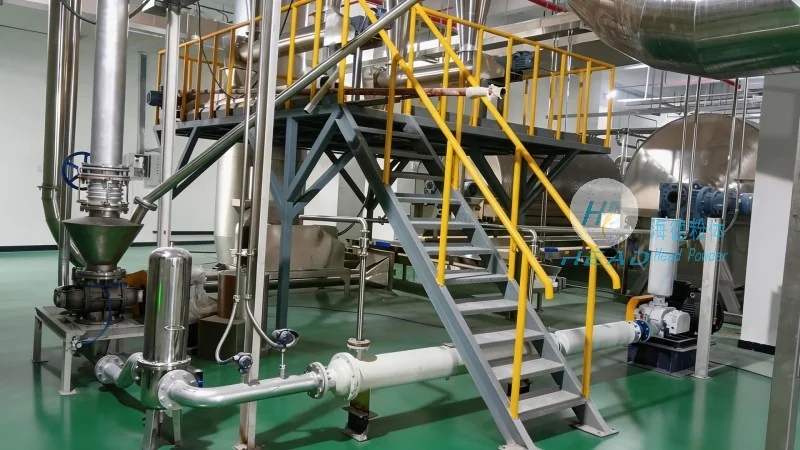
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized inert dust-free powder conveying systems to meet the specific needs of different industries. The company, commonly known as headpowder, offers a range of solutions tailored to various powder types and application requirements. Their systems can be scaled from small laboratory setups to large industrial production lines, ensuring flexibility and adaptability. The company's engineers work closely with clients to understand their operational challenges and provide tailored solutions. For example, if a client needs to handle a highly abrasive powder, the system can be equipped with special wear-resistant materials to extend its lifespan. Similarly, for powders that are sensitive to moisture, the system can be designed with additional drying components to maintain the powder's quality. This level of customization ensures that the system not only meets the current needs of the client but also accommodates future growth and changes in production.
Conclusion and Contact Information
In summary, inert dust-free powder conveying systems are essential for industries that require high-purity and safe powder handling. The principles and components of these systems work together to create a sealed environment that protects the powder from contamination and ensures efficient operation. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can access reliable and customized solutions that meet their specific requirements. By investing in such systems, companies not only improve their product quality and operational safety but also achieve long-term cost savings and operational efficiency. For more information about inert dust-free powder conveying systems, contact Shandong HeadPowder Engineering Co., Ltd., located in Shandong, China.