

Principle and Working Scene Characteristics of Grain Pneumatic Conveying Machines
Grain pneumatic conveying machines are essential equipment in the agricultural and food processing industries, designed to efficiently transport bulk materials like grains, cereals, and other dry bulk commodities. These systems utilize air as the primary medium to move materials from one location to another, offering a flexible and efficient solution for various industrial applications. The core principle behind pneumatic conveying involves creating a pressure differential or using vacuum to draw or push materials through a pipeline, ensuring smooth and continuous material handling without the need for mechanical components like belts or buckets.
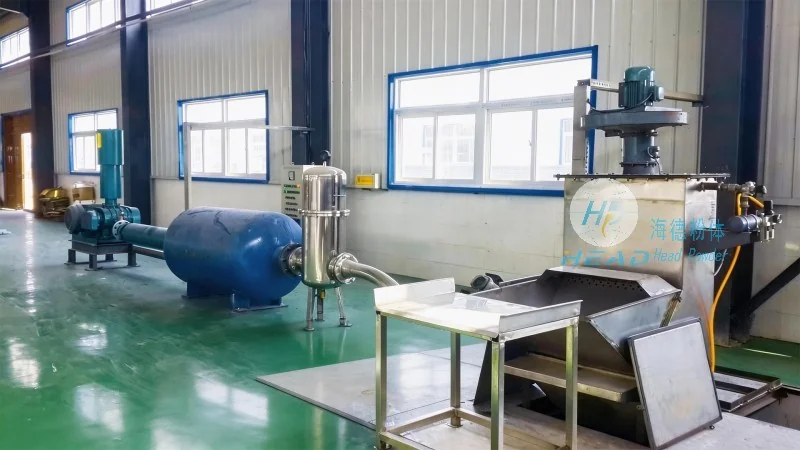
Working Principle of Pneumatic Conveying Technology
The operation of grain pneumatic conveying machines is based on the fundamental physics of fluid dynamics and material transport. There are two main types of pneumatic conveying systems: pressure and vacuum. In pressure systems, compressed air is introduced into the material hopper, creating a pressure that forces the material through the pipeline. Conversely, vacuum systems use a vacuum pump to create a negative pressure that draws the material into the pipeline. The choice between pressure and vacuum depends on the distance, height, and material characteristics. For example, pressure systems are often used for short to medium distances (typically up to 100 meters) and when handling abrasive or heavy materials like wheat or corn, as they can maintain higher air flow rates. Vacuum systems, on the other hand, are suitable for longer distances (up to several hundred meters) and when dealing with lighter or more delicate products such as flour or fine powders, as they can effectively transport materials without causing excessive wear on the pipeline.
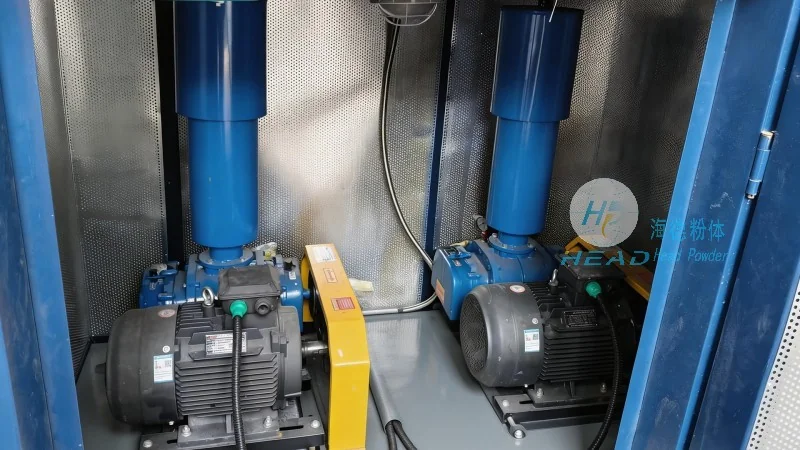
Key Working Scene Characteristics
The application of grain pneumatic conveying machines is characterized by several distinct features that make them ideal for specific industrial environments. Firstly, these systems provide a hygienic and dust-free operation, which is crucial in food processing facilities where contamination control is paramount. The enclosed pipeline design prevents dust from entering the workspace, maintaining a clean and safe environment for both personnel and products. Secondly, pneumatic conveyors offer high flexibility in layout, allowing for vertical, horizontal, or inclined transport without the need for complex mechanical adjustments. This adaptability is particularly beneficial in facilities with limited space or irregular layouts, such as small-scale grain mills or large-scale agricultural processing plants. Thirdly, the systems are capable of handling a wide range of material types, from fine powders to large granules, with adjustable air flow and pressure settings to optimize performance. This versatility makes them suitable for diverse applications, including grain storage, milling, and packaging operations. For instance, in a grain storage facility, pneumatic conveyors can efficiently move harvested grains from silos to processing lines, while in a flour mill, they can transport fine flour from grinding machines to packaging units. Additionally, the systems are designed to minimize material degradation, ensuring that the quality of the grains is preserved throughout the transport process.
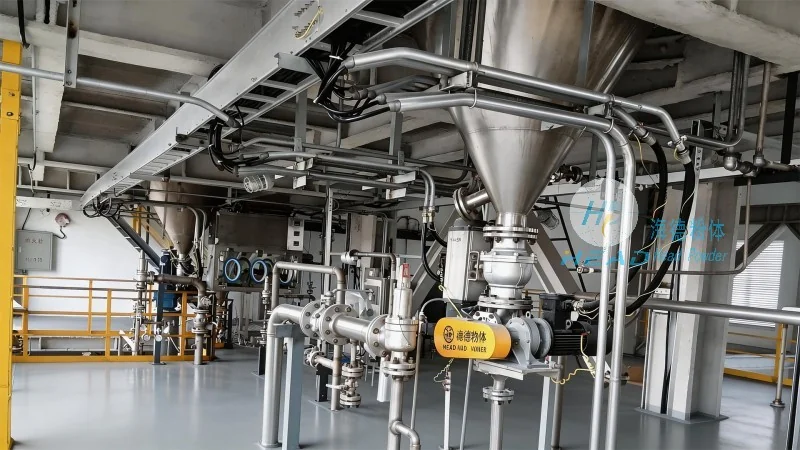
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of bulk material handling equipment, specializes in the design, development, and production of advanced grain pneumatic conveying systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for industries requiring reliable and efficient material transport solutions. HeadPowder's products are engineered to meet international standards and are tailored to the specific needs of each client, ensuring optimal performance and durability. The company's headquarters is located in Shandong, China, where it leverages local manufacturing capabilities and expertise to deliver high-quality equipment to global markets. HeadPowder's team of engineers and technicians continuously researches and develops new technologies to improve the efficiency and sustainability of pneumatic conveying systems, staying ahead of industry trends and customer demands. By focusing on customer satisfaction and product excellence, HeadPowder has built a reputation for delivering solutions that enhance operational efficiency and reduce costs for its clients.