

Principle and Working Scene Characteristics of Carbon Black Pneumatic Conveying Machines
Carbon black is a vital material across numerous industrial sectors, and efficient handling of this fine powder is crucial for maintaining production efficiency and product quality. Pneumatic conveying systems, specifically designed for carbon black, offer a reliable method for transporting these particles from production sites to processing or storage areas. This article delves into the fundamental principles behind carbon black pneumatic conveying machines and highlights the key characteristics of their operational environments.
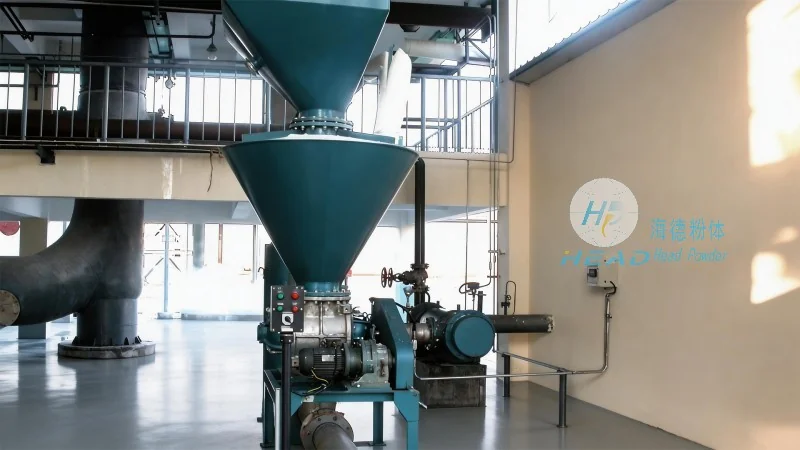
Principle of Carbon Black Pneumatic Conveying Machines
At the core of carbon black pneumatic conveying is the utilization of air as a medium to transport solid particles. The system typically comprises a blower or air compressor that generates high-pressure airflow, which then moves the carbon black particles through a network of pipes. The process can be categorized into two main types: dilute phase and dense phase conveying. Dilute phase systems rely on low-pressure air to move particles at relatively high velocities, suitable for short to medium distances. Dense phase systems, conversely, use higher pressure and lower air velocity to transport particles in a more concentrated state, ideal for longer distances or when handling delicate materials. The choice between these systems depends on factors such as the distance to be covered, the required flow rate, and the characteristics of the carbon black being conveyed.
The operation of a carbon black pneumatic conveying machine begins with the feeding of carbon black into the system. A feeder, often a rotary valve or a screw feeder, ensures a consistent flow of material into the conveying line. The air from the blower is introduced at the inlet of the pipe, creating a flow that lifts and transports the carbon black particles. The system may include features such as in-line mixers or separators to control the concentration of particles in the air stream and prevent blockages. At the receiving end, a cyclone or bag filter separates the carbon black from the air, allowing the powder to be collected in a container or silo. The exhaust air is then filtered to meet environmental regulations before being released back into the environment.
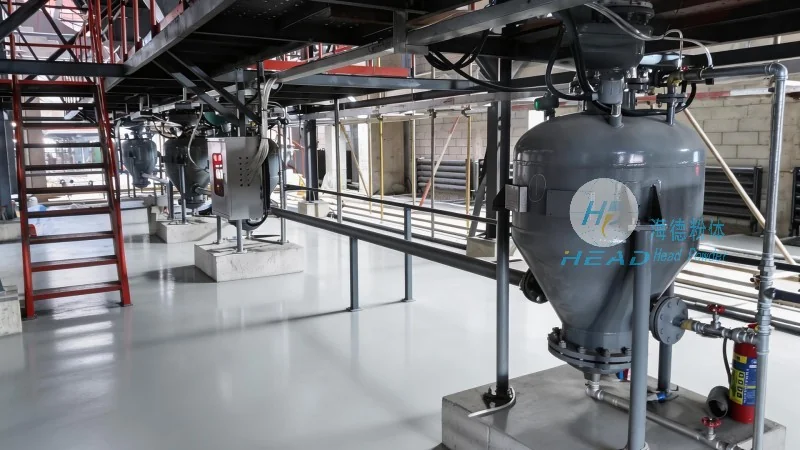
Working Scene Characteristics of Carbon Black Pneumatic Conveying Machines
The operational environment of carbon black pneumatic conveying machines is tailored to the specific needs of the industry, particularly in the production and processing of carbon black. These systems are commonly found in industrial settings such as carbon black manufacturing plants, where they are used to transport raw materials or finished products between different stages of production. The working scene characteristics include factors like the scale of operation, the type of carbon black (e.g., furnace black, channel black), and the required throughput. For instance, in large-scale production facilities, the conveying systems may need to handle high volumes of carbon black, necessitating robust and high-capacity equipment. The environment may also involve exposure to dust and fumes, requiring the use of dust collection systems and proper ventilation to ensure worker safety and compliance with environmental standards.
Another key characteristic is the need for flexibility in the conveying process. Carbon black is often used in various applications, and the conveying system may need to adapt to different particle sizes and flow rates. This flexibility is achieved through adjustable components such as variable speed blowers, variable feed rates, and modular piping systems. The working scene may also involve integration with other industrial equipment, such as mixers, extruders, or coating machines, where the carbon black is used as an additive. In such cases, the conveying system must ensure a consistent and controlled delivery of the material to maintain the quality of the final product.
Application Scenarios and Operational Advantages
Carbon black pneumatic conveying machines are employed in a wide range of applications across different industries. In the rubber and plastic manufacturing sectors, carbon black is used as a pigment and reinforcing agent, and the conveying systems ensure a uniform distribution of the material in the production process. The systems are also used in the production of inks, paints, and coatings, where the quality of the carbon black is critical. Additionally, in the battery and electronics industries, carbon black is used as a conductive material, and the precise control of its delivery is essential for product performance.
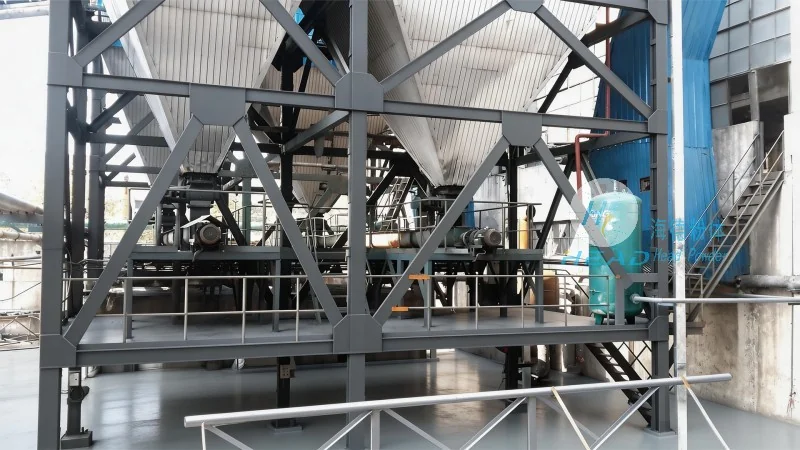
The operational advantages of carbon black pneumatic conveying machines include their ability to handle fine powders without the need for mechanical components that could cause wear or contamination. Unlike belt or screw conveyors, pneumatic systems do not have moving parts in contact with the material, reducing the risk of particle degradation and ensuring a cleaner process. The systems also offer flexibility in layout, as the pipes can be arranged in various configurations to suit the space constraints of the facility. Furthermore, pneumatic conveying can be integrated with other process control systems, allowing for real-time monitoring and adjustment of the conveying parameters to optimize performance and minimize downtime.
Supplier Information: Shandong HeadPowder Engineering Co., Ltd.
For those seeking reliable and efficient carbon black pneumatic conveying solutions, Shandong HeadPowder Engineering Co., Ltd. is a leading provider based in China. The company specializes in the design, manufacturing, and installation of pneumatic conveying systems tailored to the specific needs of carbon black handling. With years of experience in the industry, HeadPowder has developed a reputation for delivering high-quality equipment that meets the stringent requirements of modern industrial applications. The company's products are engineered to ensure durability, efficiency, and compliance with environmental regulations, making them a trusted choice for businesses in the carbon black sector. HeadPowder's commitment to customer satisfaction and technical excellence has established it as a key player in the market, providing comprehensive solutions for the transportation and processing of carbon black materials.