

Principle and Working Scene Characteristics of Gravity Dust Removal Pneumatic Conveying Equipment
Gravity dust removal pneumatic conveying equipment is a critical component in industrial material handling systems, designed to efficiently transport fine powders and dust while simultaneously ensuring air filtration and particle separation. This technology combines the principles of gravity separation with pneumatic conveying to achieve a dual purpose: material transport and air purification. The equipment is widely used in various industrial sectors where the handling of dry, fine materials is essential, such as in chemical, pharmaceutical, food processing, and mining industries.
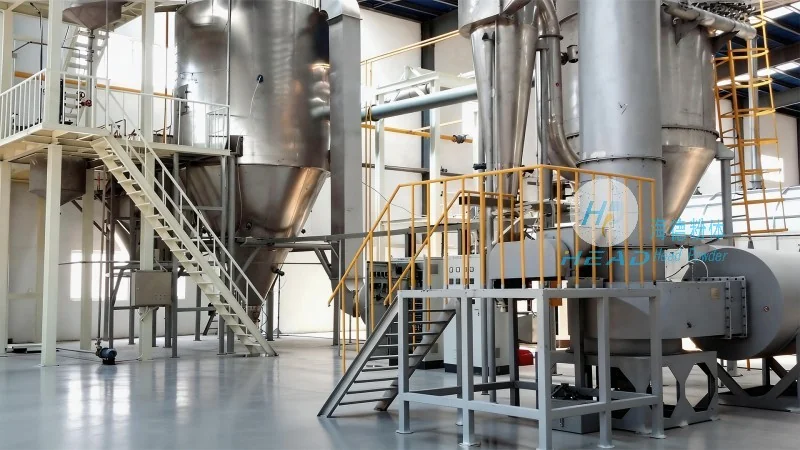
Principle of Gravity Dust Removal Pneumatic Conveying
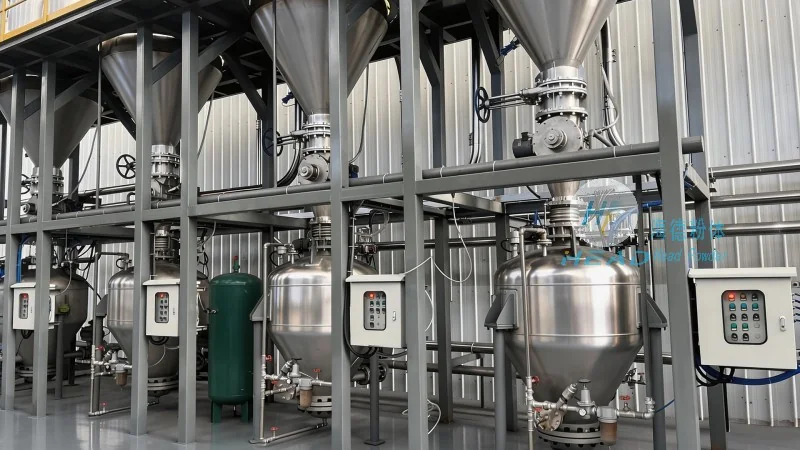
The core principle of this equipment lies in the utilization of gravity and air flow to separate particles based on their density and size. As air is introduced into the conveying system, it creates a low-pressure environment that draws the material into the pipeline. Simultaneously, gravity plays a role in the separation process, where larger or heavier particles settle due to gravitational force, while finer dust particles remain suspended in the air stream. The system typically includes a hopper for material storage, a conveying line, and a dust collection unit. The hopper is equipped with a feeder that controls the material flow into the pipeline. The conveying line is designed with appropriate bends and fittings to maintain the air flow and prevent blockages. The dust collection unit, often integrated with a filter or cyclone separator, captures the fine dust particles from the air stream, ensuring clean air is released back into the environment.

Working Scene Characteristics and Applications
Gravity dust removal pneumatic conveying equipment is particularly suited for applications where the material being handled is fine, dry, and potentially hazardous. The working scene characteristics include high efficiency in material transport over long distances, minimal material loss, and effective air filtration. In industrial settings, this equipment is commonly used in scenarios such as transporting raw materials to processing units, moving finished products from production lines to storage areas, and handling waste materials for recycling or disposal. The equipment's ability to handle fine powders without clogging or degradation makes it ideal for industries that require precise material control, such as pharmaceutical manufacturing, where product purity is paramount. Additionally, in the food processing industry, the equipment ensures that the transported materials remain free from contamination, maintaining hygiene standards. The working scene also includes environments where space is limited, as the equipment can be installed in compact areas without compromising performance. The integration of gravity separation with pneumatic conveying allows for a more energy-efficient operation compared to traditional methods, reducing the overall operational costs for industrial facilities.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of advanced material handling equipment, including gravity dust removal pneumatic conveying systems. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the industrial sector, providing customized solutions tailored to the specific needs of clients. HeadPowder's headquarters is located in Shandong, China, where the company operates a state-of-the-art manufacturing facility equipped with the latest technology and skilled workforce. The company adheres to international standards in product design, production, and testing, ensuring that each piece of equipment meets the highest quality and performance criteria. HeadPowder's commitment to customer satisfaction and technological advancement has enabled it to serve a diverse range of industries, from small-scale enterprises to large multinational corporations. The company's products are known for their durability, efficiency, and reliability, making them a preferred choice for industrial applications worldwide.