

Principle and Working Scene Characteristics of Phosphate Fertilizer Powder Pneumatic Conveying
Phosphate fertilizer powder pneumatic conveying is a critical technology in the handling and transportation of bulk solid materials, particularly in industrial settings where efficient and safe movement of phosphate-based powders is essential. This method leverages the power of air to transport dry powders like phosphate fertilizer through a pipeline system, offering advantages such as reduced equipment wear, improved safety, and enhanced process control compared to traditional mechanical conveying methods.
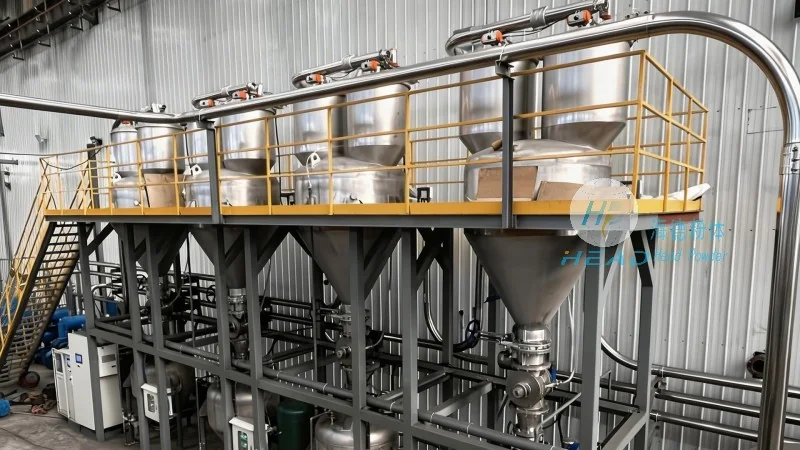
The core principle of pneumatic conveying for phosphate fertilizer powder involves creating a flow of air within a pipeline that transports the powder particles. This can be achieved through either pressure (positive pressure) or vacuum (negative pressure) systems. In positive pressure systems, a blower or compressor generates high-pressure air that pushes the powder through the pipeline, while negative pressure systems use a vacuum pump to draw the powder into the system. The design of the conveying system, including the type of air nozzle, pipeline layout, and particle characteristics, plays a crucial role in determining the efficiency and effectiveness of the conveying process.

One of the key working scene characteristics of phosphate fertilizer powder pneumatic conveying is its adaptability to various industrial environments. For instance, in mining and processing facilities, this technology is used to transport raw phosphate ore or processed phosphate powders from crushers to storage silos or processing units. The ability to handle abrasive and corrosive materials, such as phosphate minerals, makes it suitable for heavy-duty applications where mechanical conveyors might experience excessive wear or failure. Additionally, in agricultural and fertilizer production plants, pneumatic conveying is employed to move phosphate fertilizer from storage tanks to mixing and packaging equipment, ensuring a continuous and controlled flow of material.
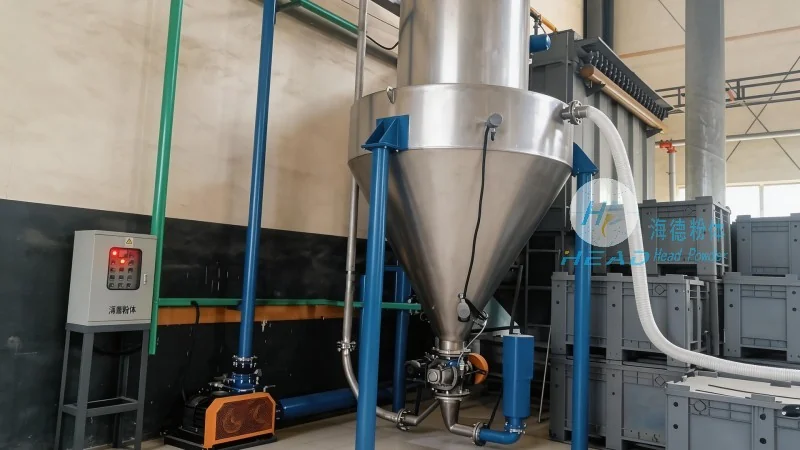
Another important aspect is the scalability of pneumatic conveying systems for phosphate fertilizer powder. Whether for small-scale laboratory applications or large-scale industrial operations, the technology can be customized to handle varying capacities and particle sizes. This flexibility allows companies to optimize their material handling processes, reducing downtime and operational costs. Furthermore, the system's ability to integrate with other industrial processes, such as dust collection and material drying, enhances overall plant efficiency and safety.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying solutions for phosphate fertilizer and other bulk solid materials. With a focus on innovation and customer-centric solutions, HeadPowder leverages years of industry experience to provide tailored systems that meet the specific needs of clients in the fertilizer, mining, and chemical sectors. The company's headquarters is located in Shandong, China, where it serves a global clientele by delivering high-quality, reliable, and efficient conveying systems that enhance operational performance and safety.
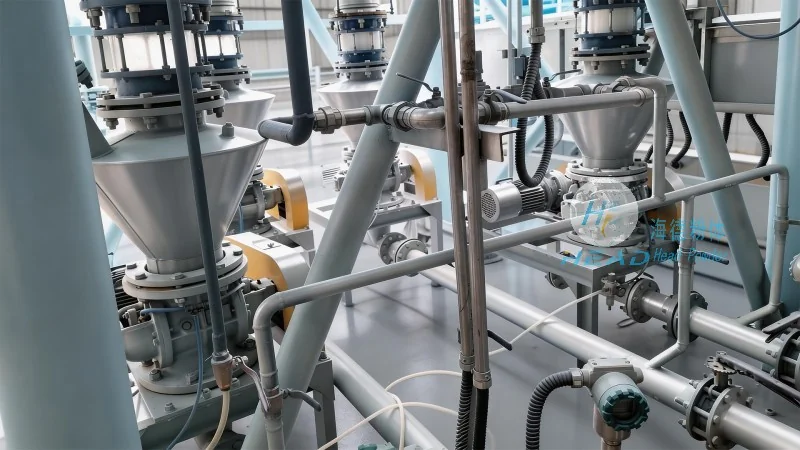
By understanding the principles and working scene characteristics of phosphate fertilizer powder pneumatic conveying, industries can make informed decisions about material handling strategies. The technology's ability to handle challenging materials like phosphate fertilizer, combined with its adaptability to diverse industrial applications, makes it a preferred choice for companies seeking to improve efficiency, reduce costs, and ensure safe operation in their material handling processes. As the demand for phosphate fertilizers continues to grow, the role of advanced pneumatic conveying systems becomes increasingly vital in supporting sustainable and efficient agricultural practices worldwide.