

Working Principle and Features of Potassium Hydroxide Powder Conveyors
For industrial applications involving the handling of potassium hydroxide (KOH) powder, specialized equipment is essential to ensure efficient and safe material transport. The potassium hydroxide powder conveyor, manufactured by Shandong HeadPowder Engineering Co., Ltd., is a critical component in processes where precise and reliable powder handling is required. This article explores the working principle and key features of such conveyors, highlighting their importance in industrial operations.
Working Principle of Potassium Hydroxide Powder Conveyors
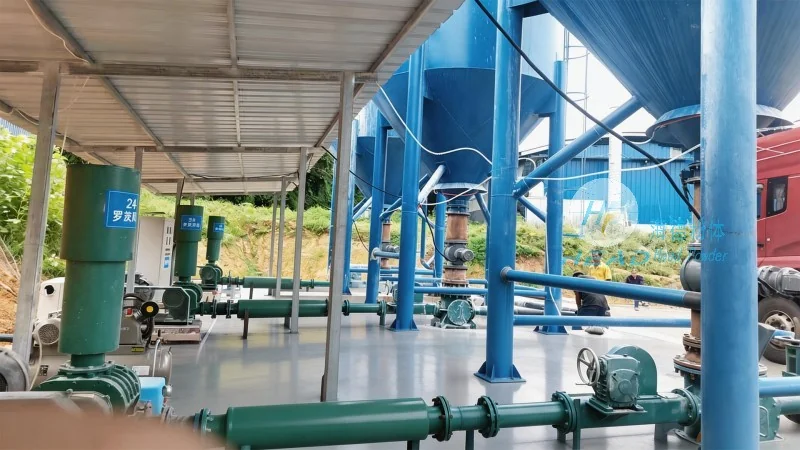
The operation of a potassium hydroxide powder conveyor typically involves a combination of mechanical components designed to move dry powder materials. The system often includes a hopper or feed bin where the potassium hydroxide powder is stored, followed by a conveyor mechanism such as a screw conveyor, belt conveyor, or pneumatic system. The conveyor transports the powder from the storage area to the processing or packaging stage. The working principle may vary based on the specific design, but the core function remains consistent: to move the powder in a controlled manner, minimizing dust generation and ensuring uniform flow. The conveyor system is equipped with components like feeders, control valves, and sometimes dust collection systems to maintain operational efficiency and safety. The design aims to handle the hygroscopic nature of potassium hydroxide, preventing clumping and ensuring smooth material movement.
Key Features of Potassium Hydroxide Powder Conveyors
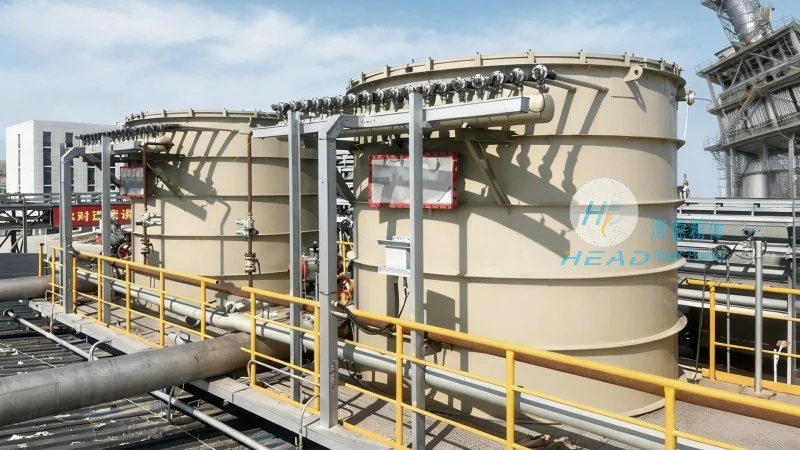
Shandong HeadPowder Engineering Co., Ltd. offers conveyors with several notable features tailored to the demands of potassium hydroxide handling. These features enhance performance, safety, and longevity. First, the conveyors are constructed from materials resistant to corrosion and chemical exposure, as potassium hydroxide is a strong base that can degrade certain metals. Stainless steel or specialized alloys are commonly used for the conveyor components to ensure durability. Second, the system incorporates dust control measures, such as sealed enclosures and filtration systems, to prevent dust dispersion and protect both the environment and personnel. Third, the conveyors are equipped with adjustable speed controls and flow rate mechanisms, allowing operators to regulate the amount of powder being transported based on production needs. This flexibility is crucial for maintaining consistent output and preventing overloading. Additionally, the design includes safety features like emergency stop buttons and overload protection to minimize risks during operation. The conveyors are also designed for easy maintenance, with accessible components that can be cleaned or replaced without extensive downtime.
Applications and Benefits in Industrial Settings
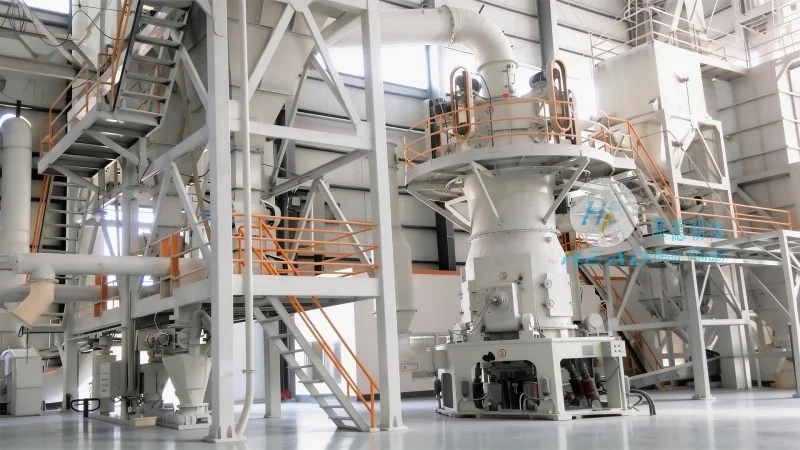
Potassium hydroxide powder conveyors are widely used in various industrial sectors, including chemical manufacturing, food processing, and pharmaceutical production. In chemical plants, these conveyors facilitate the transport of KOH from storage to reactors or processing units, ensuring a steady supply of material for production. In food processing, the conveyors help move KOH for use in food additives or cleaning applications, maintaining hygiene and safety standards. The benefits of using specialized conveyors include improved efficiency, reduced material loss, and enhanced safety. By minimizing dust and controlling material flow, the conveyors contribute to a cleaner and more controlled working environment. Furthermore, the reliability of these systems reduces downtime and maintenance costs, making them a cost-effective solution for long-term industrial operations.
Conclusion and Company Information
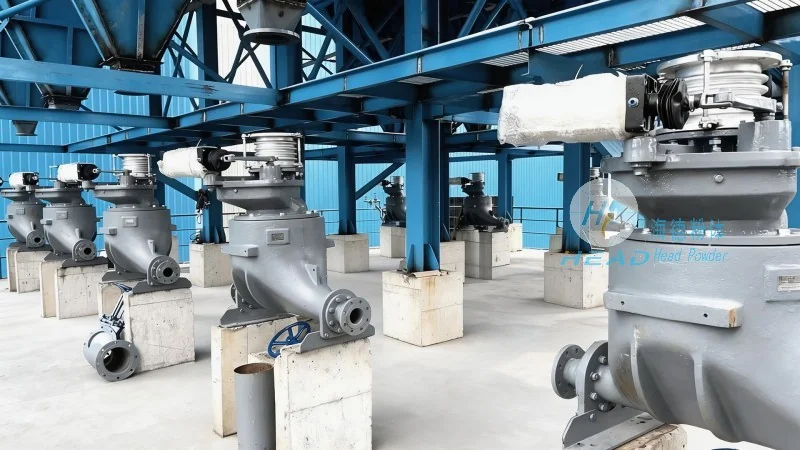
Shandong HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of high-quality potassium hydroxide powder conveyors, combining advanced engineering with practical application. The company, operating under the brand name headpowder, is based in Shandong, China, and is committed to providing reliable equipment for industrial powder handling. The conveyors offered by headpowder are engineered to meet the specific requirements of potassium hydroxide processing, ensuring optimal performance and safety. By understanding the working principle and features of these conveyors, industries can enhance their operational efficiency and maintain compliance with safety standards. For businesses seeking efficient and safe powder transport solutions, the potassium hydroxide powder conveyor from headpowder is a reliable choice.