

Working Principle and Features of Dust-Free Powder Handling Systems
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer and supplier based in Shandong, China. The company specializes in the design, development, and production of advanced dust-free powder handling systems, which are widely used in various industries such as pharmaceuticals, food processing, and chemical manufacturing. These systems are engineered to ensure the safe and efficient transfer of powders while maintaining stringent contamination control standards.
Working Principle of Dust-Free Powder Handling Systems
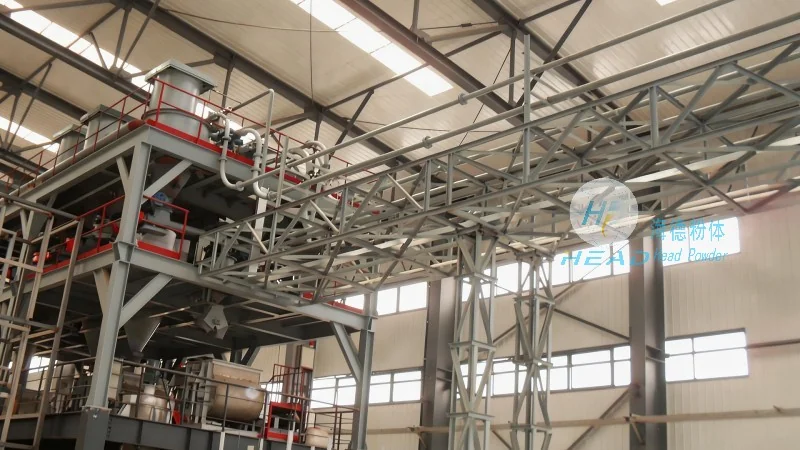
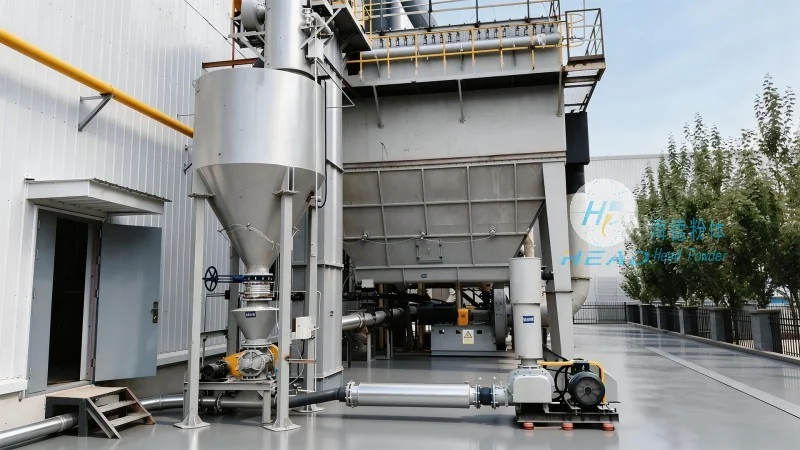
The core working principle of a dust-free powder handling system revolves around creating a sealed environment to prevent particle leakage and cross-contamination. The system typically operates by using positive pressure or negative pressure to maintain a controlled airflow within the conveying line. This airflow ensures that powders are transported through the system without coming into contact with the external atmosphere, thus minimizing the risk of dust exposure and product degradation. The process begins with the powder being loaded into a hopper or silo, where it is then drawn into the conveying pipeline by a fan or blower. The air-powder mixture travels through the pipeline, and the powder is separated from the air at the discharge point using a cyclone or filter system. This separation allows the powder to be collected in a clean container while the air is either recirculated or filtered and released back into the environment. The entire system is designed with high-quality materials and tight sealing mechanisms to maintain the integrity of the dust-free environment throughout the conveying process.
Key Features of Dust-Free Powder Handling Systems
Dust-free powder handling systems from headpowder are characterized by several key features that make them ideal for applications requiring high purity and minimal contamination. First, the systems employ advanced sealing technology to prevent any leakage of powders or dust particles. This is achieved through the use of double-flanged connections, O-ring seals, and other specialized components that ensure a tight seal even under varying pressure conditions. Second, the systems are designed for high efficiency and low energy consumption. By optimizing the airflow and conveying speed, the systems minimize the amount of air required while maximizing the throughput of powders, resulting in cost savings and reduced operational expenses. Third, the systems are highly versatile and can handle a wide range of powder types, including fine powders, granules, and bulk materials. This adaptability allows the systems to be used in various industries and for different applications without the need for significant modifications. Fourth, the systems are equipped with user-friendly control panels and monitoring systems that allow operators to easily adjust the conveying parameters and monitor the system's performance in real time. This feature enhances operational efficiency and ensures that the system operates within optimal conditions. Finally, the systems are constructed from high-quality, food-grade, or industrial-grade materials, depending on the application, to ensure durability and compliance with relevant industry standards. This ensures that the systems can withstand the rigors of continuous operation and maintain their performance over an extended period.
Applications and Benefits
The dust-free powder handling systems offered by headpowder are suitable for a wide range of applications across different industries. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision and minimal contamination, ensuring the quality and safety of the final products. In the food processing industry, the systems are used to handle food powders such as sugar, flour, and spices, maintaining the purity and freshness of the products. In the chemical industry, the systems are used to transport chemical powders, ensuring that the powders are handled safely and without exposure to the environment. The benefits of using these systems include improved product quality, reduced waste, and enhanced workplace safety. By preventing dust exposure, the systems also contribute to a healthier working environment, reducing the risk of respiratory issues and other health problems associated with dust inhalation. Additionally, the systems help in maintaining compliance with regulatory standards, such as those set by the FDA or other industry bodies, which is crucial for industries that operate under strict quality control guidelines.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides reliable and efficient dust-free powder handling systems that are designed to meet the demanding requirements of modern industries. The systems are engineered with advanced technology and high-quality materials to ensure optimal performance, durability, and safety. By understanding the working principle and key features of these systems, users can make informed decisions about their powder handling needs and choose the most suitable system for their specific applications. The company's commitment to innovation and quality ensures that its products remain at the forefront of the industry, providing customers with solutions that enhance productivity, reduce costs, and improve overall operational efficiency.