

Working Principle and Features of Slurry and Powder Conveying Systems
Slurry and powder conveying systems are essential in various industrial applications, designed to transport solid particles suspended in liquid or dry powders efficiently. Understanding the working principle and key features of such systems is crucial for selecting the right equipment for specific operational needs.
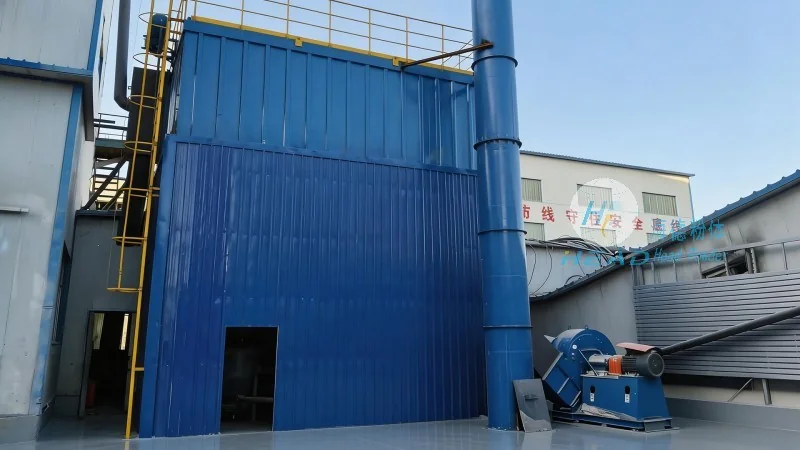
Working Principle of Slurry and Powder Conveying Systems
The core mechanism of slurry and powder conveying systems involves the movement of material through pipelines using pressure or vacuum. In pressure systems, a pump or compressor generates the necessary force to push the slurry or powder mixture through the pipeline. This method is commonly used for long-distance or high-pressure applications. Conversely, vacuum systems utilize suction to draw the material into the pipeline, which is often suitable for short distances or when handling fine powders that might be prone to dusting.
Within these systems, components like pumps, valves, and pipelines are carefully designed to handle the specific characteristics of the slurry or powder. For instance, pumps may be equipped with wear-resistant materials to withstand abrasion from solid particles, while pipelines are often lined with corrosion-resistant coatings to prevent degradation from the liquid medium. The system's control mechanisms, including flow meters and pressure sensors, ensure consistent and safe operation by monitoring key parameters in real-time.
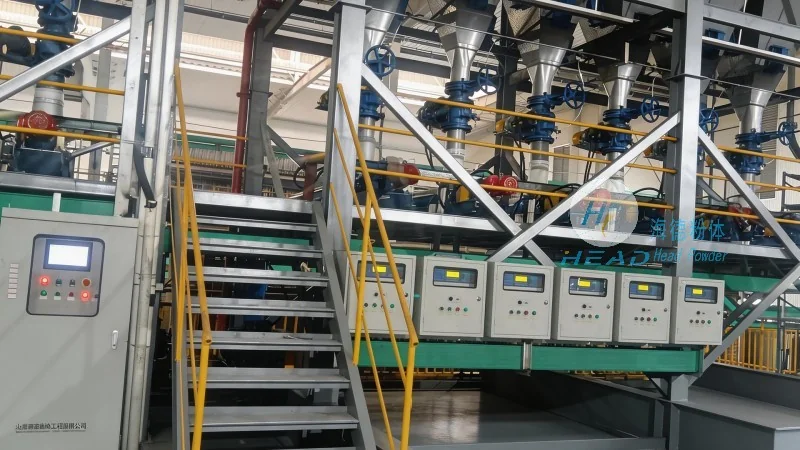
Key Features of Slurry and Powder Conveying Systems
Several critical features distinguish effective slurry and powder conveying systems. One prominent feature is the ability to handle a wide range of particle sizes and concentrations, from fine powders to coarse slurries. This versatility makes the systems adaptable to diverse industrial processes, such as mining, construction, and chemical manufacturing.
Another important feature is the system's efficiency in terms of energy consumption and operational costs. Advanced designs, including energy-efficient pumps and optimized pipeline layouts, reduce the overall power requirements while maintaining high material throughput. Additionally, the systems are engineered for minimal maintenance, with components that are easy to replace and inspect, thereby lowering downtime and operational expenses.
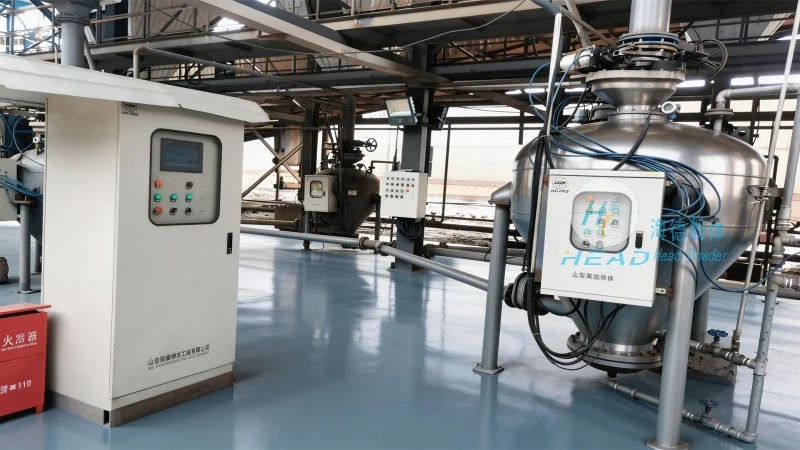
Reliability and safety are also paramount features. Modern slurry and powder conveying systems incorporate safety measures such as pressure relief valves and emergency shut-off mechanisms to prevent accidents and ensure compliance with industrial safety standards. The robust construction of the equipment, including reinforced pipelines and durable pump housings, enhances longevity and reduces the risk of leaks or failures.
Applications and Benefits in Industrial Settings
Slurry and powder conveying systems find extensive applications across multiple industries. In the mining sector, they are used to transport ore slurries from processing plants to storage facilities, ensuring smooth material flow and reducing the need for manual handling. In the construction industry, these systems efficiently deliver cement and other dry powders to job sites, improving productivity and reducing labor costs.
In the chemical and pharmaceutical industries, the systems are critical for transporting reactive or hazardous materials, as they provide a closed-loop system that minimizes exposure risks. The ability to maintain consistent material properties, such as moisture content and particle size distribution, is vital in these sectors, as it directly impacts product quality and process efficiency.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of slurry and powder conveying solutions. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the industry. HeadPowder's headquarters is located in Shandong, China, where the company operates a state-of-the-art manufacturing facility and research center.
The company specializes in designing and manufacturing customized conveying systems tailored to the unique requirements of each client. By leveraging advanced engineering techniques and extensive industry experience, HeadPowder ensures that its products meet the highest standards of performance and reliability. The company's commitment to customer satisfaction is reflected in its comprehensive after-sales support, including maintenance services and technical assistance.