

[Pulverized Bleaching Earth Pneumatic Conveying Technology: Principles, Applications, and Development Trends]
HeadPowder, a leading enterprise in the field of industrial material handling, specializes in advanced pneumatic conveying solutions tailored for the transportation of pulverized bleaching earth. This article provides an in-depth exploration of the fundamental principles underlying pneumatic conveying systems, the practical applications of such technology in various industrial settings, and the emerging trends that are shaping the future of this critical process.
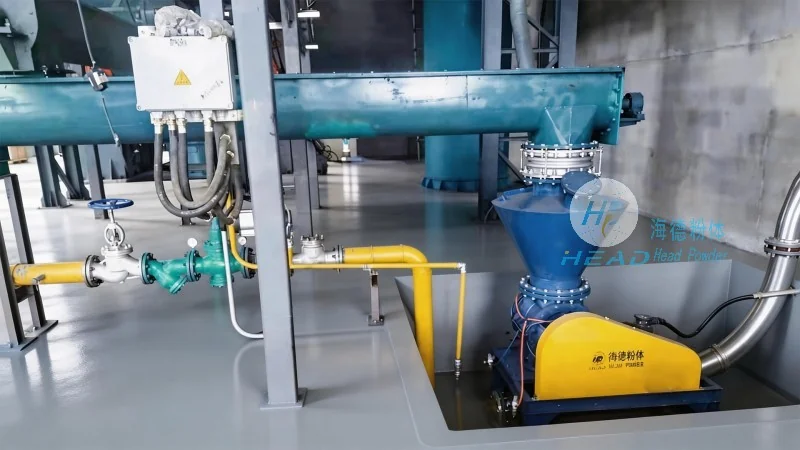
Pneumatic conveying, as a non-contact material transport method, operates by utilizing a stream of air or other gas to move particulate materials through a pipeline. In the context of pulverized bleaching earth, which is a fine powder commonly used in the oil refining and food processing industries, the efficiency and reliability of the conveying system are paramount. The core principle involves creating a pressure differential between the conveying line and the ambient environment, enabling the powder to be suspended and transported as a fluidized stream. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance costs and minimizing the risk of material contamination.
For companies like Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, the design and implementation of pneumatic conveying systems for bleaching earth require meticulous consideration of several key factors. These include the particle size distribution of the bleaching earth, which directly impacts the air velocity and pressure required for effective transport. Additionally, the moisture content and bulk density of the material influence the system's capacity and energy consumption. By addressing these variables through precise engineering, HeadPowder ensures that its pneumatic conveying solutions deliver optimal performance and durability.
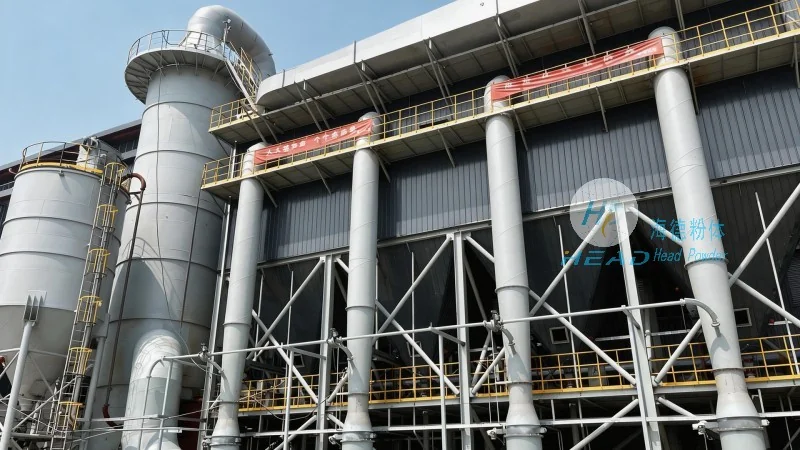
Applications of pneumatic conveying technology for bleaching earth span multiple industries. In the petroleum industry, bleaching earth is used to refine vegetable oils and animal fats, and the ability to transport this fine powder efficiently is crucial for maintaining production throughput. The food processing sector also relies on pneumatic conveying to move bleaching earth during the production of edible oils and other products, where hygiene and contamination control are critical. Furthermore, in the chemical and pharmaceutical industries, the technology is employed to handle bleaching earth as a raw material for various manufacturing processes, ensuring consistent quality and safety.
The practical implementation of pneumatic conveying systems involves several components that work in concert to achieve efficient material transport. The system typically includes a hopper or storage silo to hold the bleaching earth, a rotary airlock valve to control the flow of material into the conveying line, and a positive displacement blower or fan to generate the necessary air pressure. The pipeline network, often constructed from stainless steel or other corrosion-resistant materials, is designed to withstand the abrasive nature of the fine powder. Additionally, a filter or cyclone separator is used at the receiving end to separate the air from the conveyed material, allowing the bleaching earth to be deposited in the target container or processing unit.
Over the years, the development of pneumatic conveying technology for bleaching earth has seen significant advancements aimed at improving efficiency, reducing energy consumption, and enhancing system reliability. One notable trend is the adoption of closed-loop systems, which recycle the air used in the conveying process, thereby minimizing energy waste and environmental impact. Another trend is the integration of automation and control systems, enabling real-time monitoring of system performance and allowing for adjustments to be made promptly based on operational conditions. These advancements not only improve the overall efficiency of the process but also contribute to cost savings and increased productivity for industrial clients.
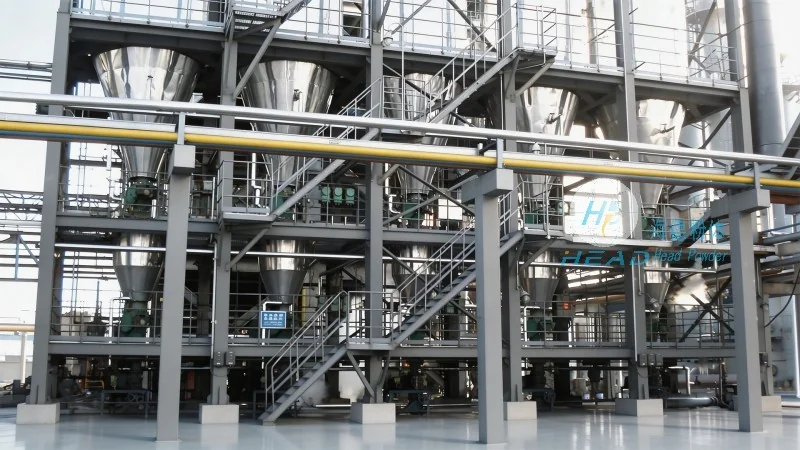
As the demand for high-quality bleaching earth continues to grow in various industries, the role of advanced pneumatic conveying technology becomes increasingly vital. Companies like Shandong HeadPowder Engineering Co., Ltd. are at the forefront of developing and implementing cutting-edge solutions that meet the evolving needs of their clients. By leveraging years of experience and expertise in material handling, HeadPowder ensures that its pneumatic conveying systems for bleaching earth are not only efficient and reliable but also adaptable to the specific requirements of each industrial application.
In conclusion, pneumatic conveying technology represents a sophisticated and effective method for transporting pulverized bleaching earth. From its fundamental principles to its diverse applications and ongoing technological advancements, this process plays a crucial role in supporting industrial operations across multiple sectors. With a commitment to innovation and quality, enterprises like Shandong HeadPowder Engineering Co., Ltd. continue to drive the development of pneumatic conveying solutions that enhance productivity and ensure the consistent quality of bleaching earth in various industrial processes.