

Principle and Working Scene Characteristics of Bentonite Powder Material Pneumatic Conveying System
Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced pneumatic conveying solutions tailored for the handling of bentonite powder. This article delves into the fundamental principles of such systems and highlights key working scene characteristics that make them ideal for industrial applications.
Core Principles of Bentonite Powder Pneumatic Conveying
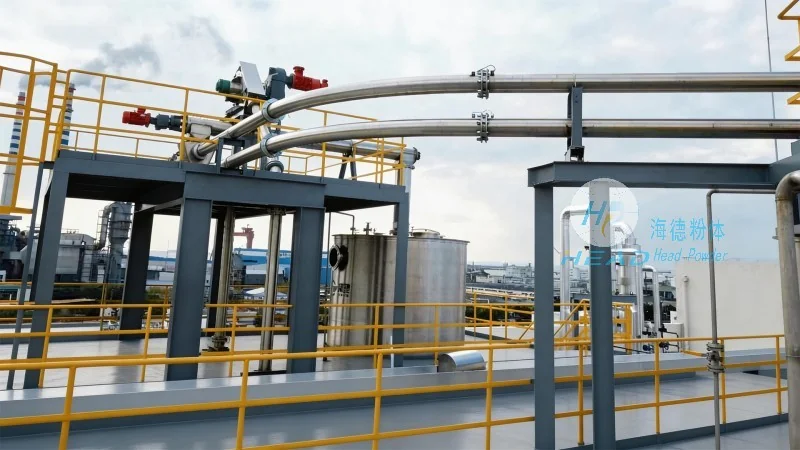
The pneumatic conveying system for bentonite powder operates on the principle of using compressed air to transport dry powder materials through a pipeline network. This method eliminates the need for mechanical components like conveyors or elevators, offering a more hygienic and efficient approach to material transport. The system typically consists of a blower, a hopper for material storage, a pipeline system, and a discharge point. Compressed air is introduced into the hopper, creating a pressure differential that lifts the bentonite powder and propels it through the pipeline to the desired destination. The design ensures minimal product degradation and contamination, which is crucial for applications where product quality and purity are paramount. The air velocity and pressure within the system are carefully controlled to maintain optimal flow rates, preventing blockages and ensuring consistent material delivery. The use of specialized nozzles and valves further optimizes the transport process, allowing for precise control over the flow of bentonite powder. This control is essential for applications that require accurate dosing or uniform distribution of the material.
Key Working Scene Characteristics
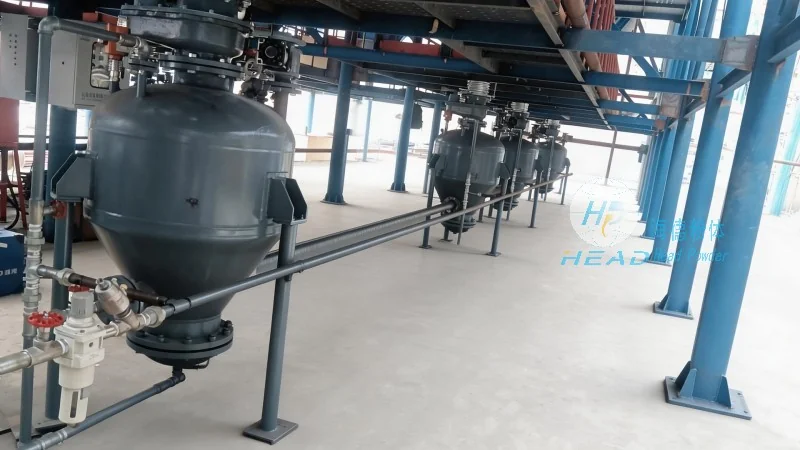
The working scene characteristics of bentonite powder pneumatic conveying systems are tailored to meet the specific demands of industrial environments. These systems are commonly employed in scenarios where bulk handling of fine powders is required, such as in chemical processing, pharmaceutical manufacturing, and food processing industries. For instance, in chemical plants, bentonite powder is used as a filter aid or adsorbent, and the pneumatic conveying system ensures efficient transport from storage silos to processing units. In pharmaceutical manufacturing, the hygienic design of the system is critical to prevent cross-contamination, making it suitable for handling active pharmaceutical ingredients (APIs) or excipients. Similarly, in food processing, the system is used to transport bentonite as a clarifying agent in beverage production, maintaining product quality and safety. The adaptability of the system to different plant layouts, including multi-level facilities or remote storage areas, further enhances its utility in diverse industrial settings. The system's ability to handle high volumes of material with minimal downtime makes it ideal for continuous production lines, where operational efficiency is a top priority.
Advantages in Industrial Applications
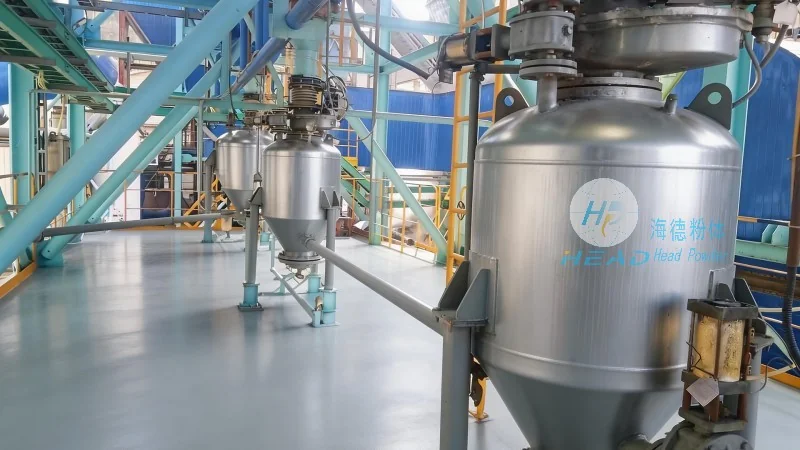
Implementing a pneumatic conveying system for bentonite powder offers several advantages over traditional material handling methods. The primary benefit is the reduction in labor costs and operational complexity, as the system automates the entire transport process. Furthermore, the absence of moving parts minimizes maintenance requirements, leading to lower long-term operational expenses. The system also enhances safety by eliminating the need for manual handling of heavy or dusty materials, reducing the risk of workplace accidents. In terms of product quality, the enclosed pipeline system prevents contamination from external sources and minimizes dust emissions, contributing to a cleaner working environment. These advantages make the system a preferred choice for industries seeking efficient, reliable, and cost-effective material handling solutions. Additionally, the system's ability to handle high volumes of material with minimal downtime makes it suitable for continuous production lines, where uninterrupted operation is essential for meeting production targets. The flexibility in system configuration, such as the option to integrate with existing infrastructure or expand capacity, provides long-term scalability for growing businesses. The hygienic and dust-free operation of the system aligns with stringent industry standards, ensuring compliance in sectors like food and pharmaceuticals where product integrity is non-negotiable.
Conclusion and Company Overview
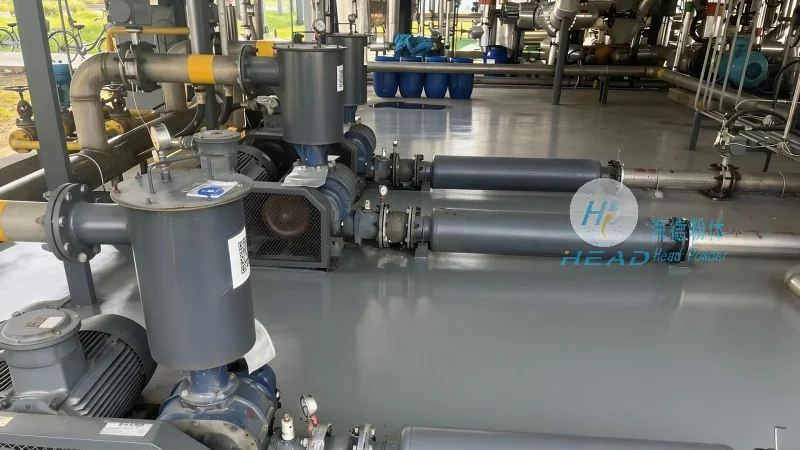
Shandong HeadPowder Engineering Co., Ltd. leverages its expertise in pneumatic conveying technology to deliver customized solutions for bentonite powder handling. With a focus on innovation and quality, the company ensures that its systems meet the unique requirements of each industrial application. The combination of advanced engineering, robust design, and adherence to industry standards positions HeadPowder as a trusted partner for businesses seeking reliable material transport solutions. Based in China, the company's facilities are equipped to handle large-scale projects and provide comprehensive support throughout the lifecycle of the system, from installation to maintenance. By prioritizing efficiency, safety, and product quality, HeadPowder continues to set the benchmark for pneumatic conveying systems in the bentonite powder industry.