

Principle and Working Scene Characteristics of Corn Granular Material Pneumatic Conveying Systems
HeadPowder, a leading provider of industrial material handling solutions, specializes in the design and implementation of advanced pneumatic conveying systems for corn granular materials. This article explores the fundamental principles behind these systems and highlights the key working scene characteristics that make them indispensable in modern agricultural and processing industries.
Understanding the Core Principle of Pneumatic Conveying Systems
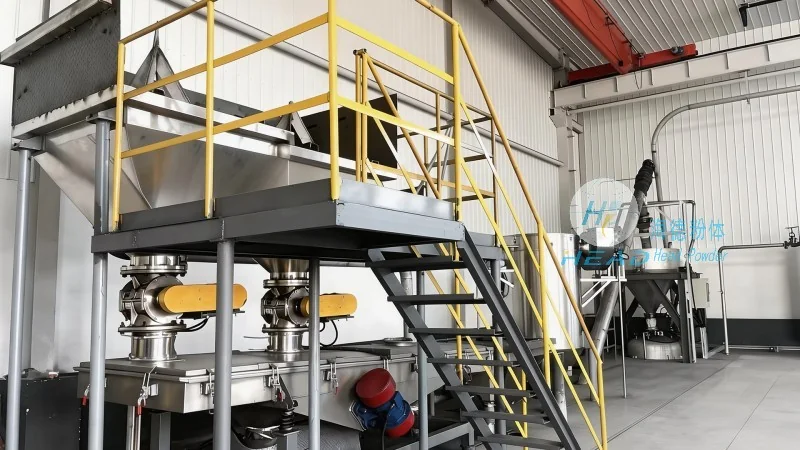
The core principle of a corn granular material pneumatic conveying system is the use of air or gas to transport solid particles through a pipeline. Unlike traditional mechanical conveyors, which rely on belts, chains, or screws, pneumatic systems utilize differential pressure to move materials. In this process, a fan or blower generates a flow of air within the pipeline, creating a pressure differential that propels the corn granules forward. The system typically consists of a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the discharged material. The selection of the appropriate air velocity and pressure is critical to ensure efficient and reliable transport, as it directly impacts the system's capacity and the integrity of the corn particles.
Key Working Scene Characteristics of Pneumatic Conveying Systems
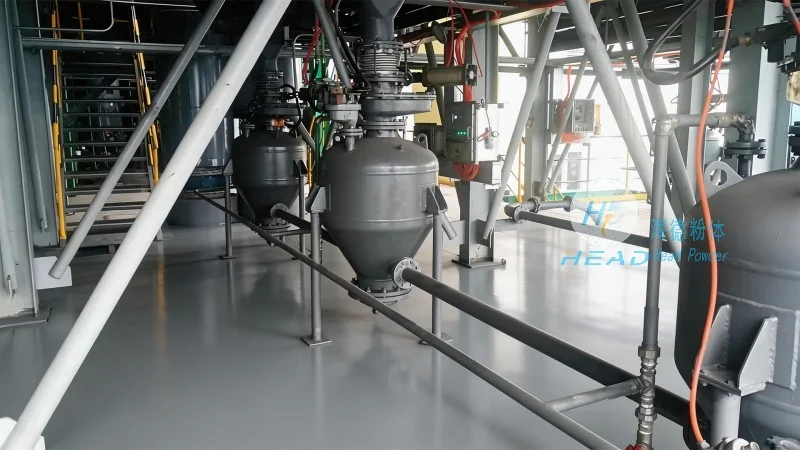
The working scene characteristics of corn granular material pneumatic conveying systems are tailored to meet the specific demands of various industrial applications. These systems are commonly employed in scenarios where the transport of bulk materials over long distances or through complex layouts is required. For instance, in corn processing facilities, these systems are used to move raw corn from storage silos to grinding or milling equipment. The flexibility of pneumatic conveyors allows them to navigate through multiple processing stages without the need for extensive reconfiguration. Additionally, the systems are designed to handle varying particle sizes and moisture content, ensuring consistent performance even with different batches of corn. The ability to operate in a closed system also minimizes dust emissions and maintains hygiene standards, which is crucial in food processing environments.
Advantages and Practical Applications in Industrial Settings
HeadPowder's pneumatic conveying systems for corn granular materials offer several advantages that make them a preferred choice in industrial settings. One of the primary benefits is the high efficiency in material transport, as the systems can handle large volumes of corn with minimal energy consumption compared to traditional methods. The compact design of these systems allows for installation in spaces with limited room, making them suitable for both new and retrofit applications. Furthermore, the systems are equipped with advanced control technologies that enable real-time monitoring and adjustment of the conveying parameters, ensuring optimal performance and reducing downtime. In agricultural processing plants, these systems are widely used for the seamless transfer of corn from storage to processing units, contributing to streamlined production workflows. The reliability and durability of HeadPowder's systems are further enhanced by the use of high-quality materials and robust construction, ensuring long-term operation with minimal maintenance requirements.
About HeadPowder Engineering Co., Ltd.
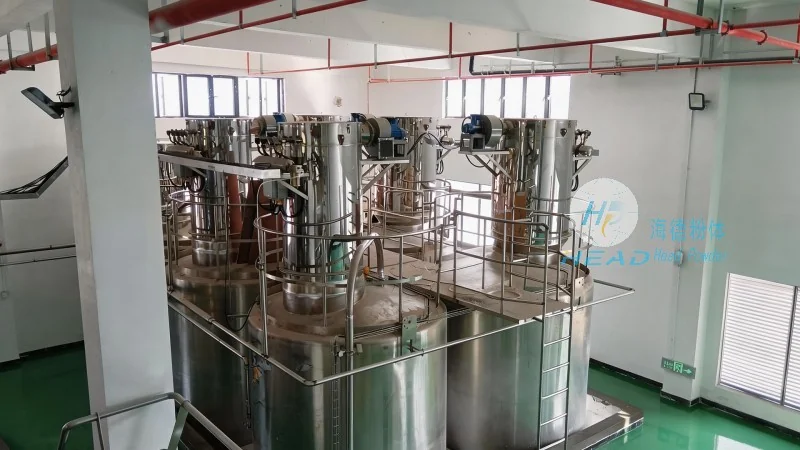
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a renowned manufacturer specializing in the development and production of industrial material handling equipment. With years of experience in the field, the company has established itself as a trusted partner for businesses seeking efficient and reliable solutions for bulk material transport. HeadPowder's commitment to innovation and quality has enabled them to deliver customized pneumatic conveying systems that meet the unique requirements of various industries, including agriculture, food processing, and chemical manufacturing. The company's team of experts provides comprehensive support, from system design and installation to maintenance and after-sales service, ensuring customer satisfaction and operational excellence.