

Principle and Working Scene Characteristics of Cereal Pulp Powder Pneumatic Conveying Equipment
Cereal pulp powder pneumatic conveying equipment is a specialized system engineered for the efficient and reliable transport of fine powders, such as those derived from cereal processing like malt or grain residues. This equipment is pivotal in industries where handling dry, particulate materials is essential, particularly in the food, feed, and agricultural sectors. The subsequent sections will delve into the fundamental principles behind these systems and the key characteristics of their operational environments.
The Core Principle of Pneumatic Conveying Systems
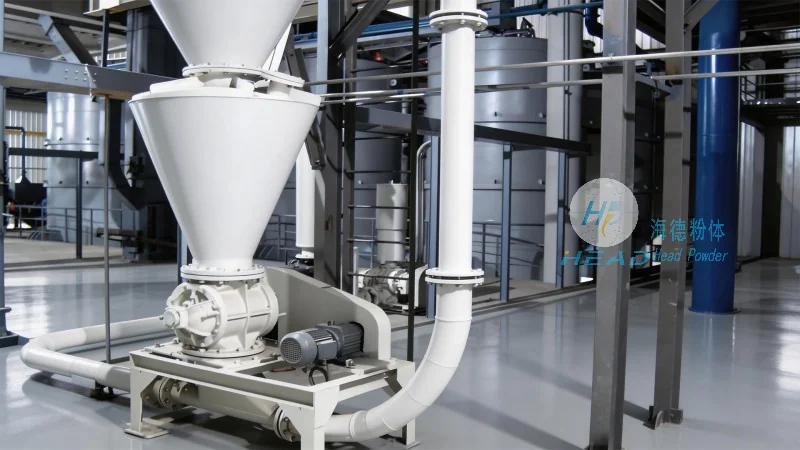
The operation of cereal pulp powder pneumatic conveying equipment is based on the fundamental principle of utilizing air flow to move solid particles. Unlike traditional mechanical conveyors, which rely on physical contact and friction, pneumatic systems employ compressed air or suction to create a flow that carries the powder through a pipeline. This method is particularly effective for materials that are light, dusty, or prone to caking, as it minimizes product degradation and reduces the risk of contamination. The system typically comprises a source of air (either a blower or a vacuum pump), a hopper or feeder to introduce the powder, and a pipeline network that transports the material to its destination. The air flow is controlled to maintain a consistent velocity, ensuring that the powder particles are suspended and moved smoothly without settling or blocking the line.
Working Scene Characteristics and Application Advantages
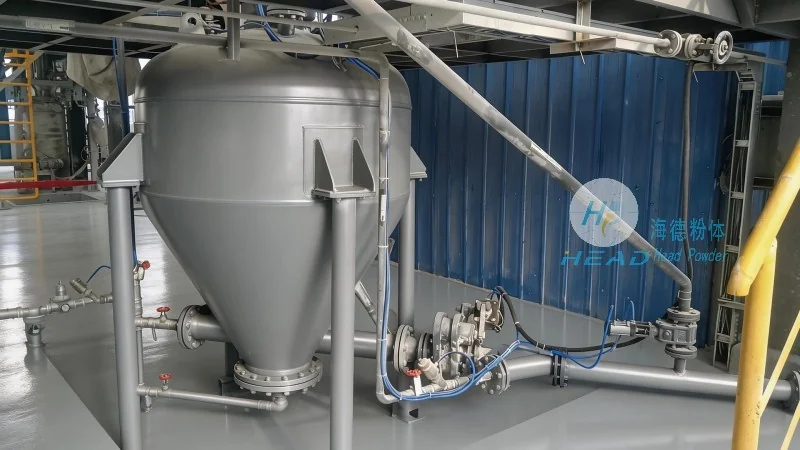
The working scene characteristics of cereal pulp powder pneumatic conveying equipment are tailored to the specific demands of industrial processes. These systems are commonly employed in environments where hygiene, cleanliness, and product integrity are paramount. For example, in the production of animal feed, the equipment ensures that the cereal pulp is transported without cross-contamination from other materials or equipment. Similarly, in the food processing industry, such as in breweries or distilleries, the system efficiently handles spent grains or malt residues, maintaining the quality of the final product. One of the key advantages is the ability to handle materials that are difficult to convey with traditional methods, such as fine powders that are prone to dusting or clogging. The pneumatic system also offers flexibility in terms of layout, as the pipeline can be configured to follow the existing plant layout, minimizing the need for additional space or structural modifications. Additionally, these systems are generally more compact and require less maintenance compared to bulk handling equipment, making them a cost-effective solution for many industrial applications.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
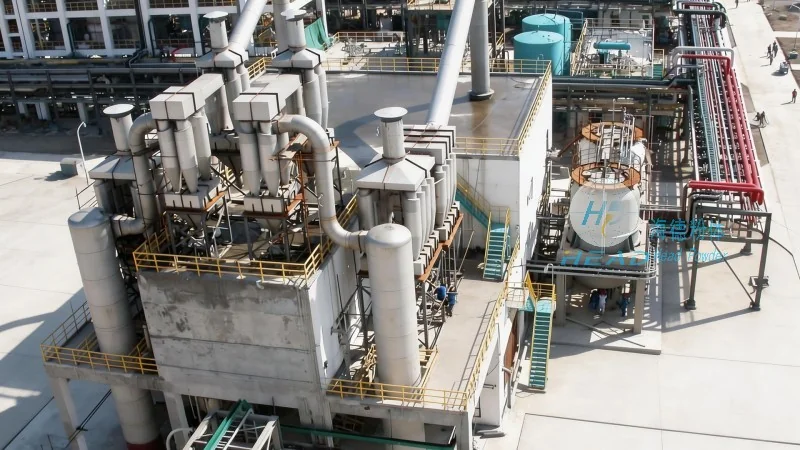
HeadPowder, a professional manufacturer of cereal pulp powder pneumatic conveying equipment, is a leading company based in Shandong, China. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted supplier in the field of powder handling technology. The company specializes in designing and manufacturing customized pneumatic conveying systems tailored to the unique requirements of its clients. HeadPowder's products are engineered to meet the highest standards of efficiency, reliability, and safety, ensuring optimal performance in various industrial settings. The company's headquarters and main operations are located in Shandong, providing a solid foundation for its global presence and customer support. By leveraging advanced engineering and manufacturing capabilities, HeadPowder continues to deliver cutting-edge solutions that enhance productivity and operational efficiency for its clients in the food, feed, and agricultural industries.